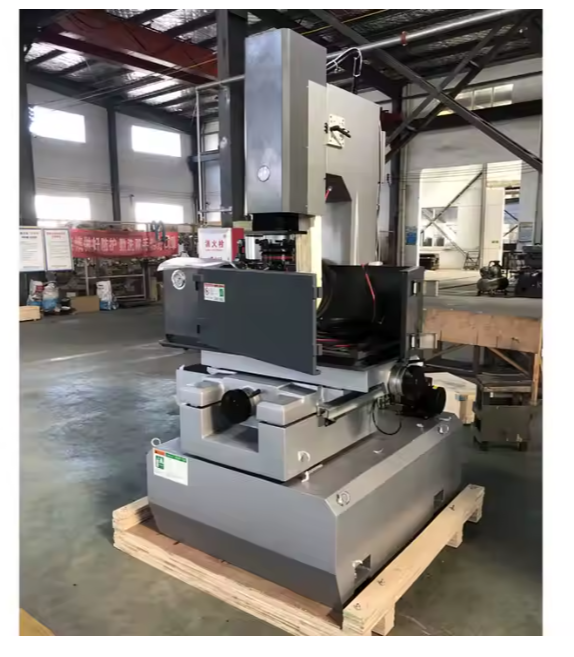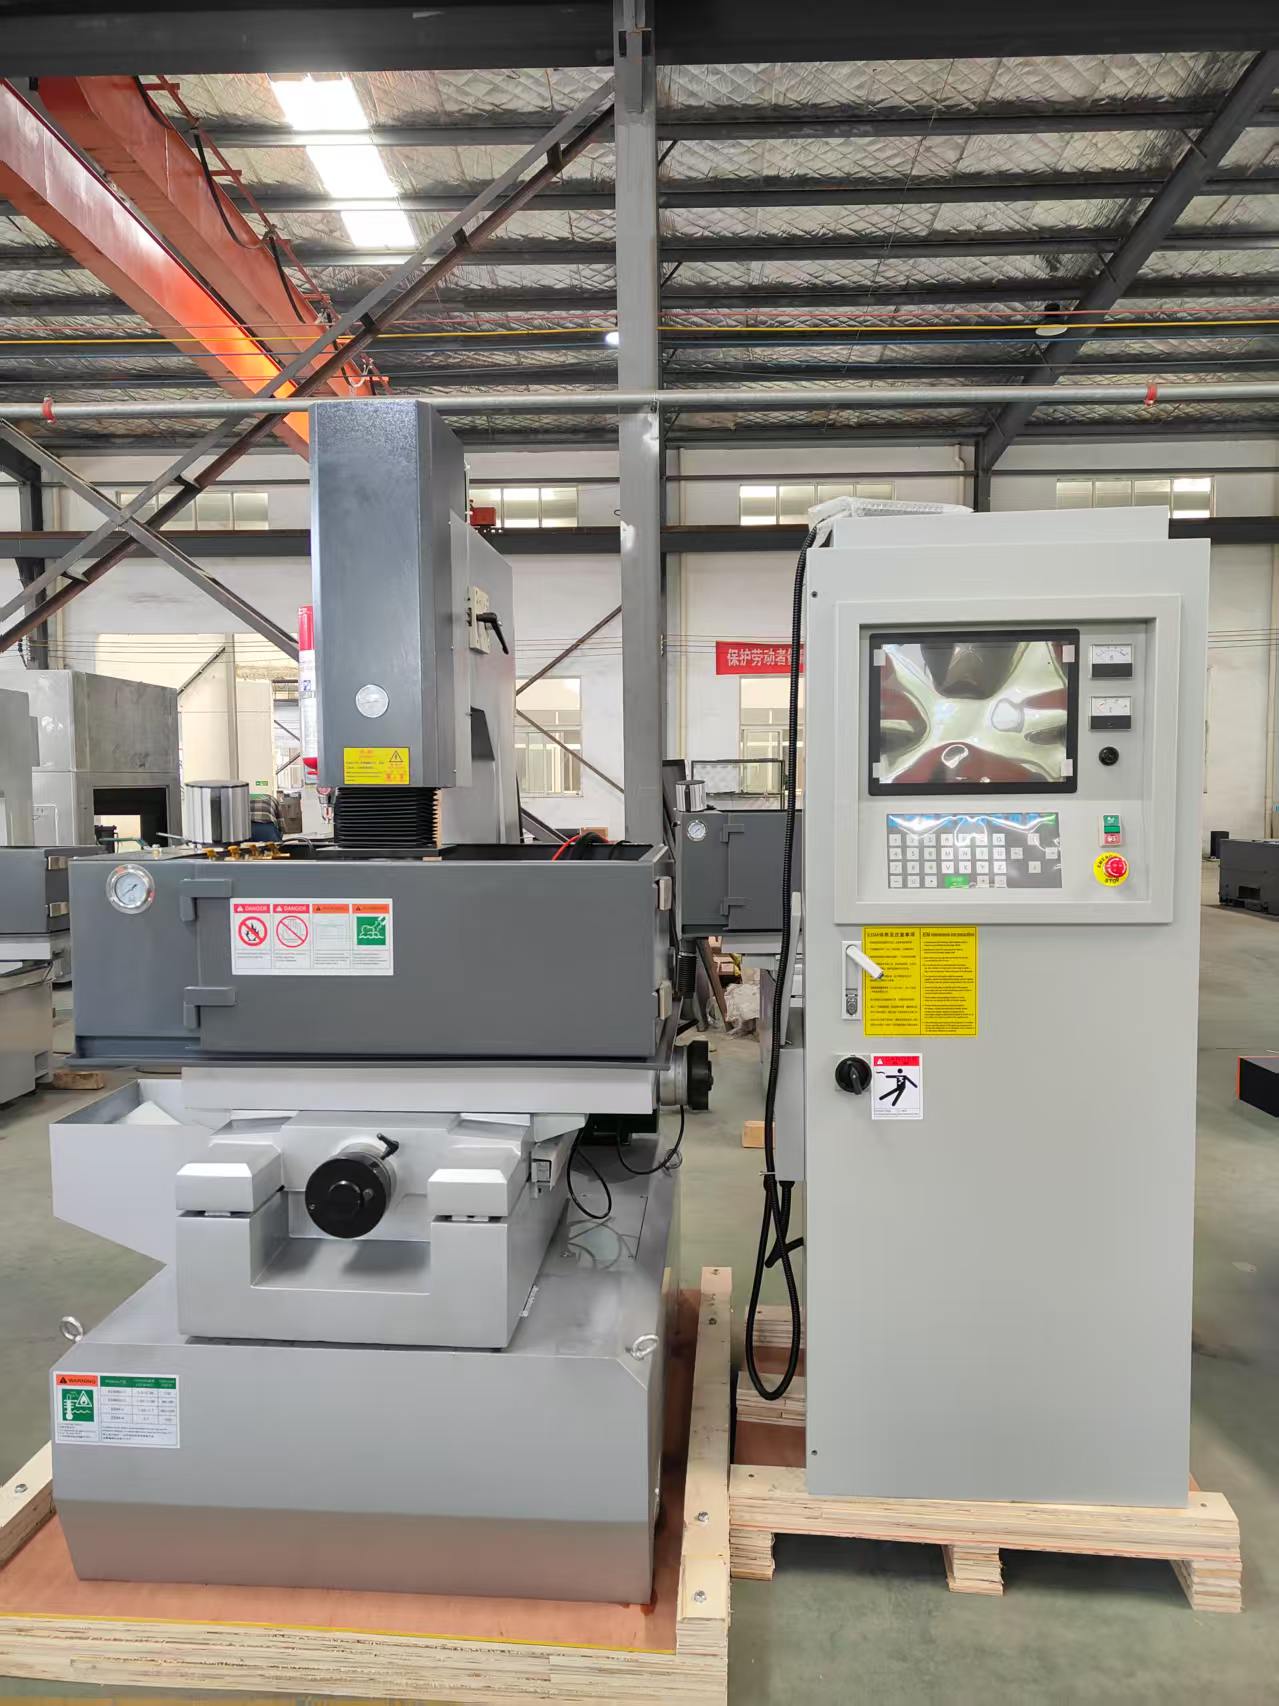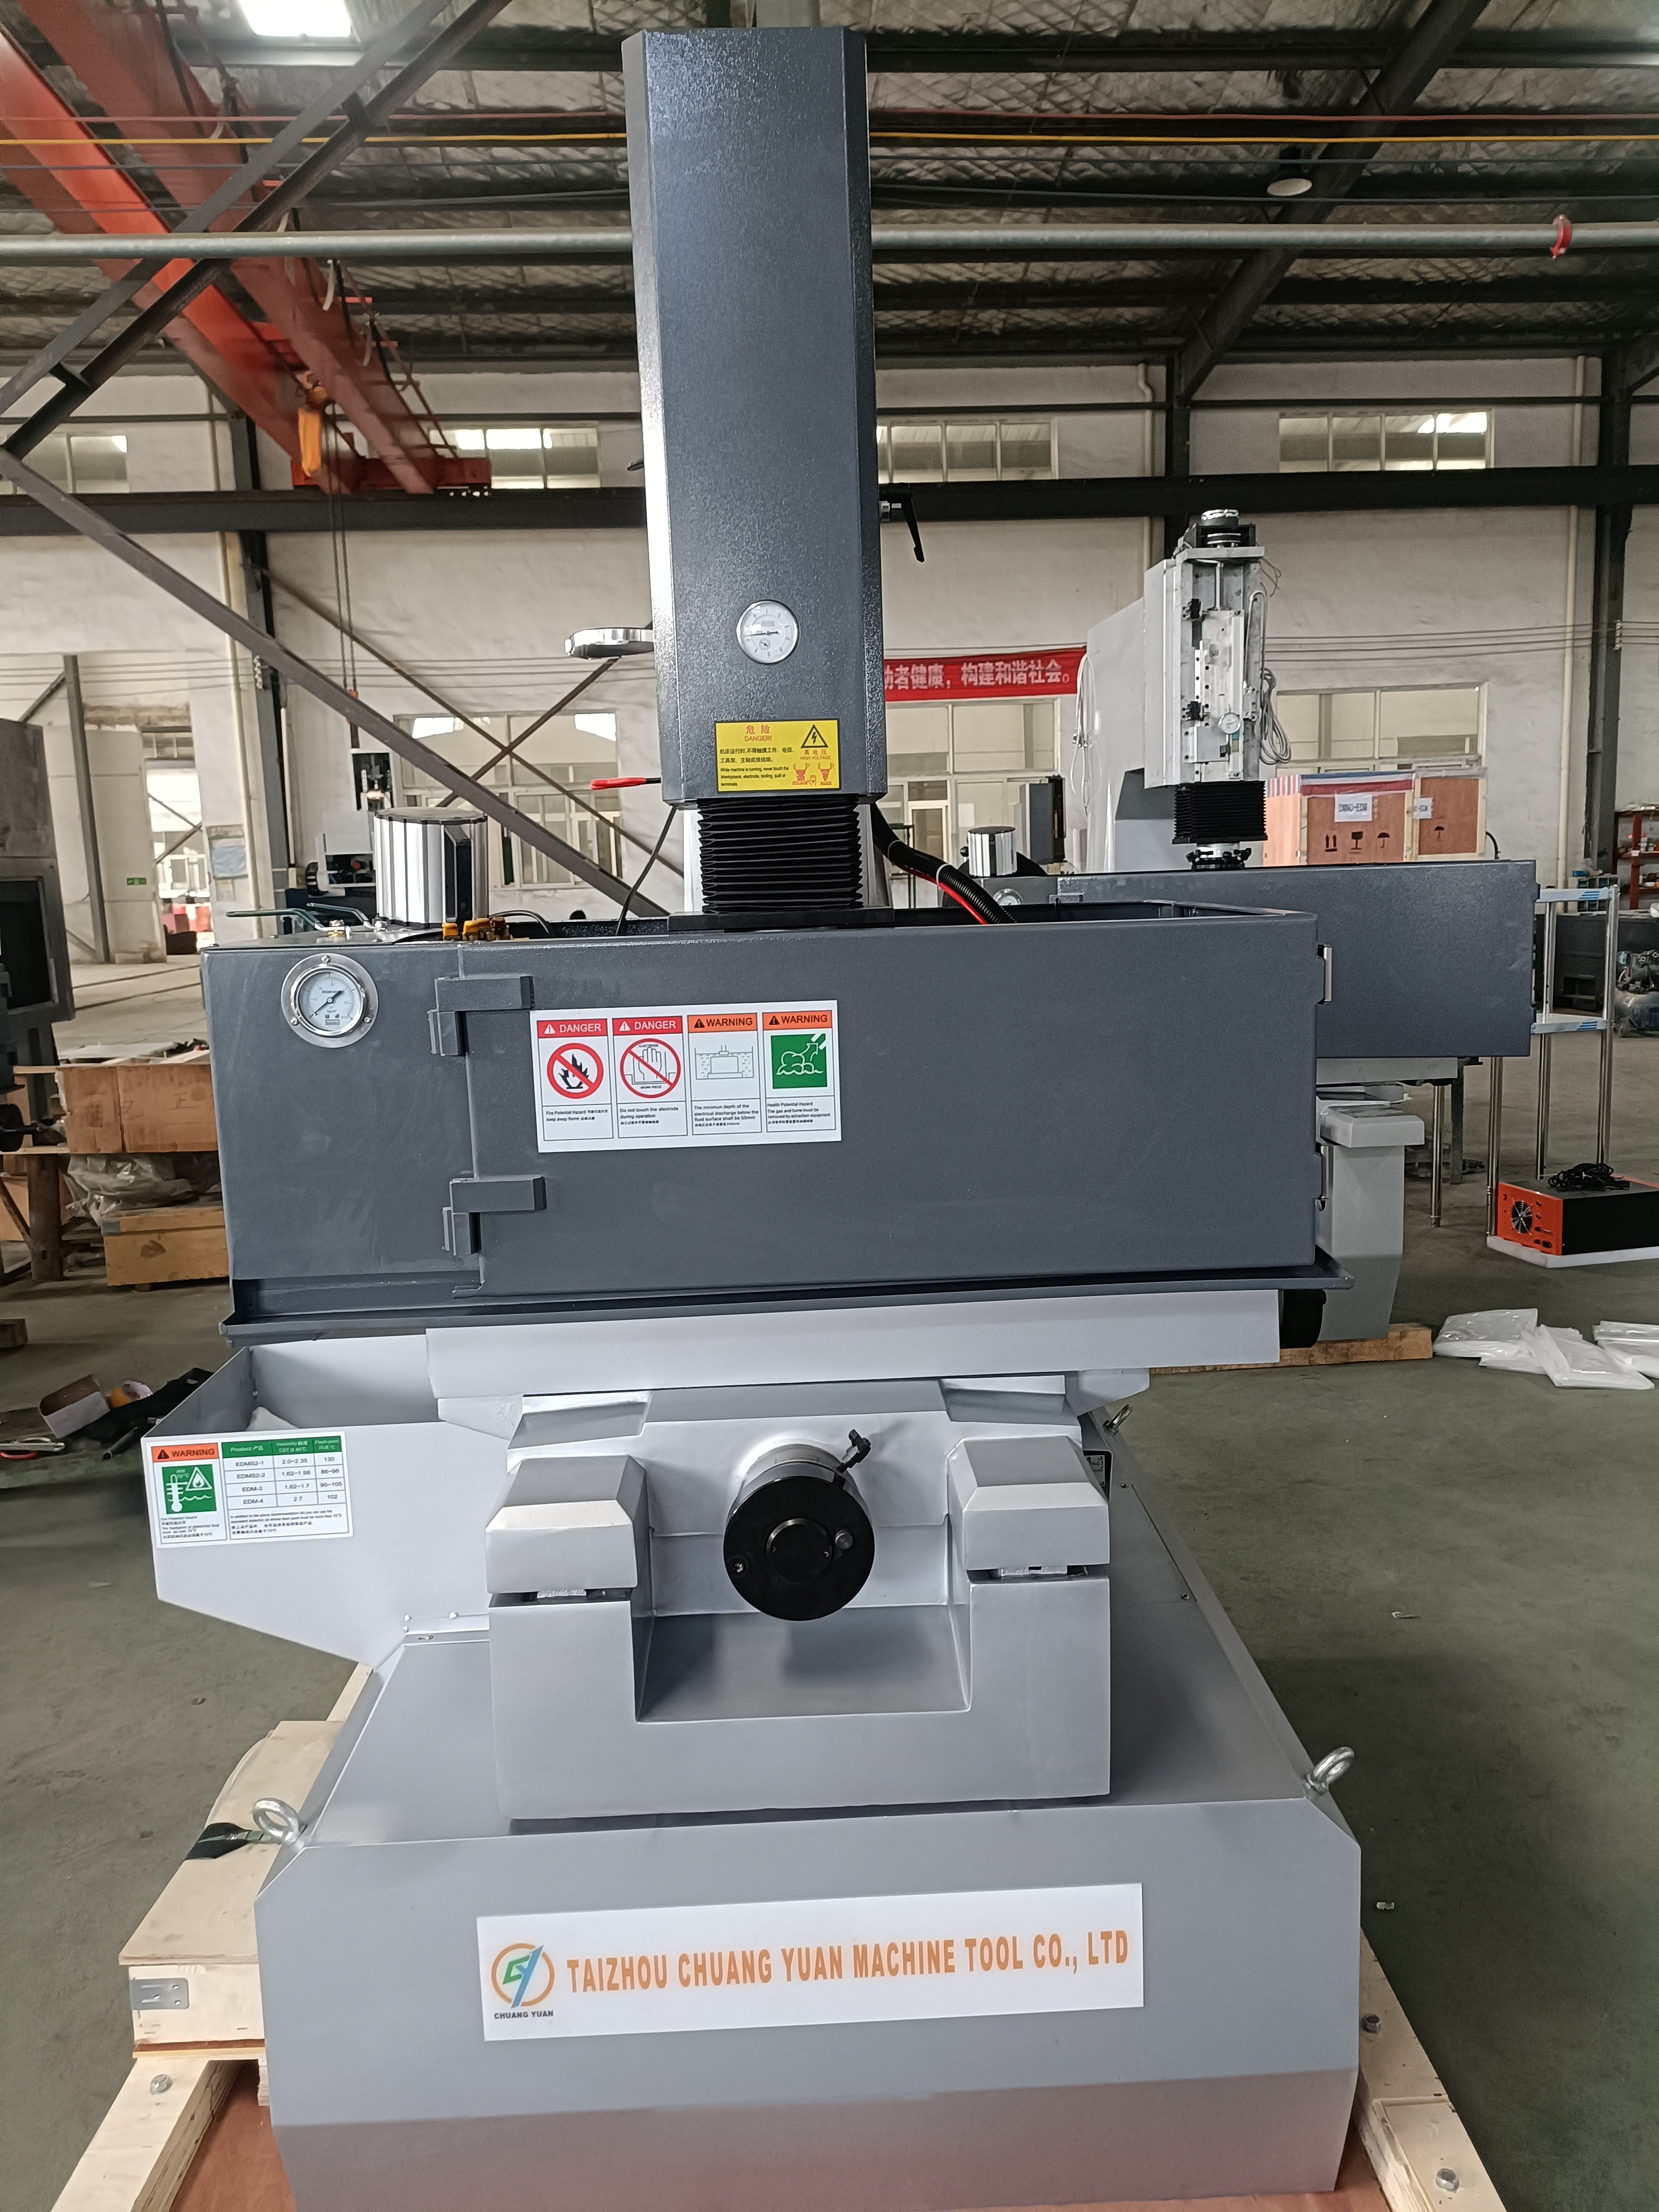
Die Sinking EDM Machine | ±0.005mm Accuracy, Ra 0.2µm Finish

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Die Sinking EDM Machine Advantages Built on Two Decades of Precision Manufacturing Excellence

Die Sinking EDM Machine Advantages Built on Two Decades of Precision Manufacturing Excellence

As a professional manufacturer established in 2003 in Taizhou City, Jiangsu Province, Taizhou Chuang Yuan Machine Tool Co., Ltd. integrates research and development, production, and sales of precision machine tools. Our Die Sinking EDM Machine delivers repeatable accuracy of ±0.005 mm and a best surface finish of Ra 0.2 µm, supported by rigid cast-iron structures, precision linear guides, and intelligent CNC pulse generators. In mold-making shops, tool rooms, and aerospace component plants, operators rely on our machines for deep-rib cavity work, sharp-corner inserts, and hardened steel dies above 60 HRC. A German mold maker reduced electrode wear by 28 percent and cut cavity finishing time from 14 hours to 9 hours after switching to our ZNC and CNC Die Sinking EDM Machine series. Power consumption is lowered by up to 22 percent through adaptive discharge control, while automatic tool changers and multi-cavity programming raise unattended runtime beyond 20 hours.
Get A Quote

Case Study

Automotive Die Maker Cuts Electrode Costs by 31 Percent

A tier-one automotive stamping supplier in Thailand produced complex door-panel dies with deep ribs and narrow slots. Their existing Die Sinking EDM Machine struggled with unstable arcs, causing electrode scrap and rework. We supplied a CNC model with adaptive discharge control and a 40-position electrode changer. Within three months, electrode consumption fell 31 percent, surface rework dropped from 12 percent to 3 percent, and die delivery lead time improved by 18 percent, supporting a monthly output of 45 die sets.

Medical Mold Manufacturer Raises Cavity Accuracy to ±0.003 mm

A medical device mold maker in Italy needed multi-cavity syringe molds with mirror-like finishes. Using our Die Sinking EDM Machine with fine-finish circuitry and temperature-stabilized dielectric handling, they achieved ±0.003 mm dimensional consistency and Ra 0.15 µm on hardened stainless inserts. Scrap rate decreased from 8 percent to under 2 percent, and the company now runs three of our machines across two shifts, exporting molded parts to 14 countries.

Aerospace Tool Room Reduces Setup Time by 40 Percent

A European aerospace tool room machined nickel-based alloy fixtures with frequent small-batch changeovers. Our Die Sinking EDM Machine, equipped with a rotary C-axis and quick-change chuck system, cut setup time by 40 percent and eliminated manual re-alignment errors. Orbit control held corner accuracy within 0.01 mm on 250 mm deep features, and machine availability reached 94 percent over 12 months, helping the shop win two long-term defense contracts.

Related products

The Die Sinking EDM Machine remains an indispensable asset in modern mold and tool manufacturing because it machines hardened conductive materials with accuracy that milling cannot match. At Taizhou Chuang Yuan Machine Tool Co., Ltd., established in 2003, we build these machines through a disciplined production flow that begins with finite-element analysis of the cast-iron base. Each base is seasoned, stress-relieved, and precision-ground before assembly, ensuring long-term geometric stability. The spindle head, linear guideways, and dielectric tank are produced on our own machining centers, which keeps critical tolerances within ±0.005 mm. During assembly, technicians scrape and align the X, Y, and Z axes, then calibrate the pulse generator to deliver stable discharges from roughing at 400 A to fine finishing at 1 A. Every Die Sinking EDM Machine undergoes a 72-hour load test that simulates real cavity work, checking depth accuracy, electrode wear ratio, and thermal drift. Our research team continuously refines adaptive control algorithms that reduce arcing, lower electrode wear by up to 30 percent, and shorten finishing cycles by roughly 20 percent. Global application data supports these figures: mold shops in Germany use our machines for multi-cavity packaging molds, automotive suppliers in Thailand rely on them for stamping dies, and medical manufacturers in Italy depend on them for syringe and implant molds. In each region, local voltage conditions, operator habits, and production rhythms are considered, so we configure dielectric cooling, handwheel jogging, and parameter libraries to match site realities. Service extends beyond delivery, with remote diagnostics, spare-part kits, and on-site training that help customers reach stable production within days. Because we export to more than 20 countries, our engineers understand diverse standards, including CE and ISO expectations, and can prepare documentation accordingly. For buyers evaluating a Die Sinking EDM Machine, the decisive factors are accuracy retention, electrode economy, and uptime, and our integrated manufacturing model addresses all three. We invite distributors and end users to visit our facility in Jiangsu Province, inspect machines under power, and discuss customized solutions for their local markets.

Frequently Asked Questions

What materials can a Die Sinking EDM Machine process effectively?

It machines any conductive material, including hardened tool steel above 60 HRC, carbide, copper alloys, titanium, and nickel-based superalloys. This makes it suitable for molds, dies, and aerospace fixtures where traditional cutting tools wear quickly or cannot reach deep ribs.
We provide on-site installation, commissioning, and training, plus remote diagnostics and video guidance. Parameter libraries are preloaded for common materials, and our engineers can adjust settings to local power conditions and production habits.
Standard models achieve ±0.005 mm positioning accuracy and surface finishes to Ra 0.2 µm; fine-finish configurations reach Ra 0.15 µm on mirror-cavity work. Results depend on electrode quality and process parameters, which we help optimize.
Standard Die Sinking EDM Machine models ship in 30 to 45 days after deposit, with a 12-month warranty covering core components. Spare parts are stocked for fast dispatch to more than 20 export markets.
Yes. With quick-change chucks, automatic tool changers, and multi-cavity programming, changeover time drops significantly, and unattended runtime can exceed 20 hours, which suits high-mix mold and tool rooms.

Related Articles

How to choose a machining center?

12

Dec

How to choose a machining center?

View More
What after sales service should reliable edm drilling machine suppliers provide

14

Jul

What after sales service should reliable edm drilling machine suppliers provide

The Evolution of Flexible Manufacturing Through Modular Architecture Modern industrial landscapes demand a high degree of adaptability, where the ability to transition production configurations quickly defines a facility’s operational rhythm....
View More
How to customize spring machine mold fixtures for special shaped spring production

03

Aug

How to customize spring machine mold fixtures for special shaped spring production

Mastering Complex Spring Production Challenges Navigating the intricacies of high-speed industrial manufacturing demands a profound understanding of wire feed dynamics, mechanical tolerances, and multi-axis bending mechanics across modern automated...
View More
What output benefits enterprises gain by updating old edm spark erosion machine equipment

03

Aug

What output benefits enterprises gain by updating old edm spark erosion machine equipment

Identifying Legacy Constraints in Spark Erosion Production Operating mature, decades-old equipment on high-precision manufacturing shop floors often creates hidden operational penalties that quietly erode profit margins over time. When production f...
View More

Customer Testimonials

Michael Berger, Tooling Manager, Germany
Reliable Accuracy in Daily Mold Production

We run two of their Die Sinking EDM Machine units for packaging molds. Depth repeatability stays within 0.005 mm after a year of two-shift operation, and electrode wear dropped about 25 percent compared with our previous machines. Their engineers trained our operators in two days.

Daniel Whitfield, Production Director, United Kingdom
Fast Support and Strong Uptime

Our aerospace fixture work needs tight corners and stable arcs. Their machine held 0.01 mm on deep features and ran at 94 percent availability. Spare parts arrived in four days, which kept our delivery schedule intact.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Integrated Research, Production, and Sales Since 2003

Integrated Research, Production, and Sales Since 2003

Taizhou Chuang Yuan Machine Tool Co., Ltd. was established in 2003 and operates as a professional manufacturer integrating research and development, production, and sales. This integrated model means the Die Sinking EDM Machine is not assembled from loosely sourced parts but engineered around our own castings, machined components, and control software. Our engineers design the pulse generator, spindle, and dielectric system as one coordinated platform, which improves discharge stability and accuracy retention. Because design, machining, and final testing happen under one roof, we respond quickly to customer requests, whether that means a custom Z-axis travel or a modified work tank. For buyers, the benefit is traceable quality: every critical component carries inspection records, and each Die Sinking EDM Machine completes a 72-hour load test before shipment.
Verified Performance Metrics That Lower Cost Per Part

Verified Performance Metrics That Lower Cost Per Part

Our Die Sinking EDM Machine is engineered around measurable outcomes: ±0.005 mm positioning accuracy, surface finish to Ra 0.2 µm, electrode wear reduction up to 30 percent, and power savings up to 22 percent. These figures come from controlled tests and field data across more than 20 export markets, not marketing estimates. In a German mold shop, finishing time for a hardened cavity fell from 14 hours to 9 hours; in Thailand, an automotive die maker cut electrode consumption by 31 percent and rework from 12 percent to 3 percent. Such gains directly lower cost per part, which matters in industries where mold lead time and electrode expense dominate budgets. Adaptive discharge control prevents harmful arcs, extends electrode life, and protects the workpiece, while multi-cavity programming and automatic tool changers raise unattended runtime beyond 20 hours. We also monitor thermal drift and dielectric condition to keep results repeatable across shifts.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop