Mesin CNC EDM Die Sinker | ±0.005mm Accuracy & Ra 0.2µm Finish

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Mesin CNC EDM Die Sinker Built for Precision Mold and Die Manufacturing

Mesin CNC EDM Die Sinker Built for Precision Mold and Die Manufacturing

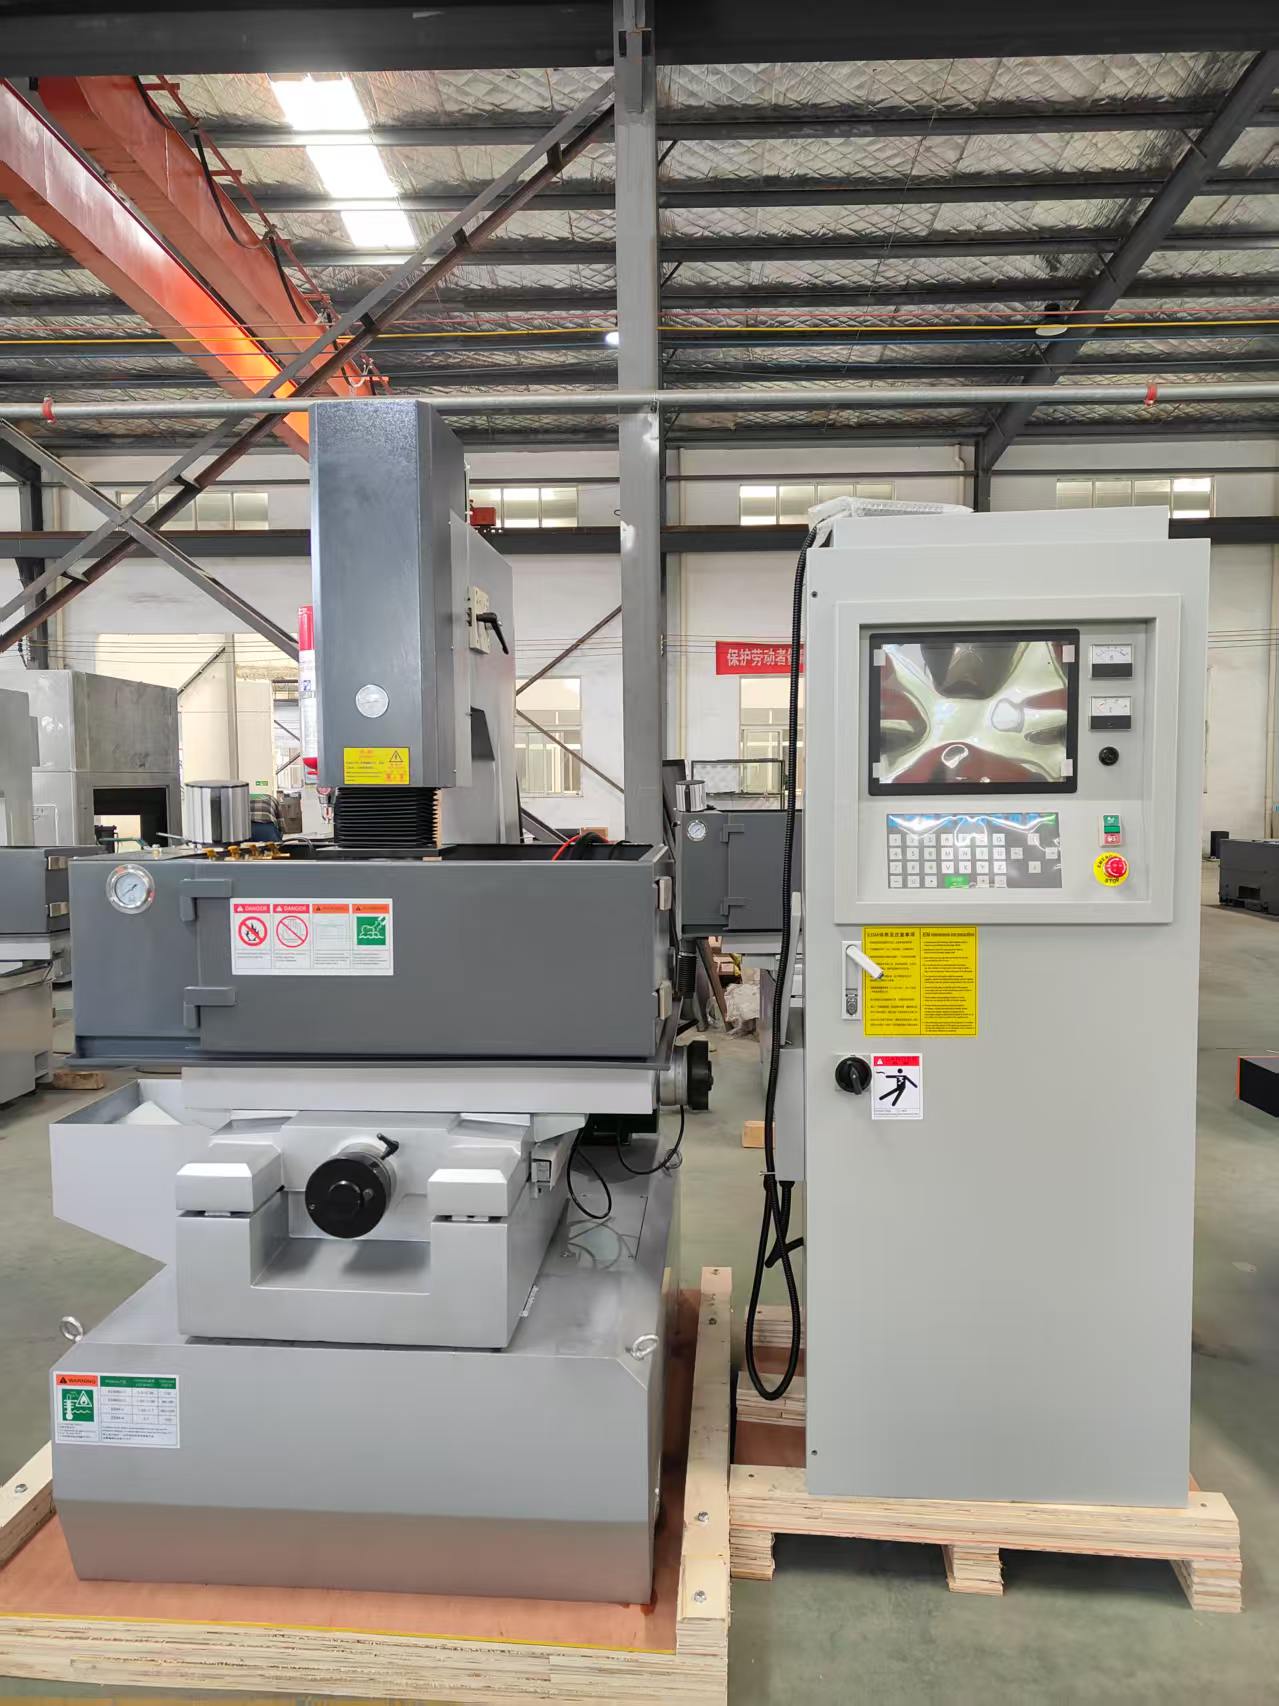
Taizhou Chuang Yuan Machine Tool Co., Ltd. has manufactured Mesin CNC EDM Die Sinker solutions since 2003 from Taizhou City, Jiangsu Province, China, integrating research, production, and sales into one professional operation. Our Mesin CNC EDM Die Sinker platforms serve mold shops, die makers, aerospace tooling suppliers, and automotive stamping plants that machine hardened tool steel, carbide inserts, and complex cavities where conventional cutting fails. In daily use, operators rely on the CNC-controlled Z-axis servo, multi-axis interpolation, and automatic electrode wear compensation to burn deep ribs, sharp corners, and fine surface finishes in a single setup. Quantified results from our installations show positioning accuracy of +/-0.005 mm, best surface roughness of Ra 0.2 um, electrode wear reduced by up to 30 percent, and 20 to 40 percent shorter machining cycles compared with manual ram EDM.
Get A Quote

Case Study

Automotive Stamping Die Producer Cuts Electrode Cost by 28 Percent

A Thai automotive stamping die manufacturer faced frequent electrode replacement on deep door-panel cavities, driving up consumable cost and downtime. Our Mesin CNC EDM Die Sinker with adaptive discharge control and programmable multi-cavity orbits stabilized the burn, reduced electrode wear by 28 percent, and shortened each cavity cycle from 9.5 hours to 6.8 hours. The customer now runs three shifts with one operator supervising two machines, and scrap from over-burn was cut to below 1 percent. The project paid back the equipment investment within 14 months.

Medical Mold Maker Achieves Ra 0.2 um Finish on Hardened Steel

A German medical mold maker needed mirror-like cavities in 1.2344 hardened steel at 52 HRC. Using our Mesin CNC EDM Die Sinker with fine-finish power packs and graphite electrode optimization, the shop reached Ra 0.2 um directly after EDM, eliminating a separate polishing operation. Dimensional consistency held within +/-0.005 mm across 120 cavities, and lead time for new insulin pen molds dropped from 25 days to 17 days. The client reported a 22 percent increase in accepted mold orders in the following year.

Aerospace Tooling Supplier Reduces Setup Time by 35 Percent

A Brazilian aerospace tooling supplier machined nickel-based alloy fixtures with frequent manual re-alignment. Our Mesin CNC EDM Die Sinker with automatic tool changers, on-machine touch probing, and stored process libraries reduced setup time by 35 percent and held true position within 0.01 mm. After 18 months of two-shift operation, unplanned downtime stayed under 1.5 percent, helping the supplier win a long-term contract for turbine blade fixture production.

Related products

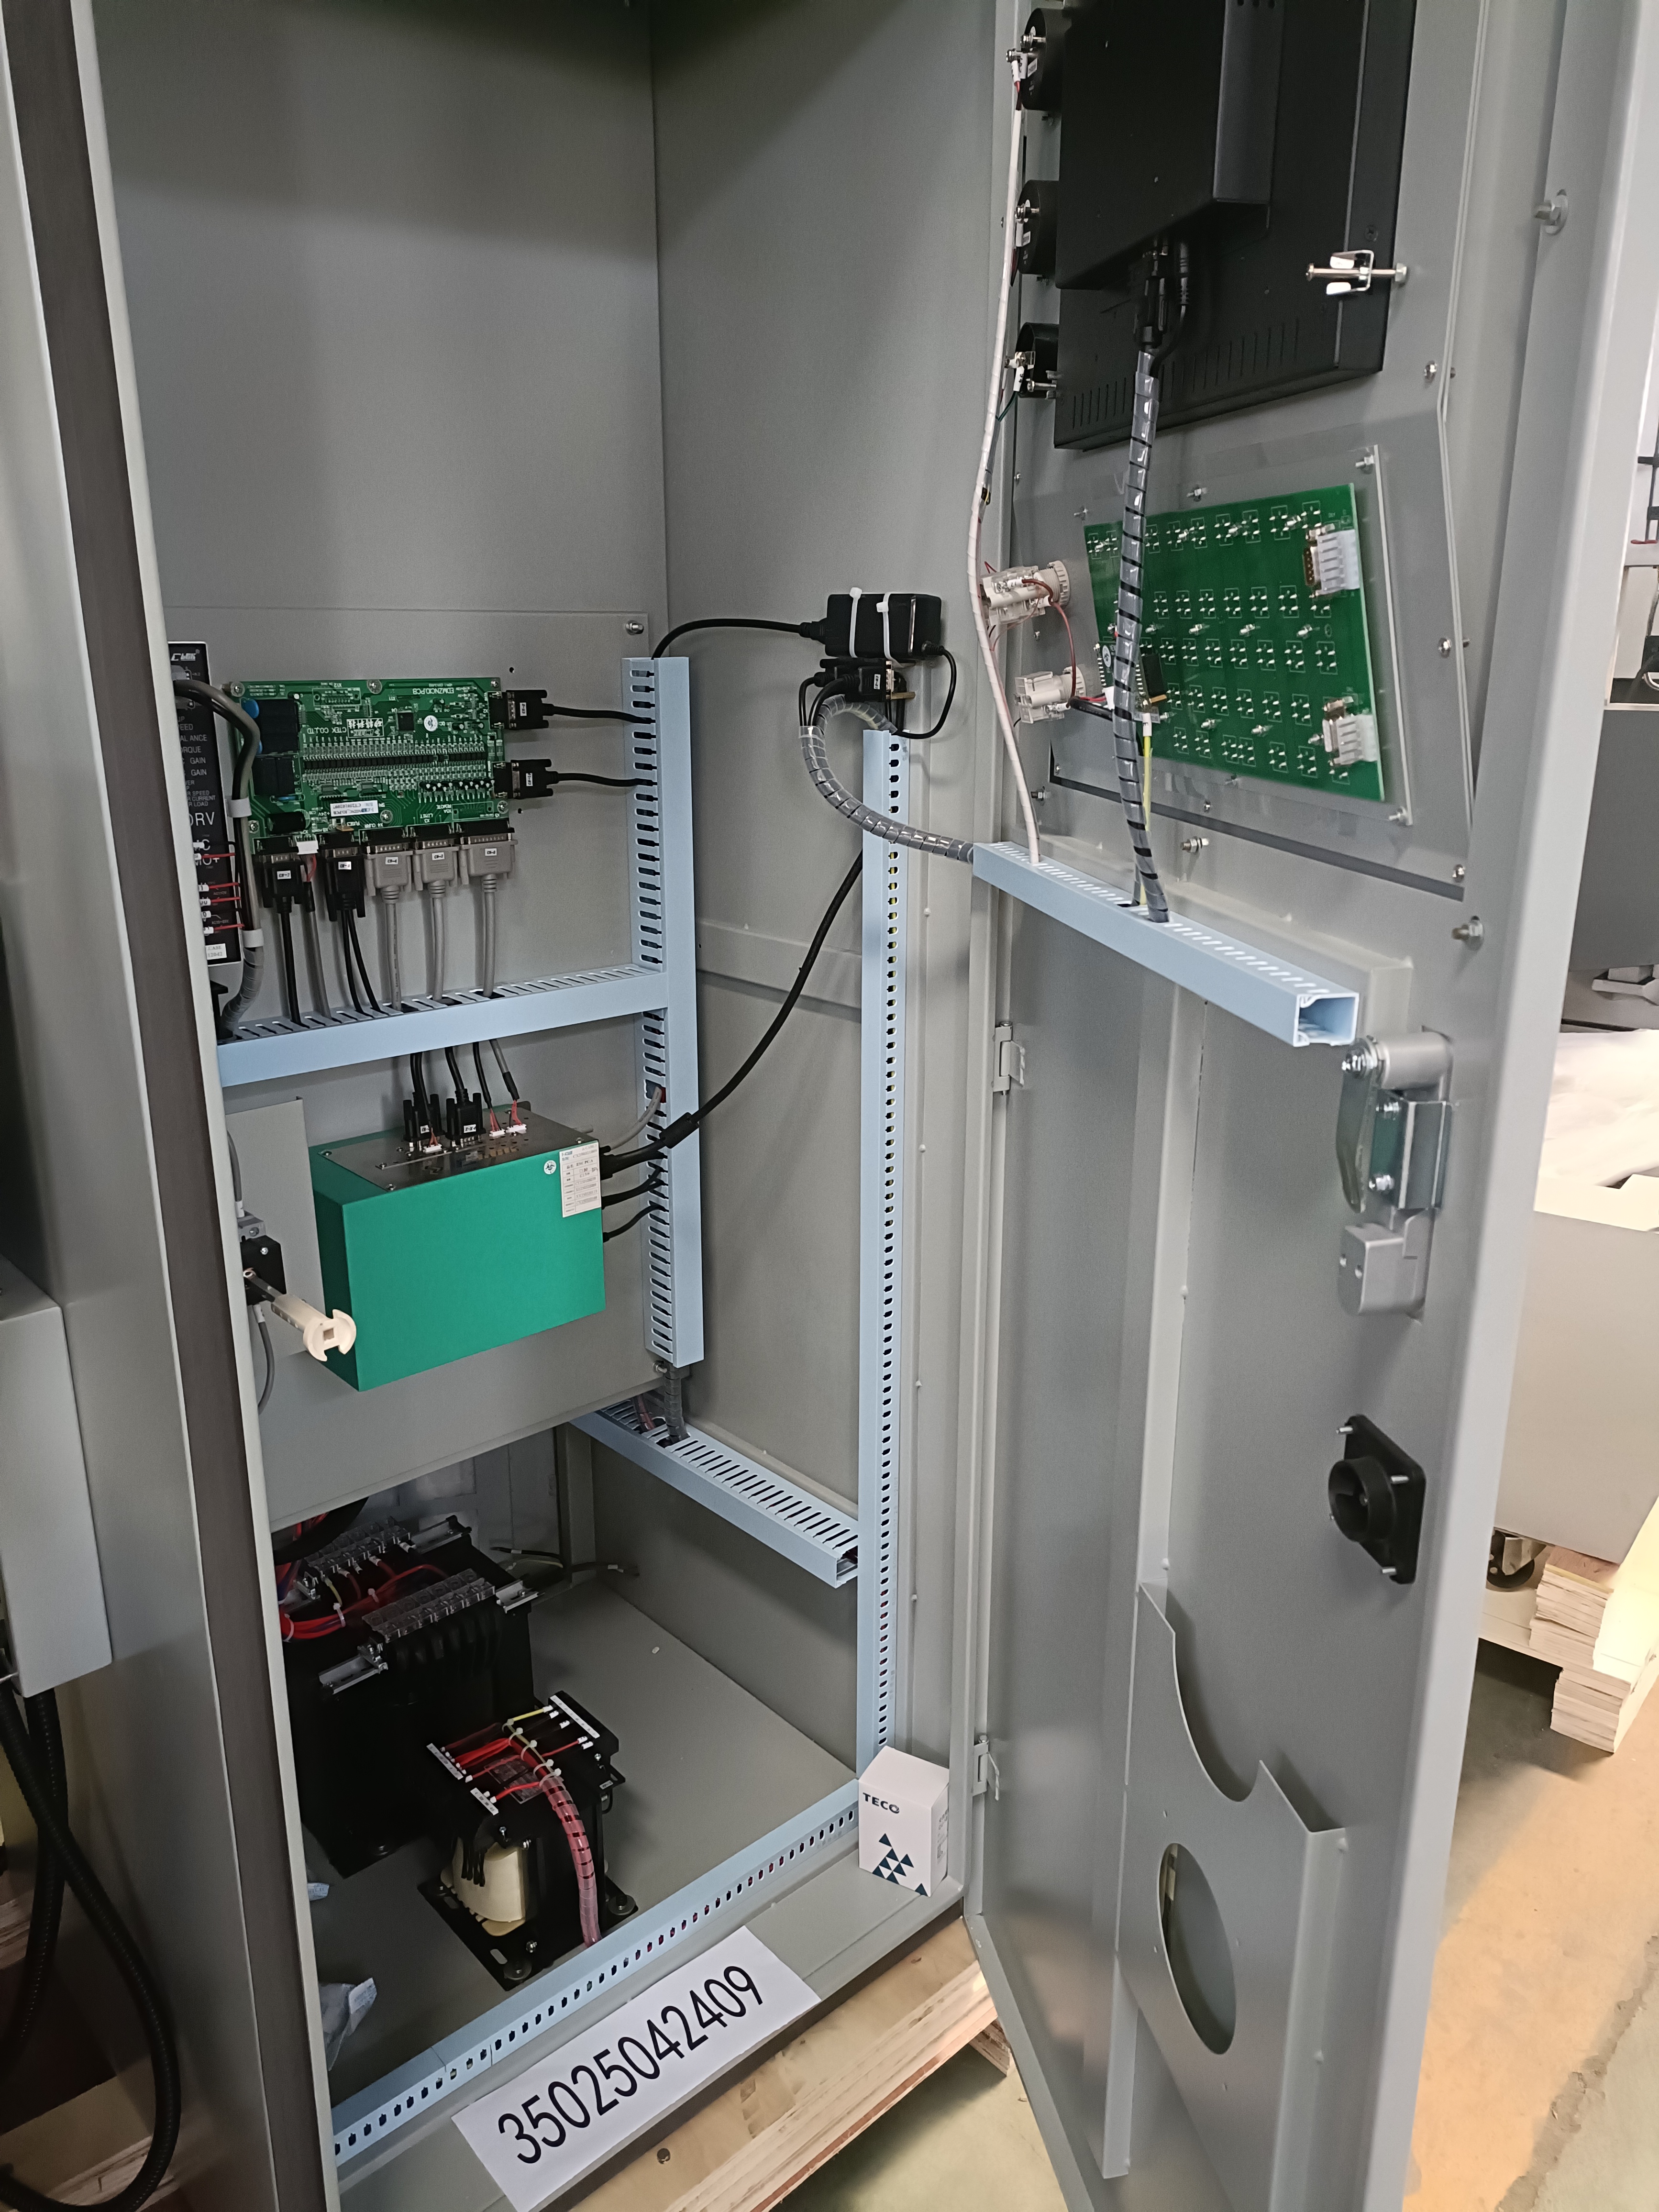
The manufacturing process behind every Mesin CNC EDM Die Sinker begins with finite element analysis of the machine bed, followed by high-grade cast iron casting, natural aging, and vibration stress relief to guarantee long-term geometric stability. The ram, column, and worktable are precision ground and hand scraped to ensure squareness within 0.01 mm per 300 mm. Each spindle assembly is dynamically balanced and tested at rated speed before integration. Electrical cabinets use industrial-grade servo drives, isolated power supplies, and discharge circuits capable of delivering stable pulses from roughing to mirror finishing. Software development runs in parallel, with CNC systems offering multi-axis interpolation, automatic electrode wear compensation, orbit control, and process databases for common materials such as tool steel, carbide, copper, and graphite. Before shipment, every Mesin CNC EDM Die Sinker completes a 72-hour continuous burning test, laser interferometer verification, and a full accuracy report. On the production floor, customers use these machines to cut deep ribs, narrow slots, sharp internal corners, and three-dimensional cavities that milling cannot reach economically. In automotive stamping, shops burn door panels, structural brackets, and progressive die inserts, often achieving cavity cycle reductions of 20 to 40 percent. In medical molding, manufacturers rely on fine-finish circuits to reach Ra 0.2 um and skip manual polishing, protecting sterile surfaces and tight tolerances. In aerospace and energy, tooling teams machine heat-resistant alloys and complex cooling channels with repeatability within +/-0.005 mm. Globally, our Mesin CNC EDM Die Sinker units operate in more than 20 exporting countries and regions, supported by multilingual documentation, remote diagnostics, and regional spare parts stock. Typical energy consumption is optimized to reduce kWh per cavity, while dielectric fluid management and filtration extend consumable life. Training programs combine classroom theory with on-machine practice, enabling operators to master orbiting strategies, electrode compensation, and preventive maintenance within days. By controlling the complete chain from casting to software, Taizhou Chuang Yuan Machine Tool Co., Ltd. ensures consistent quality, faster delivery, and competitive pricing. This vertical integration also allows customized travel, taper angles, and automation interfaces for customers expanding into lights-out manufacturing. Whether a shop produces one large die per month or thousands of small inserts per year, the Mesin CNC EDM Die Sinker platform scales to the workload, protects accuracy over years of service, and delivers measurable gains in cost per part, lead time, and surface quality. Customers frequently report that the combination of robust mechanics, intelligent control, and responsive service makes our Mesin CNC EDM Die Sinker a dependable profit center rather than a mere machine tool.

Frequently Asked Questions

What materials can a Mesin CNC EDM Die Sinker machine effectively?

It machines any electrically conductive material regardless of hardness, including tool steel, hardened die steel up to 62 HRC, carbide, copper alloys, nickel-based superalloys, and titanium. This makes it ideal for mold cavities, stamping dies, and aerospace fixtures where milling struggles.
Standard models hold positioning accuracy of +/-0.005 mm and repeatability of +/-0.003 mm. With on-machine probing and temperature compensation, shops routinely maintain true position within 0.01 mm across long production runs.
Using fine-finish power packs and optimized graphite electrodes, the Mesin CNC EDM Die Sinker reaches Ra 0.2 um, allowing many molds to skip polishing, reducing labor and protecting delicate cavity geometry.
Remote preparation takes about three days. On-site installation, commissioning, and operator training normally require five to seven days, covering orbit strategies, electrode compensation, maintenance, and safety.
We serve more than 20 exporting countries and regions with multilingual manuals, remote diagnostics, regional spare parts stock, and engineer visits. Most spare parts ship within 48 hours to minimize downtime.

Related Articles

How to choose a machining center?

12

Dec

How to choose a machining center?

View More
The correct handling method for insufficient machining accuracy of fast wire cutting machine

13

Dec

The correct handling method for insufficient machining accuracy of fast wire cutting machine

View More
Why modular spring machine supports fast switching of different spring production types

14

Jul

Why modular spring machine supports fast switching of different spring production types

Production Bottlenecks of Traditional Integrated Spring Forming Equipment Modern metal forming manufacturing increasingly features diversified product specifications and mixed batch production. Many production facilities need to process springs ...
View More
Why multi functional edm machine meets mixed mold and part production factory demands

14

Aug

Why multi functional edm machine meets mixed mold and part production factory demands

Navigating the Complexities of High-Mix Manufacturing Environments Running a modern industrial production plant often feels like juggling a dozen spinning plates at once, especially when dealing with high-mix, low-volume manufacturing schedules. Pl...
View More

Customer Testimonials

Daniel Weber, Tooling Manager, Germany
Consistent Accuracy Across Three Shifts

We run two Mesin CNC EDM Die Sinker machines around the clock producing connector molds. Position repeatability has stayed within 0.005 mm for 14 months, electrode wear dropped about 25 percent, and our scrap rate fell below 1 percent. The process library shortened new-program setup from two days to a few hours.

Camila Ferreira, Production Director, Brazil
Fast Support Kept Our Aerospace Contract on Schedule

Our nickel-alloy fixture work demanded tight tolerances and quick service. The Mesin CNC EDM Die Sinker delivered 0.01 mm true position, and a replacement servo arrived in 48 hours, keeping our delivery on time and helping us secure a three-year aerospace contract.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Rigid Machine Structure Ensures Long-Term Mesin CNC EDM Die Sinker Accuracy

Rigid Machine Structure Ensures Long-Term Mesin CNC EDM Die Sinker Accuracy

The base, column, and ram of every Mesin CNC EDM Die Sinker are cast from high-grade iron and subjected to natural aging plus vibration stress relief, removing internal stress that otherwise causes drift after months of operation. Guideways are precision ground, heat treated, and hand scraped to maintain squareness within 0.01 mm per 300 mm. This rigid structure allows stable deep-rib burning, reduces electrode vibration, and protects surface finish even during high-current roughing. In practice, customers report that after three years of two-shift operation, accuracy remains within original specifications without re-scraping. The design also supports heavy workpieces up to several tons, making it suitable for large automotive stamping dies and die-casting molds. Because the structure absorbs discharge reaction forces, operators achieve consistent cavity depth across multi-cavity molds, cutting scrap and rework.
Intelligent CNC Control Raises Mesin CNC EDM Die Sinker Productivity

Intelligent CNC Control Raises Mesin CNC EDM Die Sinker Productivity

Our Mesin CNC EDM Die Sinker uses an industrial CNC system with multi-axis interpolation, automatic electrode wear compensation, and programmable orbit strategies. Operators select material and electrode combinations from a built-in process database, and the machine calculates optimal discharge parameters automatically. This reduces reliance on operator experience and shortens training time. In real installations, setup time fell by up to 35 percent and cavity cycle times dropped 20 to 40 percent compared with manual ram EDM. On-machine probing verifies workpiece position before burning, preventing costly misalignment. Remote diagnostic ports allow our engineers to troubleshoot software issues quickly, while USB and network interfaces simplify program transfer. For shops transitioning to lights-out manufacturing, the control supports automation handshaking and unattended operation.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop