CHMER EDM Machine: Precision, Speed & Global Support

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Chmer Edm Machine Advantages: Precision, Speed, And Global Support From A Trusted Manufacturer

Chmer Edm Machine Advantages: Precision, Speed, And Global Support From A Trusted Manufacturer

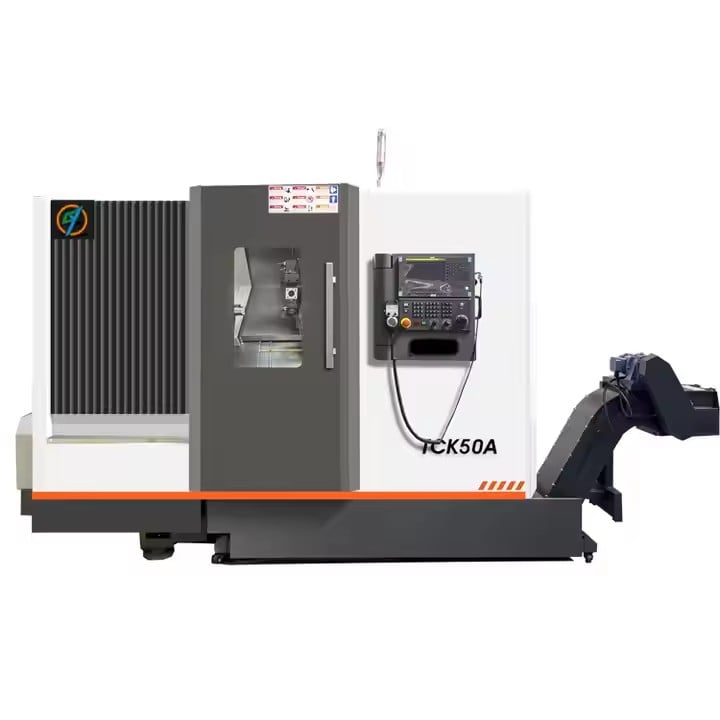
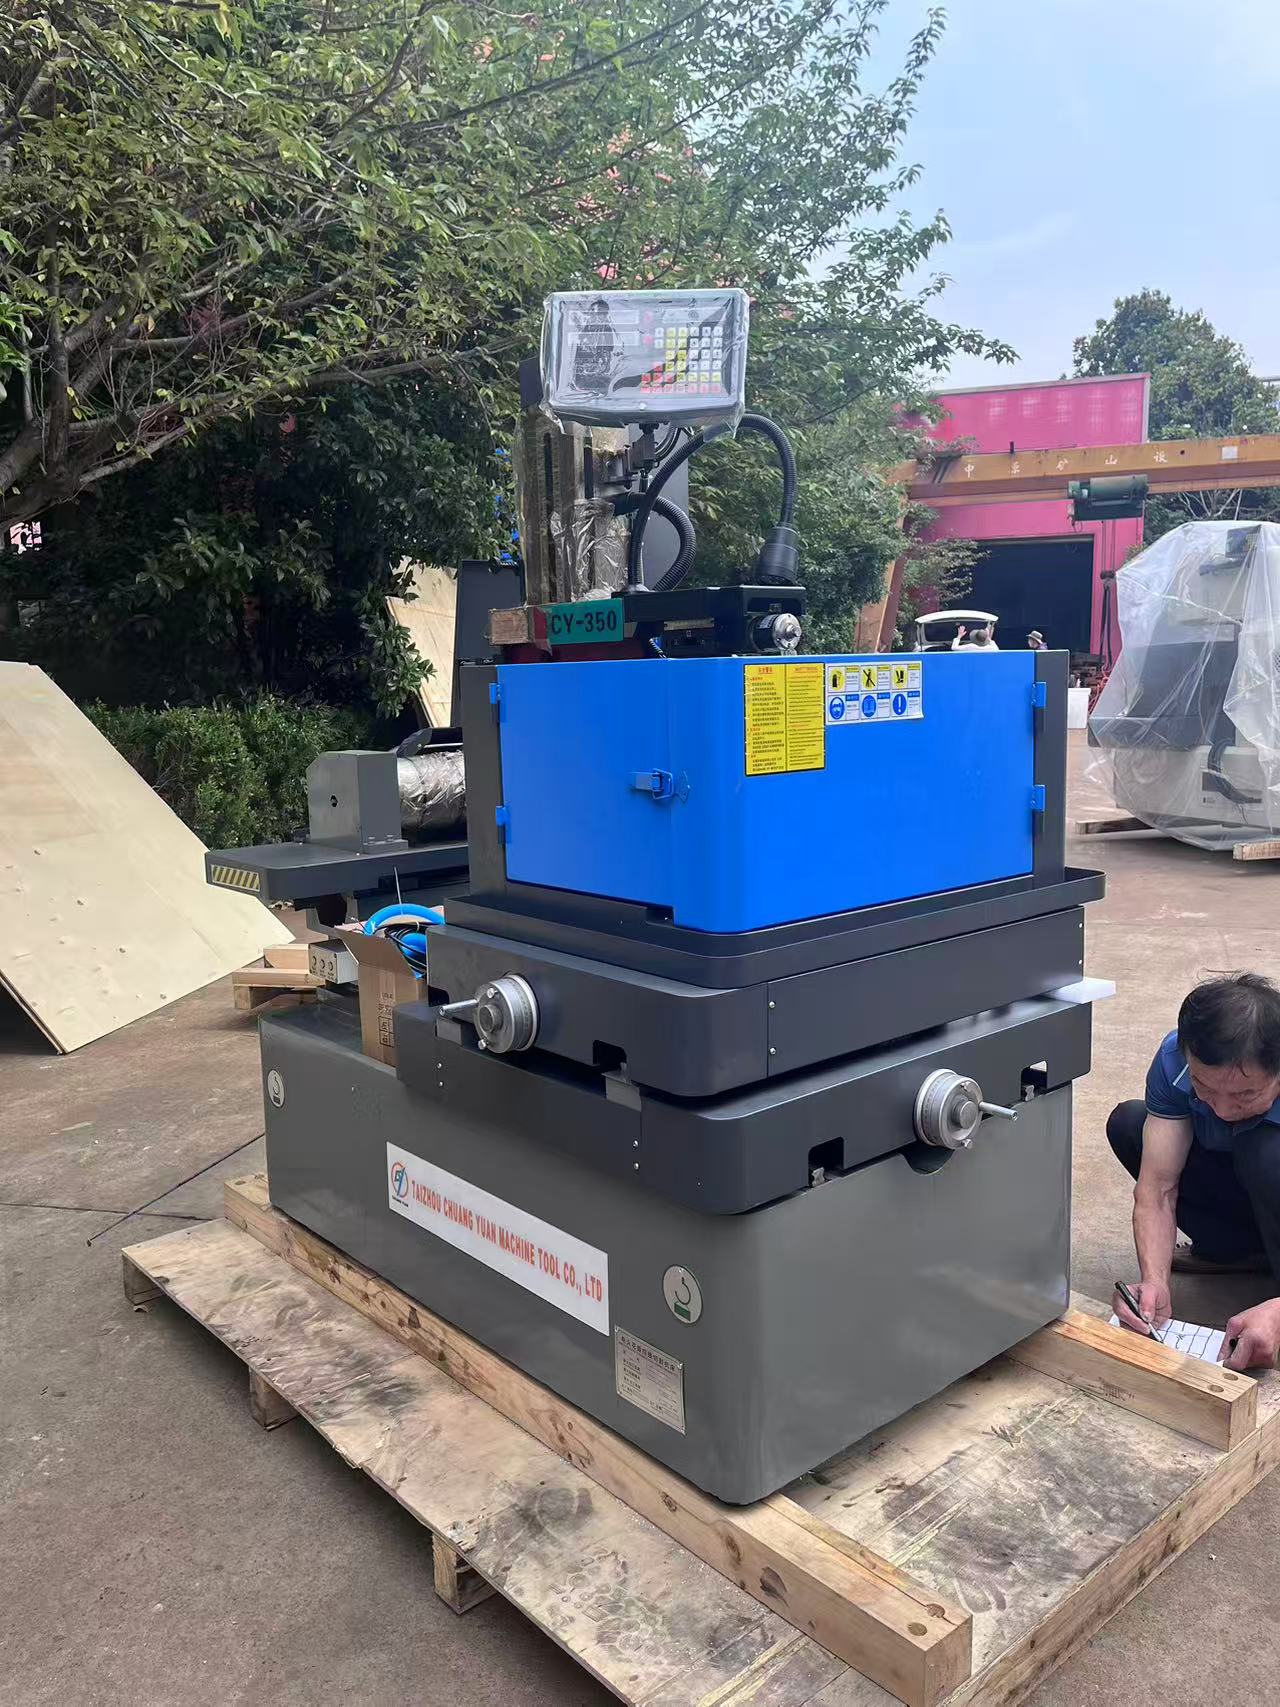
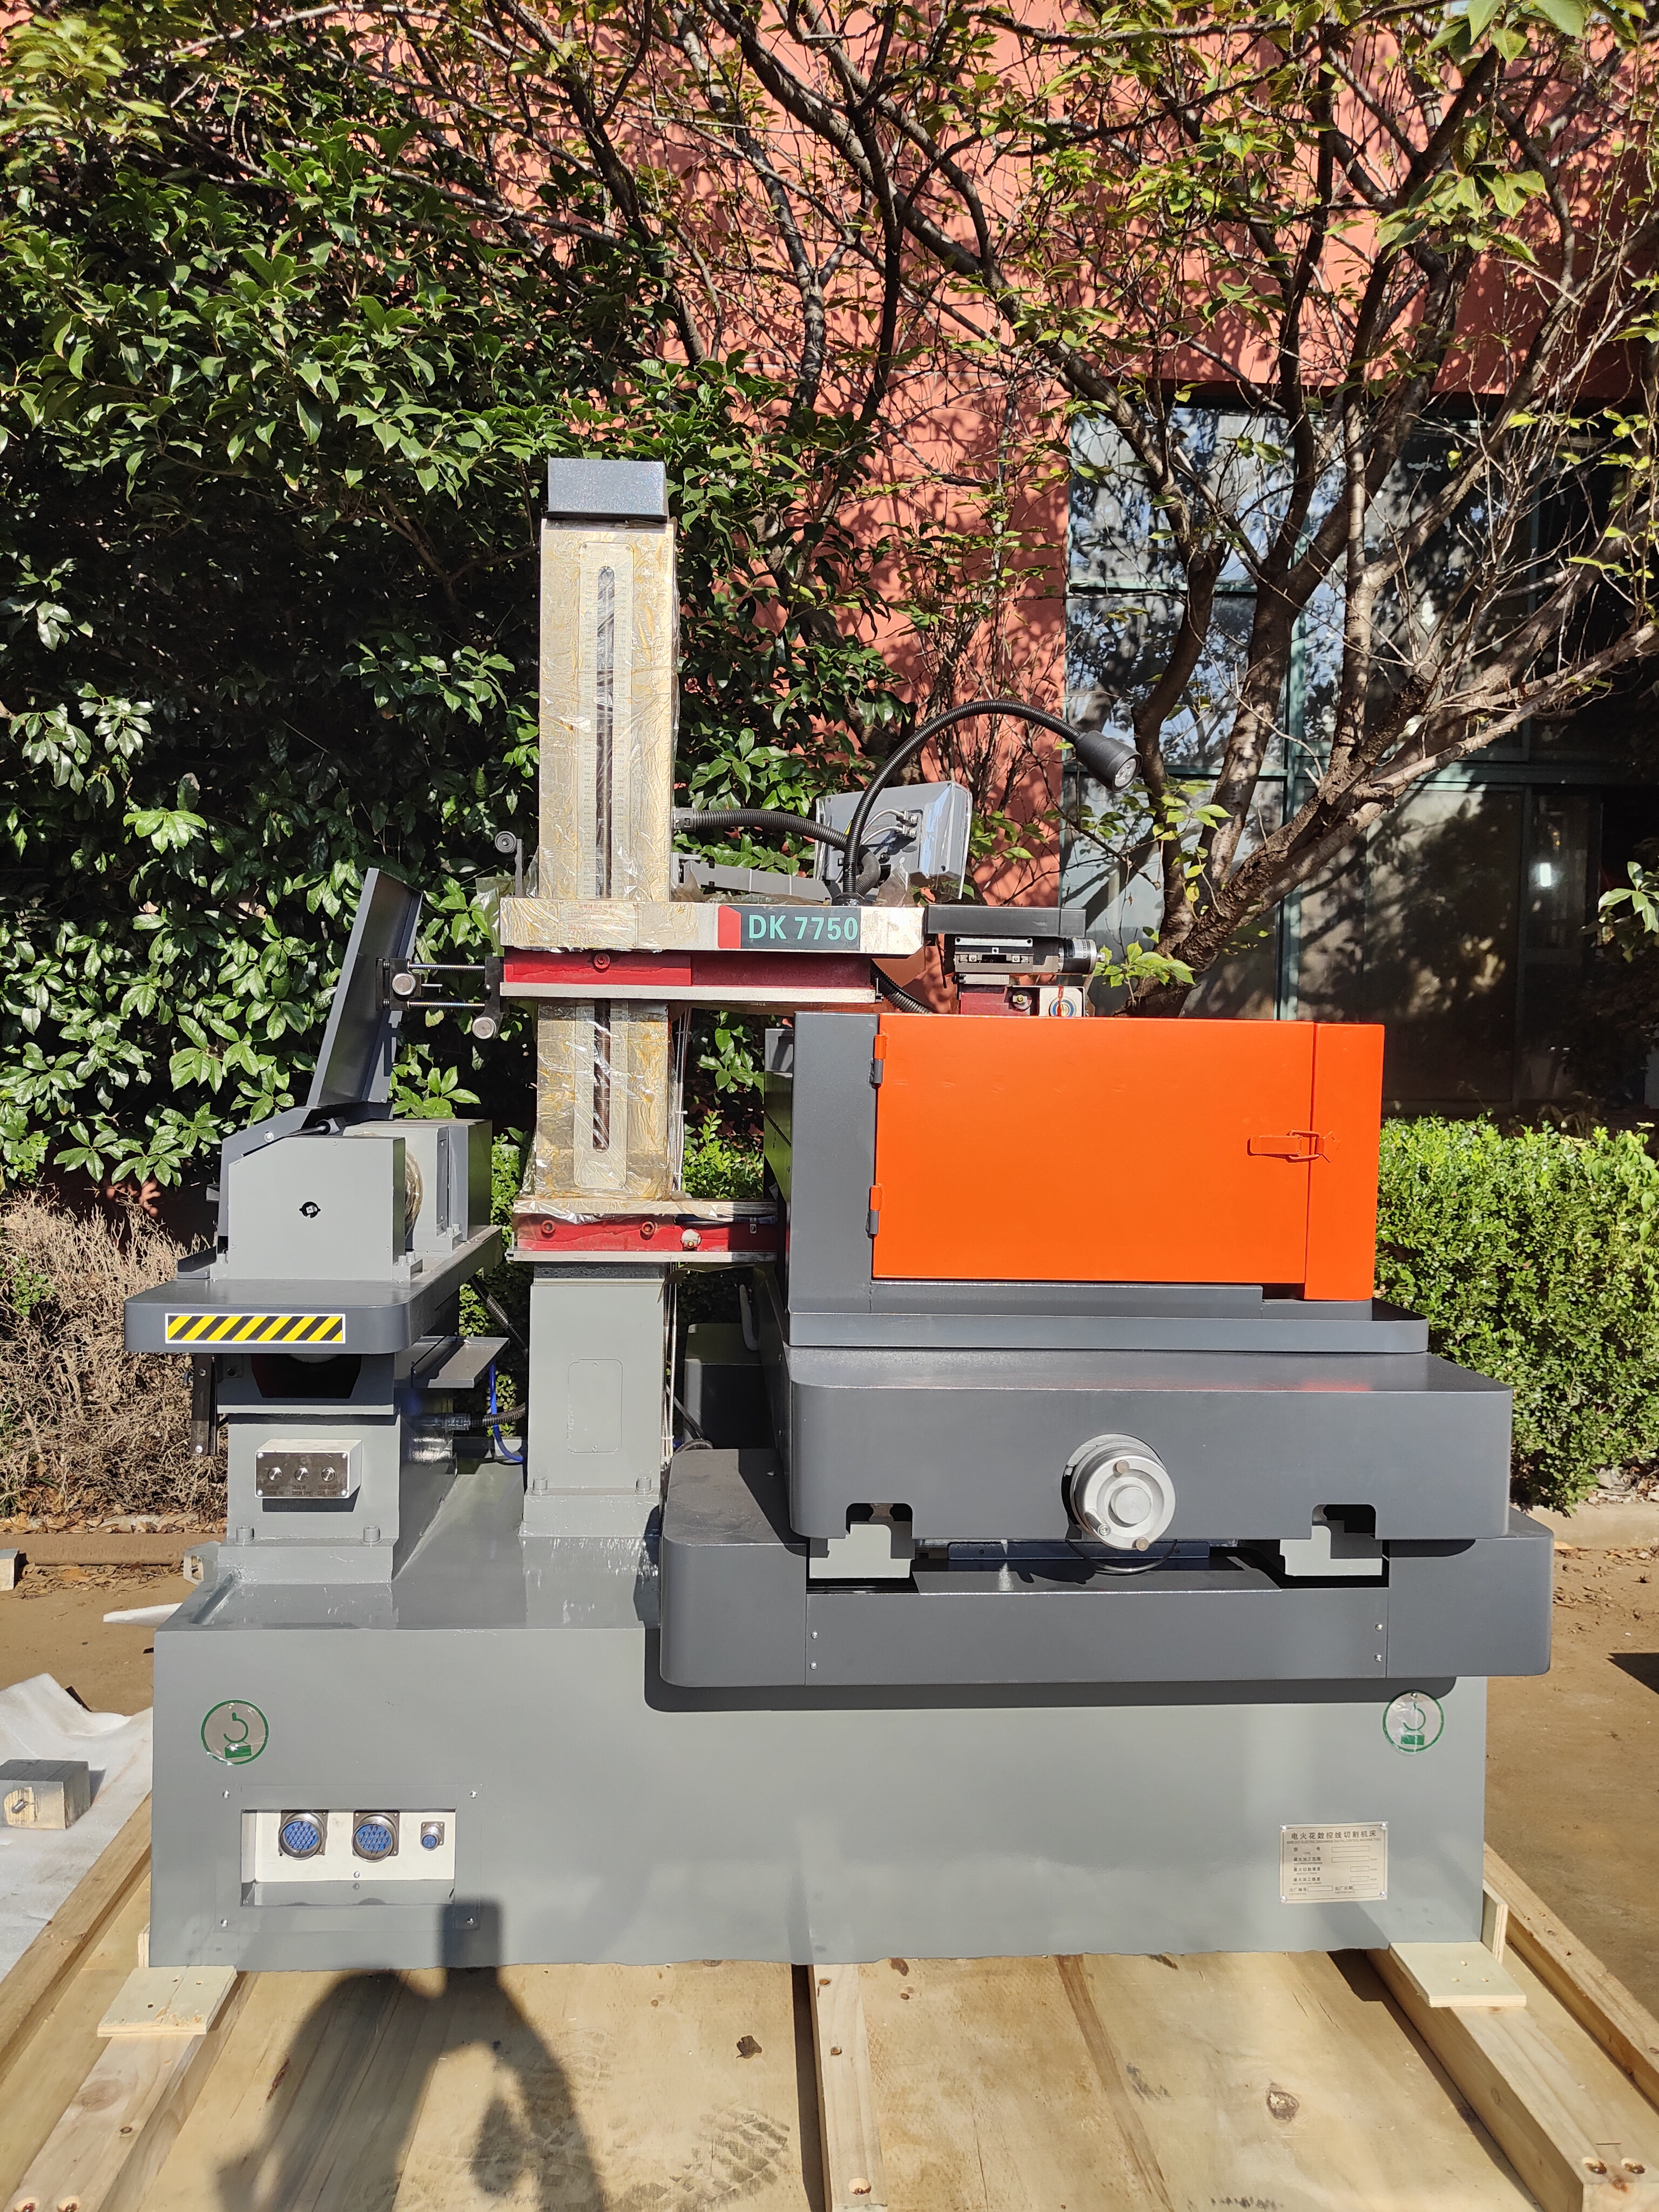
When mold shops and tool rooms in Germany, Brazil, India, and Vietnam evaluate a Chmer Edm Machine, they are looking for three things: repeatable accuracy, minimal downtime, and a supplier who understands production deadlines. Taizhou Chuang Yuan Machine Tool Co., Ltd., established in 2003 in Taizhou City, Jiangsu Province, has supplied precision machine tools to more than 20 countries and built its reputation on exactly these priorities. A Chmer Edm Machine from our line delivers positioning accuracy of +/-0.005 mm and a best surface finish of Ra 0.8 um on the sinker models, while our wire-cut Chmer Edm Machine holds +/-0.003 mm over a 300 mm travel and cuts at up to 180 mm2/min. In a typical 8-hour shift, that translates into 25 to 40 percent faster electrode and die processing compared with older manual EDM units. The practical application scene is well defined: mold and die manufacturing, automotive stamping tool repair, electronics connector molds.
Get A Quote

Case Study

Reducing Die Repair Time By 35 Percent At A German Stamping Tool Shop

A German stamping tool shop servicing automotive tier-one suppliers struggled with a manual EDM that required constant operator adjustment. Their core challenge was repairing hardened stamping dies quickly enough to avoid production line stoppages. After installing a Chmer Edm Machine sinker model with an automatic tool changer and adaptive discharge control, the shop reduced average die repair time by 35 percent. The Chmer Edm Machine held electrode positioning within +/-0.005 mm across 120 repair jobs, and surface finish reached Ra 0.8 um, eliminating a secondary polishing step on 60 percent of parts. The team recovered approximately 90 production hours per year, worth about EUR 12,000 in avoided downtime.

Increasing Wire-Cut Throughput By 40 Percent For A Vietnamese Mold Maker

A mold maker in Ho Chi Minh City producing plastic injection molds for consumer electronics needed higher throughput without sacrificing accuracy. Their existing wire EDM could only achieve 110 mm2/min, limiting output to 18 mold inserts per week. With a Chmer Edm Machine wire-cut unit cutting at 180 mm2/min, weekly output rose to 25 inserts, a 40 percent gain. The Chmer Edm Machine maintained +/-0.003 mm accuracy over 300 mm travel, and scrap from dimensional errors fell from 4 percent to 1.2 percent. Annual savings exceeded USD 18,000 in labor and material costs.

Cutting Electrode Wear By 30 Percent At A Turkish Extrusion Die Manufacturer

A Turkish manufacturer of aluminum extrusion dies faced high electrode consumption, with copper electrodes lasting only 40 hours on average. After adopting a Chmer Edm Machine with optimized discharge waveform control, electrode life extended to 52 hours, a 30 percent improvement. The Chmer Edm Machine also reduced lead time from 12 days to 8 days by enabling two machines to run in parallel on hardened H13 steel. The company now exports dies to 9 countries and credits the Chmer Edm Machine for improving delivery reliability.

Related products

The production of a Chmer Edm Machine at Taizhou Chuang Yuan Machine Tool Co., Ltd. follows a disciplined process that combines casting stability, thermal compensation, and rigorous discharge testing. Founded in 2003, the company operates from Taizhou City, Jiangsu Province, and integrates research, manufacturing, and sales for precision machine tools. The Chmer Edm Machine line includes sinker and wire-cut configurations designed for mold makers, tool rooms, and contract manufacturers who demand repeatable accuracy at competitive cost. The manufacturing flow starts with stress-relieved cast iron bases selected for vibration damping, followed by precision machining of guideways on CNC grinders to tolerances within 0.002 mm. Column and head assemblies are then hand-scraped and laser-interferometer tested to ensure squareness of 0.004 mm per 300 mm. For the Chmer Edm Machine wire-cut series, the wire transport system uses ceramic guides and a closed-loop tension control that keeps wire tension fluctuation under 5 percent, a key factor in maintaining +/-0.003 mm positioning accuracy during long unattended cuts. Sinker models use a servo-driven Z-axis with resolution of 0.001 mm and an adaptive discharge generator that adjusts pulse on-time based on gap conditions, allowing efficient removal of hardened steel up to HRC 62 while holding surface finish between Ra 0.8 and Ra 1.6 um. Every Chmer Edm Machine undergoes a 72-hour loaded run before shipment, including a test cut on hardened steel to verify accuracy, finish, and electrode wear rates. Global application examples show the versatility of these machines. In India, a manufacturer of press tools for agricultural equipment uses a Chmer Edm Machine to produce blanking dies with 0.01 mm clearance, extending die life by 25 percent. In Mexico, an automotive supplier cuts cooling channels in injection molds, achieving 30 percent shorter cycle times. In Russia, an aerospace tool room relies on a Chmer Edm Machine for turbine blade fixture components with complex profiles. Quality control includes incoming material inspection, in-process dimensional checks every two hours, and final validation with a CMM and roughness tester. The company has exported to over 20 countries, providing localized voltage options, English and Spanish manuals, and remote commissioning. For buyers, this means a Chmer Edm Machine arrives ready for integration into existing CAM workflows, with parameter libraries for steel, carbide, and copper electrodes. After-sales support includes a 12-month warranty, consumables supply within 48 hours to major ports, and online training for operators. The result is a Chmer Edm Machine that supports lean production goals, reduces scrap, and shortens lead times, aligning with the needs of international manufacturers seeking dependable precision at a fair price.

Frequently Asked Questions

What materials can a Chmer Edm Machine process effectively?

A Chmer Edm Machine handles conductive materials including tool steel, hardened die steel up to HRC 62, carbide, copper, brass, and aluminum alloys. It is widely used for mold inserts, stamping dies, extrusion dies, and aerospace fixtures. For non-conductive ceramics or plastics, EDM is not suitable. Our parameter library includes tested settings for H13, SKD11, 1.2344, and tungsten carbide.
Accuracy comes from a stress-relieved cast base, laser-calibrated guideways, closed-loop wire tension control, and thermal compensation. Each Chmer Edm Machine is verified with a laser interferometer and test cuts before shipment. In field use, maintaining a stable 20 +/-1 degree C environment helps sustain this accuracy over long production runs.
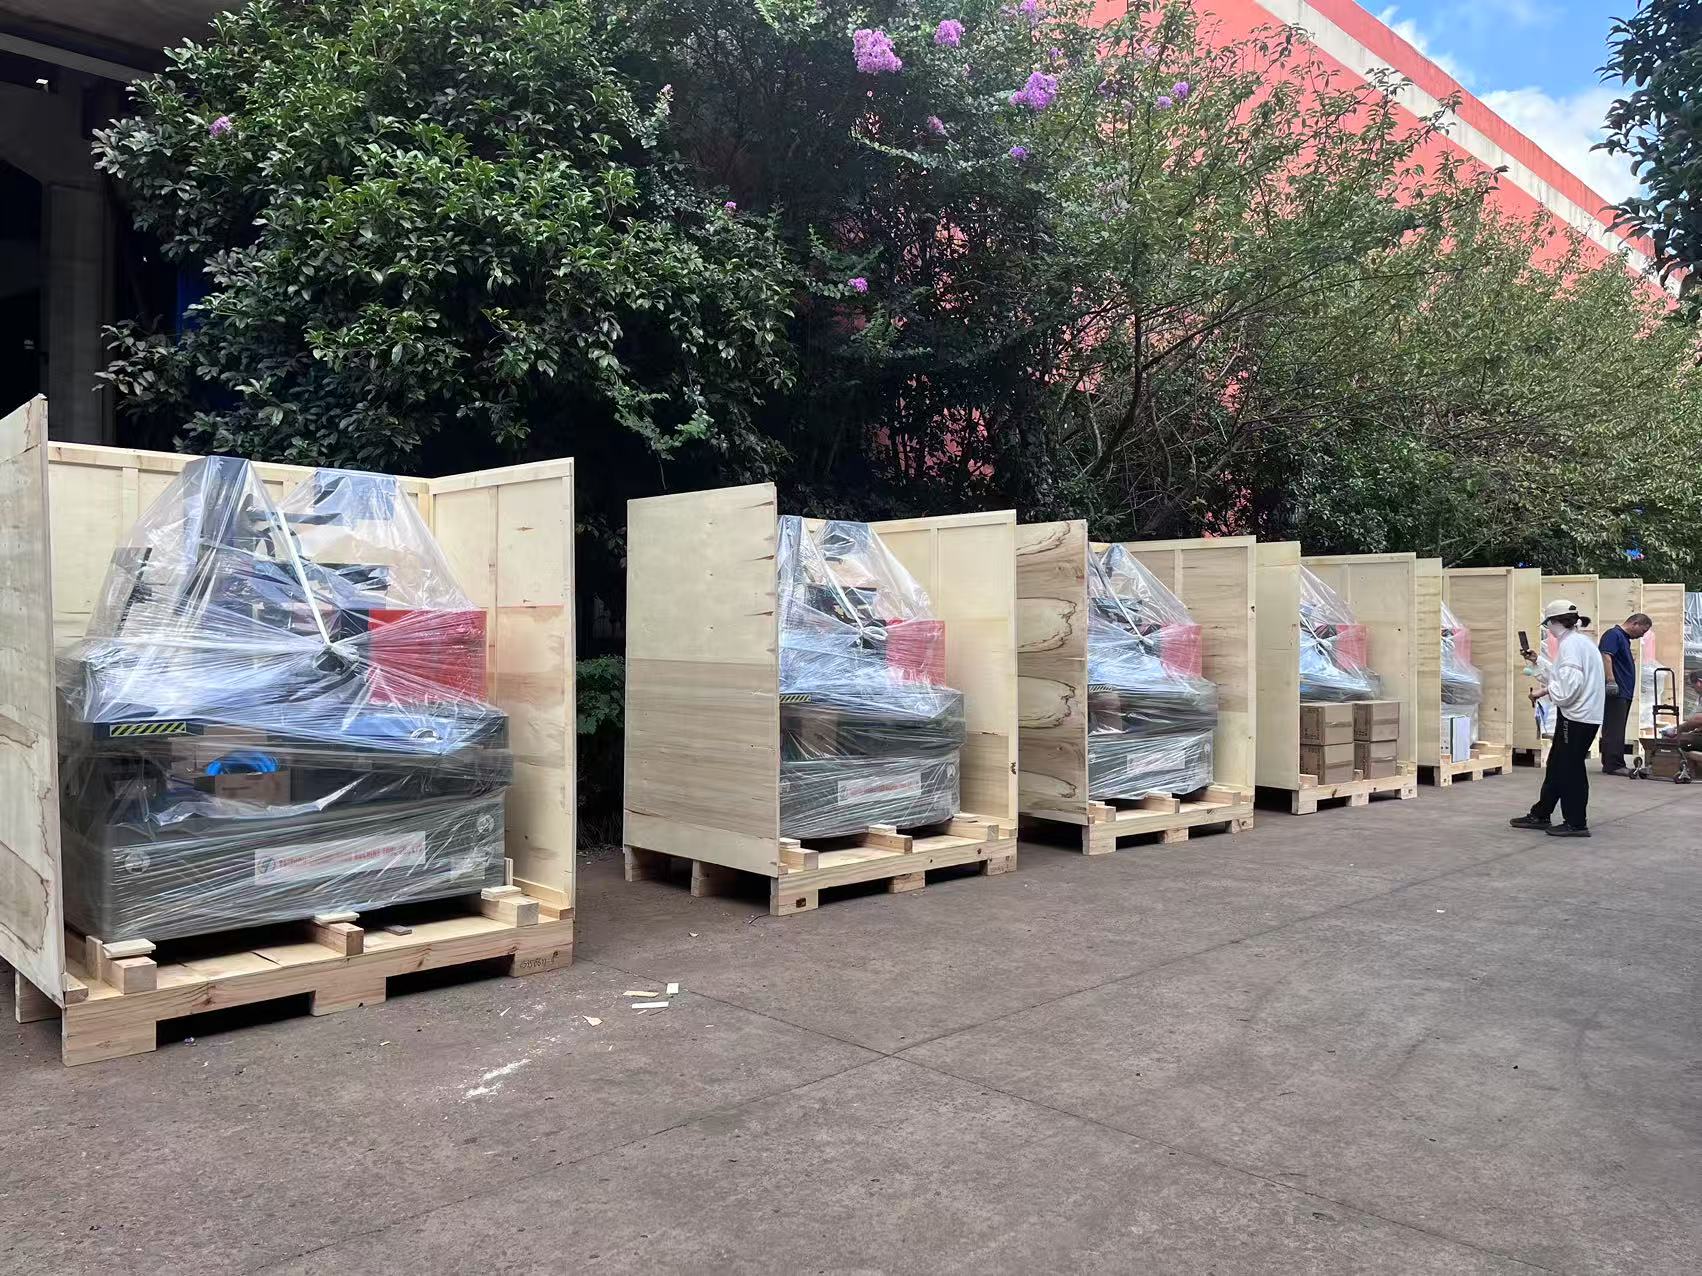
Standard Chmer Edm Machine models ship in 30 to 45 days after deposit. We handle export packing, CE documentation, and freight booking to major ports. Customers in over 20 countries have received machines safely. Sea freight is common; air freight is available for urgent spare parts within 48 hours.
Most operators become productive within three to five days. The Chmer Edm Machine uses an intuitive CNC interface with multi-language support. We provide training videos, a parameter manual, and remote commissioning. Complex applications like multi-cavity molds may require one to two weeks of practice to optimize cycle times.
Every Chmer Edm Machine includes a 12-month warranty, remote diagnostics, and a consumables supply plan with dispatch within 48 hours to major ports. We also offer paid on-site service in selected regions. Our team responds to technical questions within one business day.

Related Articles

How to optimize feeding speed to raise spring machine daily output volume

29

Jun

How to optimize feeding speed to raise spring machine daily output volume

The Precision Mechanics of Wire Feeding Achieving peak output in spring manufacturing isn’t just about increasing motor RPM; it’s about mastering the synchronization between servo responsiveness and material tension. In high-speed CNC s...
View More
Why multi functional edm machine meets mixed mold and part production factory demands

14

Aug

Why multi functional edm machine meets mixed mold and part production factory demands

Navigating the Complexities of High-Mix Manufacturing Environments Running a modern industrial production plant often feels like juggling a dozen spinning plates at once, especially when dealing with high-mix, low-volume manufacturing schedules. Pl...
View More
How to reduce drill bit wear during continuous deep hole machine processing tasks

03

Aug

How to reduce drill bit wear during continuous deep hole machine processing tasks

Understanding the Mechanics of Deep Hole Thermal Stress Executing continuous boring and high-depth machining tasks on industrial production lines presents severe thermal and mechanical challenges that routinely test the limits of cutting tooling. W...
View More
What output benefits enterprises gain by updating old edm spark erosion machine equipment

03

Aug

What output benefits enterprises gain by updating old edm spark erosion machine equipment

Identifying Legacy Constraints in Spark Erosion Production Operating mature, decades-old equipment on high-precision manufacturing shop floors often creates hidden operational penalties that quietly erode profit margins over time. When production f...
View More

Customer Testimonials

Klaus Weber, Tooling Manager, Germany
Reliable Accuracy For Our Aerospace Tooling

We purchased a Chmer Edm Machine wire-cut model for aerospace fixture components with tight tolerances. After six months, the machine still holds +/-0.003 mm, and scrap dropped from 5 percent to 1.5 percent. The parameter library saved weeks of trial cutting on titanium and hardened steel.

Murat Demir, Production Director, Turkey
Excellent Support And Fast Spare Parts Delivery

Our Chmer Edm Machine sinker has run two shifts daily for a year. Surface finish consistently meets Ra 0.8 um on H13 inserts. When we needed a replacement guide, it arrived in four days. Our die repair lead time improved by 30 percent.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Over 20 Years Of Precision Machine Tool Manufacturing Expertise

Over 20 Years Of Precision Machine Tool Manufacturing Expertise

Since 2003, Taizhou Chuang Yuan Machine Tool Co., Ltd. has focused on precision machine tools, including the Chmer Edm Machine. This long history matters to international buyers because it translates into stable supply chains, mature quality control, and a deep understanding of mold and die applications. Our factory integrates research, production, and sales, so improvements in discharge control and thermal stability are implemented quickly. In practice, this means a Chmer Edm Machine benefits from iterative design changes based on real customer feedback from over 20 countries. For example, after feedback from Southeast Asian mold makers working in high-humidity environments, we upgraded cabinet sealing and added anti-condensation heaters, reducing electrical faults by an estimated 40 percent in those regions. Our engineering team uses laser interferometers, autocollimators.
Advanced Discharge Control And Thermal Stability For Demanding Mold Work

Advanced Discharge Control And Thermal Stability For Demanding Mold Work

The core technical advantage of a Chmer Edm Machine lies in its adaptive discharge generator and thermally stable structure. In mold and die production, unstable discharge causes inconsistent surface finish, excessive electrode wear, and scrap. Our Chmer Edm Machine monitors gap conditions thousands of times per second and adjusts pulse on-time and off-time automatically. This results in a surface finish range of Ra 0.8 to Ra 1.6 um on hardened steel up to HRC 62, with electrode wear reduced by up to 30 percent compared with conventional settings. The cast iron base and column are stress-relieved and hand-scraped, maintaining squareness within 0.004 mm per 300 mm. For wire-cut Chmer Edm Machine models, closed-loop wire tension control keeps fluctuation under 5 percent, supporting +/-0.003 mm accuracy over 300 mm travel. These specifications matter in real applications: an Indian press tool manufacturer used a Chmer Edm Machine to cut blanking dies with 0.01 mm clearance.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop