Drilling EDM Machine: 55% Faster Micro-Hole Machining

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Proven Drilling EDM Machine Results In Demanding Industries

Proven Drilling EDM Machine Results In Demanding Industries

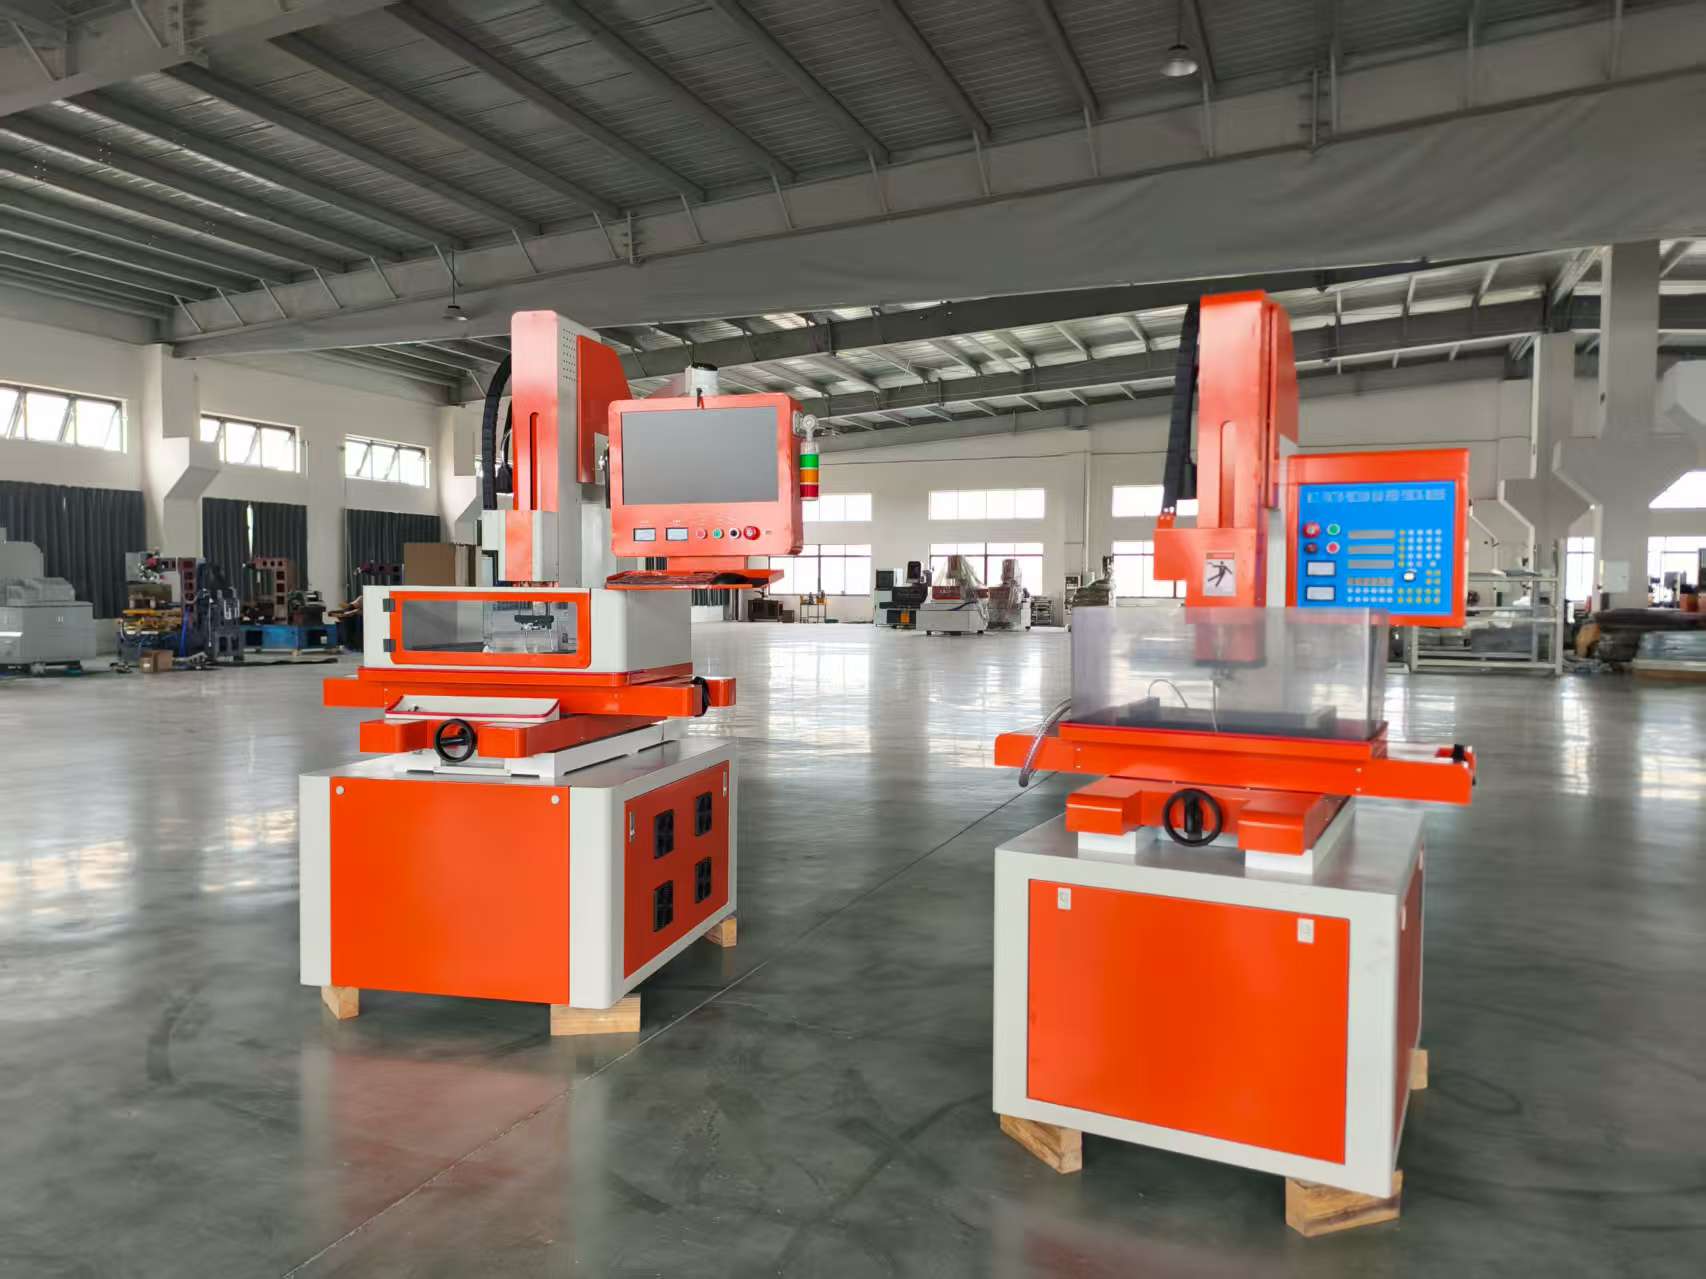
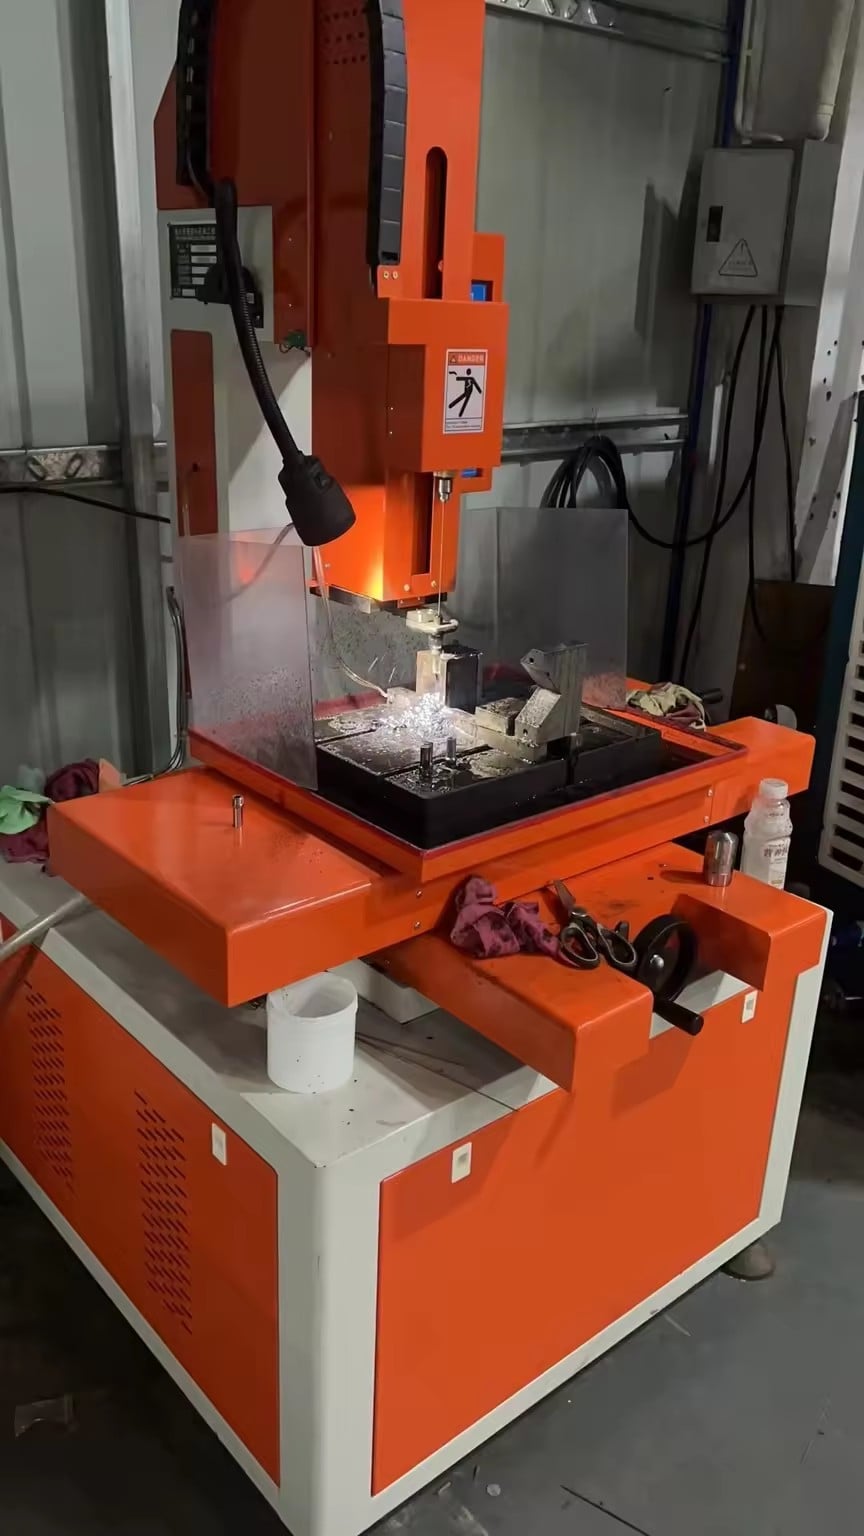
As a professional manufacturer established in 2003 in Taizhou City, Jiangsu Province, China, Taizhou Chuang Yuan Machine Tool Co., Ltd. integrates research and development, production, and sales of precision machine tools. Our Drilling EDM Machine, also known as a small hole drilling EDM, is engineered for fast, precise, and stable drilling of small deep holes in conductive materials such as hardened steel, carbide, copper, and aluminum alloys. It is widely used in mold making, aerospace, automotive, medical device, and electronics manufacturing. In mold shops, operators use it to drill water lines, ejector pin holes, and wire-cut start holes with diameters from 0.15 mm to 3.0 mm and a depth-to-diameter ratio up to 300:1. Our machines achieve a best surface roughness of Ra 0.8 μm, positioning accuracy of ±0.005 mm, and a maximum removal rate of 30 mm³/min, which shortens hole processing time by 40-60% compared with conventional drilling on hardened materials.
Get A Quote

Case Study

融合先进技术,驱动业务增长与数字化转型。

Reducing Turbine Blade Cooling Hole Time By 55% For A German Aerospace Supplier

A German aerospace supplier needed to drill hundreds of cooling holes in nickel-based turbine blades with diameters of 0.4-0.6 mm and depths of 8-10 mm. Their existing process required frequent electrode changes and caused recast layers and taper. We recommended our Drilling EDM Machine with a high-frequency pulse generator, automatic electrode changer, and customized process parameters. Using 0.5 mm brass electrodes and our optimized pulse width, the machine achieved a removal rate of 22 mm³/min and a hole taper below 0.03 mm. Cycle time dropped from 14 minutes to 6.3 minutes per blade, a 55% reduction, and recast layer thickness was controlled below 5 μm. After a two-week trial, the customer ordered six units and standardized our machine across three production lines. They reported annual savings of over 120,000 EUR and improved first-pass yield from 88% to 97%, confirming the Drilling EDM Machine as a reliable competitive advantage.

Cutting Electrode Cost By 38% For An Indian Mold Maker

An Indian mold maker producing plastic injection molds for automotive interiors struggled with high electrode consumption and frequent hole misalignment on hardened H13 steel. They used a 1.0 mm copper tube to drill 150 mm deep water lines. Our Drilling EDM Machine, equipped with a servo-controlled Z-axis and built-in depth control, maintained stable discharge and reduced electrode wear by 38%. The average drilling time per hole fell from 9 minutes to 4.5 minutes. The customer also used our recommended tungsten carbide guide to improve hole straightness and reduced secondary machining. Within six months, the shop increased mold output by 30% and lowered tooling costs by 15,000 USD annually. This case demonstrates how the Drilling EDM Machine solves deep-hole challenges and improves profitability for mold makers.

Raising Nozzle Production Capacity By 45% For A Turkish Automotive Parts Manufacturer

A Turkish automotive parts manufacturer needed to produce fuel injector nozzles with 0.2 mm holes and a strict tolerance of ±0.003 mm. Their previous EDM process produced inconsistent hole diameters and high scrap rates. We supplied a Drilling EDM Machine with a precision rotary spindle, fine servo control, and an automatic electrode dressing unit. The machine achieved a surface finish of Ra 0.6 μm and a hole diameter repeatability of ±0.002 mm. Production capacity increased by 45%, from 800 to 1,160 nozzles per shift, and scrap rate decreased from 6% to 1.2%. The customer now operates four of our Drilling EDM Machines and exports nozzles to European markets. This project highlights our ability to customize the Drilling EDM Machine for micro-hole applications and deliver measurable quality gains. Drilling EDM Machine Product Showcase: Engineered For Micro-Hole Precision And High-Volume Production

Related products

Drilling EDM Machine Manufacturing Process And Global Application Expertise

Taizhou Chuang Yuan Machine Tool Co., Ltd. has specialized in precision machine tools since 2003. Our Drilling EDM Machine is developed, produced, and tested in our facility in Taizhou City, Jiangsu Province, China, where we control the complete manufacturing chain from casting and machining to assembly and final inspection. The production process begins with high-grade cast iron bases that are stress-relieved and precision-milled to ensure structural rigidity and long-term stability. The spindle, servo system, and dielectric circulation unit are assembled in a temperature-controlled workshop. Each machine undergoes a 72-hour continuous running test, laser interferometer calibration, and a full accuracy inspection according to ISO standards. Our research and development team continuously improves the pulse power supply, servo control algorithm, and automatic tool changer to meet the evolving needs of mold making, aerospace, automotive, medical, and electronics industries. In mold making, customers use the Drilling EDM Machine to create wire-cut start holes, water lines, and ejector pin holes in hardened steel, reducing reliance on skilled manual drilling. In aerospace, the machine drills cooling holes in turbine blades and combustor liners with diameters as small as 0.15 mm and depth-to-diameter ratios up to 300:1. In medical device manufacturing, it produces micro-holes in surgical instruments and implant components with burr-free edges. In electronics, it drills via holes in ceramic substrates and connector molds. Our quality management system covers incoming material inspection, in-process monitoring, and final performance testing. We maintain a large inventory of standard electrode tubes, guides, and spare parts to ensure fast delivery and minimal downtime. For international customers, we provide English technical manuals, remote video commissioning, and on-site training. Our engineers have supported installations in over 20 countries, including Germany, India, Turkey, Vietnam, Mexico, and Brazil. By combining advanced manufacturing, rigorous testing, and responsive service, we ensure that every Drilling EDM Machine delivers consistent accuracy, high removal rates, and long service life. Our commitment to innovation and customer satisfaction has made us a trusted partner for manufacturers seeking reliable small hole drilling EDM solutions worldwide.

Frequently Asked Questions

What materials can a Drilling EDM Machine process?

A Drilling EDM Machine can process any electrically conductive material, including hardened steel, tool steel, carbide, copper, brass, aluminum, titanium, and superalloys. It is ideal for materials that are difficult to cut with conventional drilling, such as H13, SKD61, and nickel-based alloys. Non-conductive materials like ceramics or glass cannot be processed directly. For best results, we provide recommended parameters for each material and can supply sample testing before purchase.
Our standard Drilling EDM Machine can drill holes from 0.15 mm to 3.0 mm in diameter. With optional precision guides and optimized parameters, the depth-to-diameter ratio can reach 300:1, for example a 0.5 mm hole up to 150 mm deep. Actual performance depends on material, electrode type, and flushing conditions. We can recommend the right configuration based on your specific hole requirements.
We use a high-precision servo control system, a high-frequency pulse power supply, and a rigid machine structure to achieve positioning accuracy of ±0.005 mm and hole diameter repeatability of ±0.002 mm. Surface roughness can reach Ra 0.6-0.8 μm. Each machine is laser-calibrated and tested before shipment. We also provide on-site or remote parameter optimization to help you achieve consistent results.
We provide English operation manuals, remote video commissioning, and on-site installation and training when required. Our engineers respond within 24 hours to technical inquiries. We maintain a spare parts inventory for fast shipment and offer process support for new applications. With customers in over 20 countries, we understand international service expectations and work to minimize downtime.
Standard Drilling EDM Machine models are delivered within 30-45 days after deposit, depending on configuration. Customized solutions may take 60-75 days. We offer a 12-month warranty on main components and lifetime technical support. We also provide optional extended warranty and preventive maintenance packages to ensure long-term reliability and productivity.

Related Articles

How to choose a machining center?

12

Dec

How to choose a machining center?

View More
Why modular spring machine supports fast switching of different spring production types

14

Jul

Why modular spring machine supports fast switching of different spring production types

Production Bottlenecks of Traditional Integrated Spring Forming Equipment Modern metal forming manufacturing increasingly features diversified product specifications and mixed batch production. Many production facilities need to process springs ...
View More
Why multi functional edm machine meets mixed mold and part production factory demands

14

Aug

Why multi functional edm machine meets mixed mold and part production factory demands

Navigating the Complexities of High-Mix Manufacturing Environments Running a modern industrial production plant often feels like juggling a dozen spinning plates at once, especially when dealing with high-mix, low-volume manufacturing schedules. Pl...
View More
What export quality standards international clients require for wire cutting machine products

03

Aug

What export quality standards international clients require for wire cutting machine products

Understanding International Export Compliance in Precision Machining Navigating the complex landscape of global industrial trade requires a thorough understanding of the stringent technical benchmarks that overseas buyers mandate for advanced metal...
View More

Customer Testimonials

Johann Becker, Production Manager, Germany
Reliable Accuracy And Excellent Support

We purchased two Drilling EDM Machines for our mold shop in Germany. The machines have been running three shifts for 18 months with minimal maintenance. Hole accuracy is consistently within ±0.005 mm, and our electrode consumption dropped by 35%. The remote support team helped us optimize parameters for hardened steel, and we reduced cycle time by 40%. We highly recommend this Drilling EDM Machine for any precision mold application.

Ayse Demir, Manufacturing Engineer, Turkey
High Productivity For Micro-Hole Drilling

Our Turkish automotive parts company uses the Drilling EDM Machine to produce fuel injector nozzles with 0.2 mm holes. The machine increased our capacity by 45% and lowered scrap rate to 1.2%. The automatic electrode changer is reliable and easy to operate. Training from the supplier was thorough, and spare parts arrived quickly. This machine has become a key asset in our production line.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
High-Speed Micro-Hole Drilling With Advanced Pulse Control

High-Speed Micro-Hole Drilling With Advanced Pulse Control

Our Drilling EDM Machine features a high-frequency pulse power supply and intelligent servo control that deliver a maximum removal rate of 30 mm³/min and surface roughness as low as Ra 0.6 μm. In mold making, this means water lines and start holes can be drilled up to 60% faster than conventional EDM, while maintaining a taper below 0.03 mm. The system automatically adjusts pulse parameters based on material and electrode size, reducing operator workload and improving repeatability. For aerospace customers drilling 0.4 mm cooling holes in nickel alloys, the machine achieves a depth-to-diameter ratio of 200:1 with minimal recast layer. The advanced control also lowers electrode wear by up to 40%, cutting consumable costs significantly. Whether you produce injection molds, turbine blades, or medical instruments, this technology ensures consistent quality and high throughput, making the Drilling EDM Machine a profitable investment for precision manufacturers.
Rigid Machine Structure For Long-Term Accuracy And Stability

Rigid Machine Structure For Long-Term Accuracy And Stability

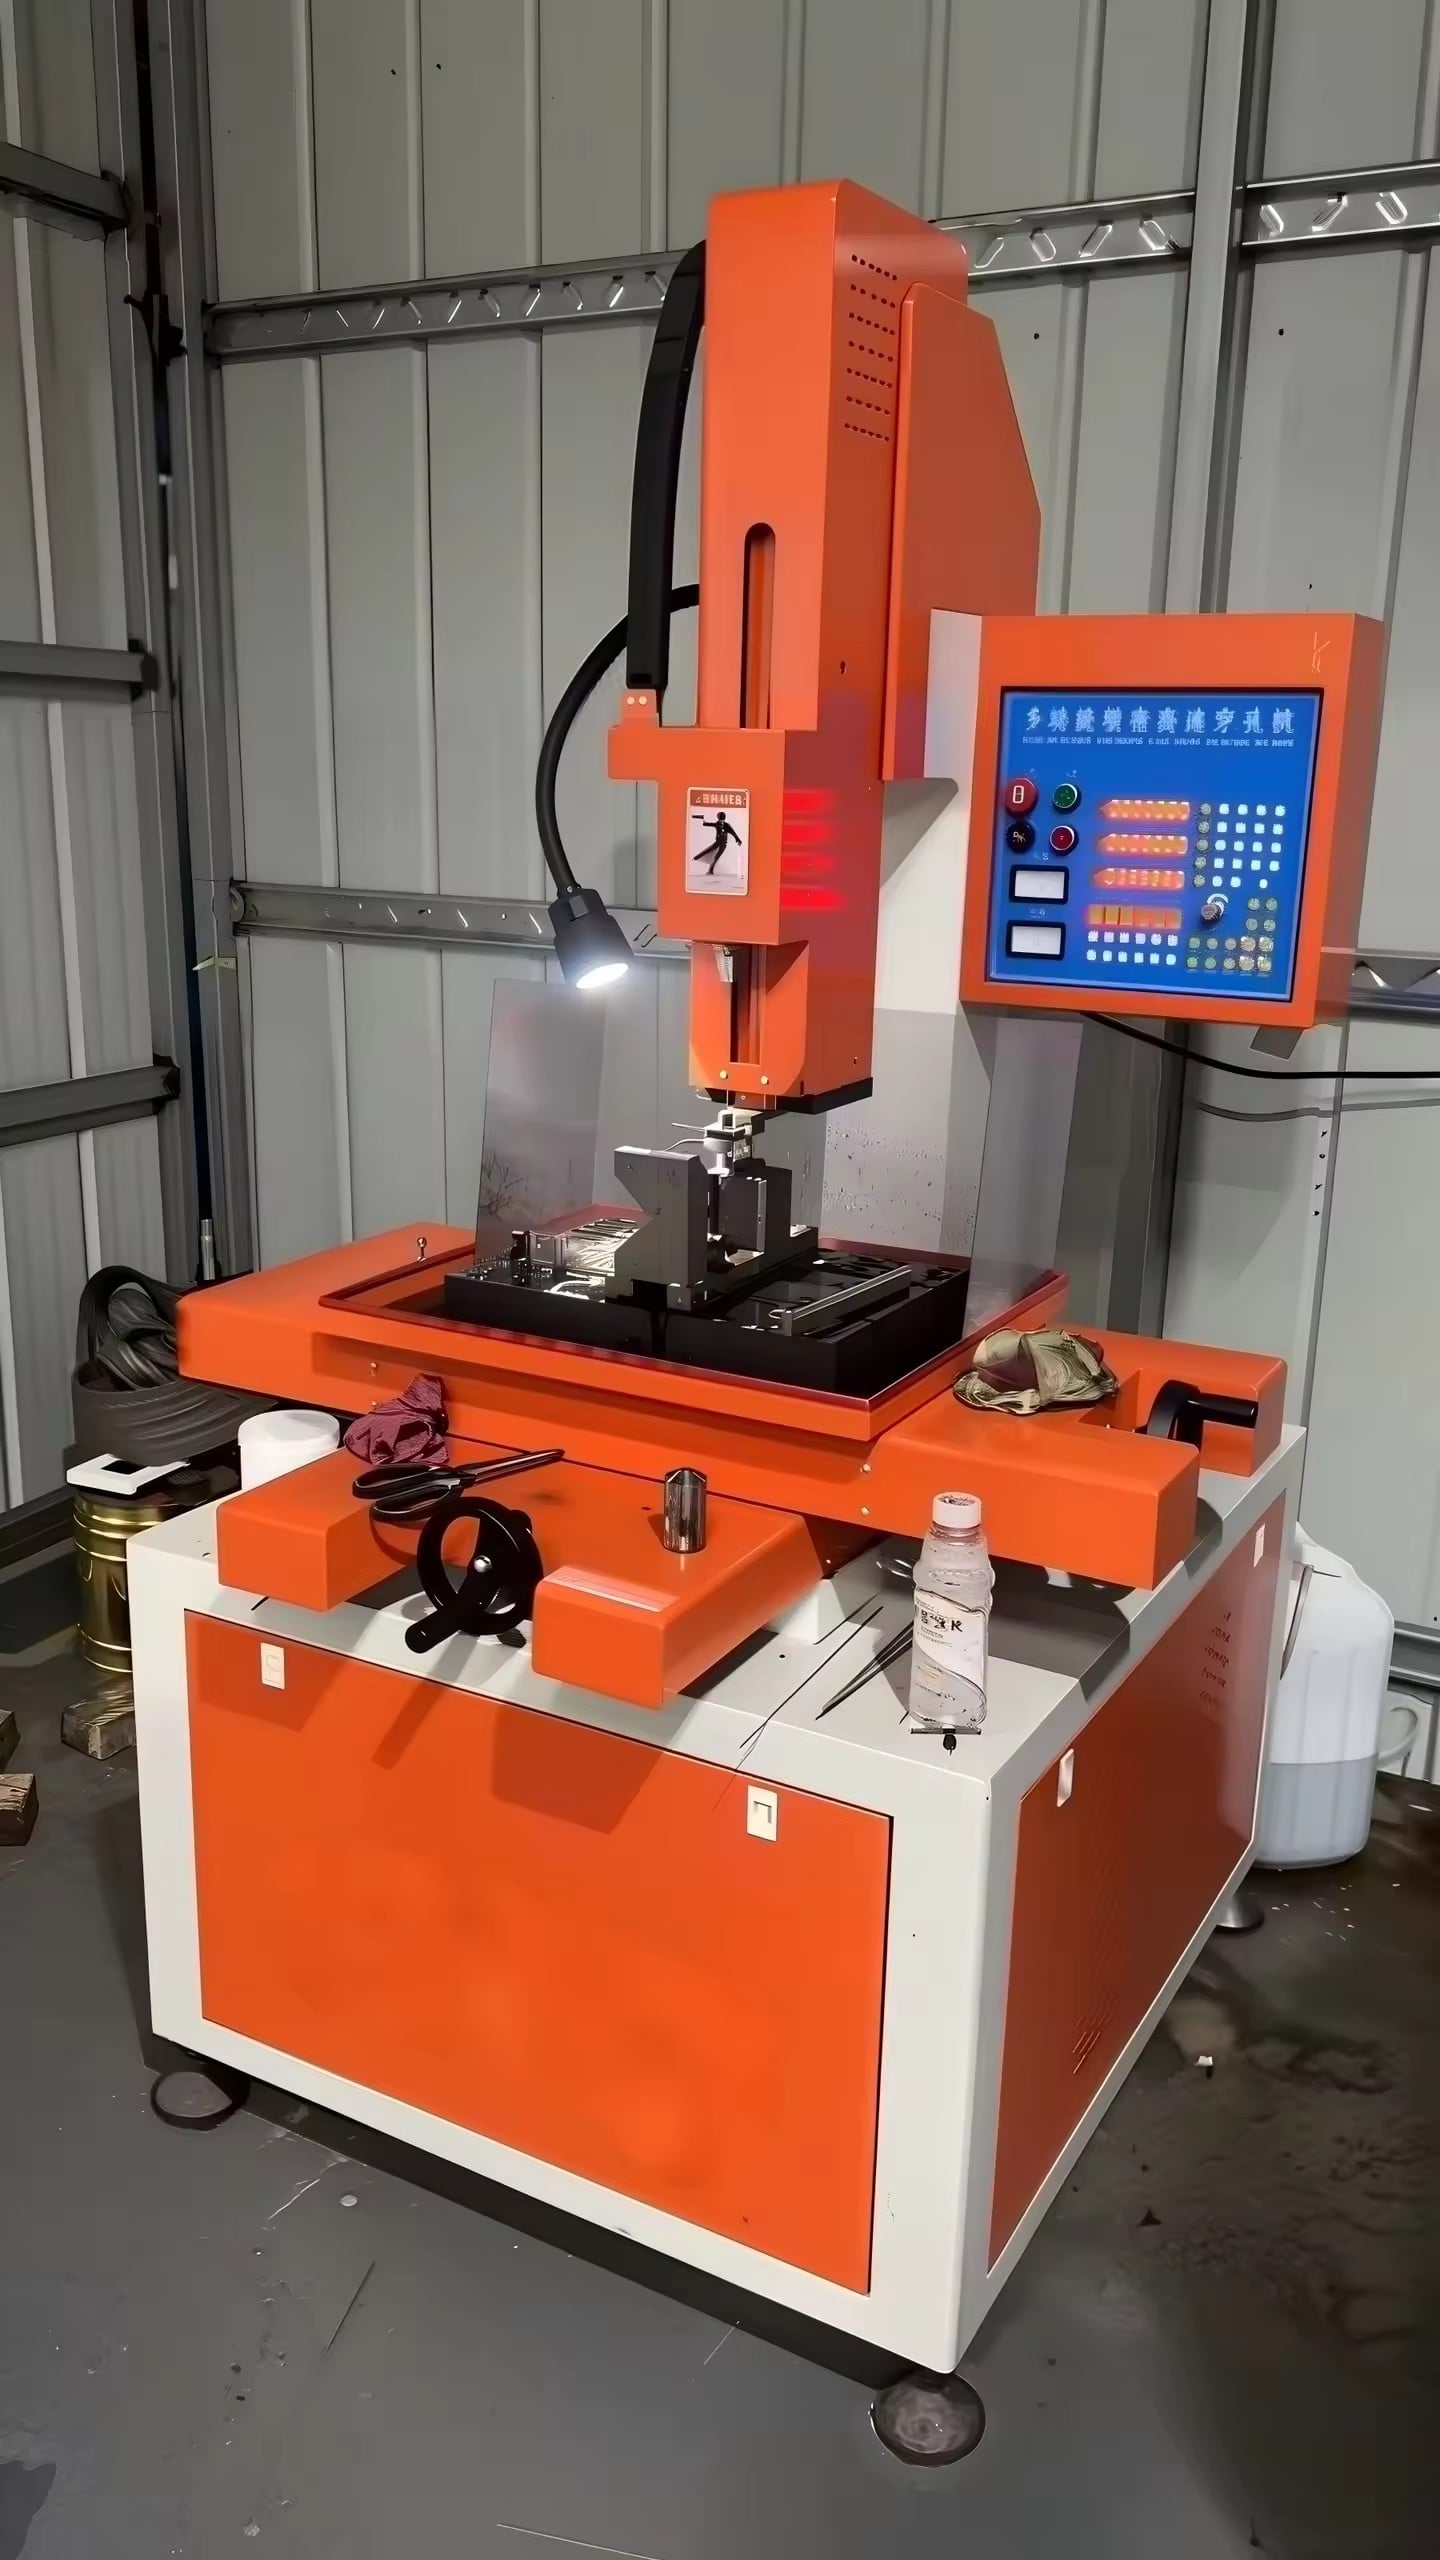
The Drilling EDM Machine is built on a stress-relieved cast iron base and a precision-machined column, providing excellent vibration damping and thermal stability. This rigid structure enables positioning accuracy of ±0.005 mm and repeatability of ±0.002 mm, even after years of heavy use. In a German mold shop, our machine has operated three shifts for 18 months with accuracy remaining within specification. The servo-driven Z-axis and precision linear guides ensure smooth movement and minimal wear. The dielectric system includes a high-pressure flushing unit and a temperature control device to maintain stable machining conditions. For deep-hole drilling, the rigid structure prevents electrode deflection and improves hole straightness. Customers in over 20 countries rely on this durability for continuous production. By investing in a robust Drilling EDM Machine, manufacturers reduce maintenance costs, extend machine life, and achieve consistent quality.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop