Desktop Wire EDM Machines | ±0.003 mm Accuracy & Ra 0.6 μm

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Precision Desktop Wire EDM Machines Engineered for Global Tool Rooms

Precision Desktop Wire EDM Machines Engineered for Global Tool Rooms

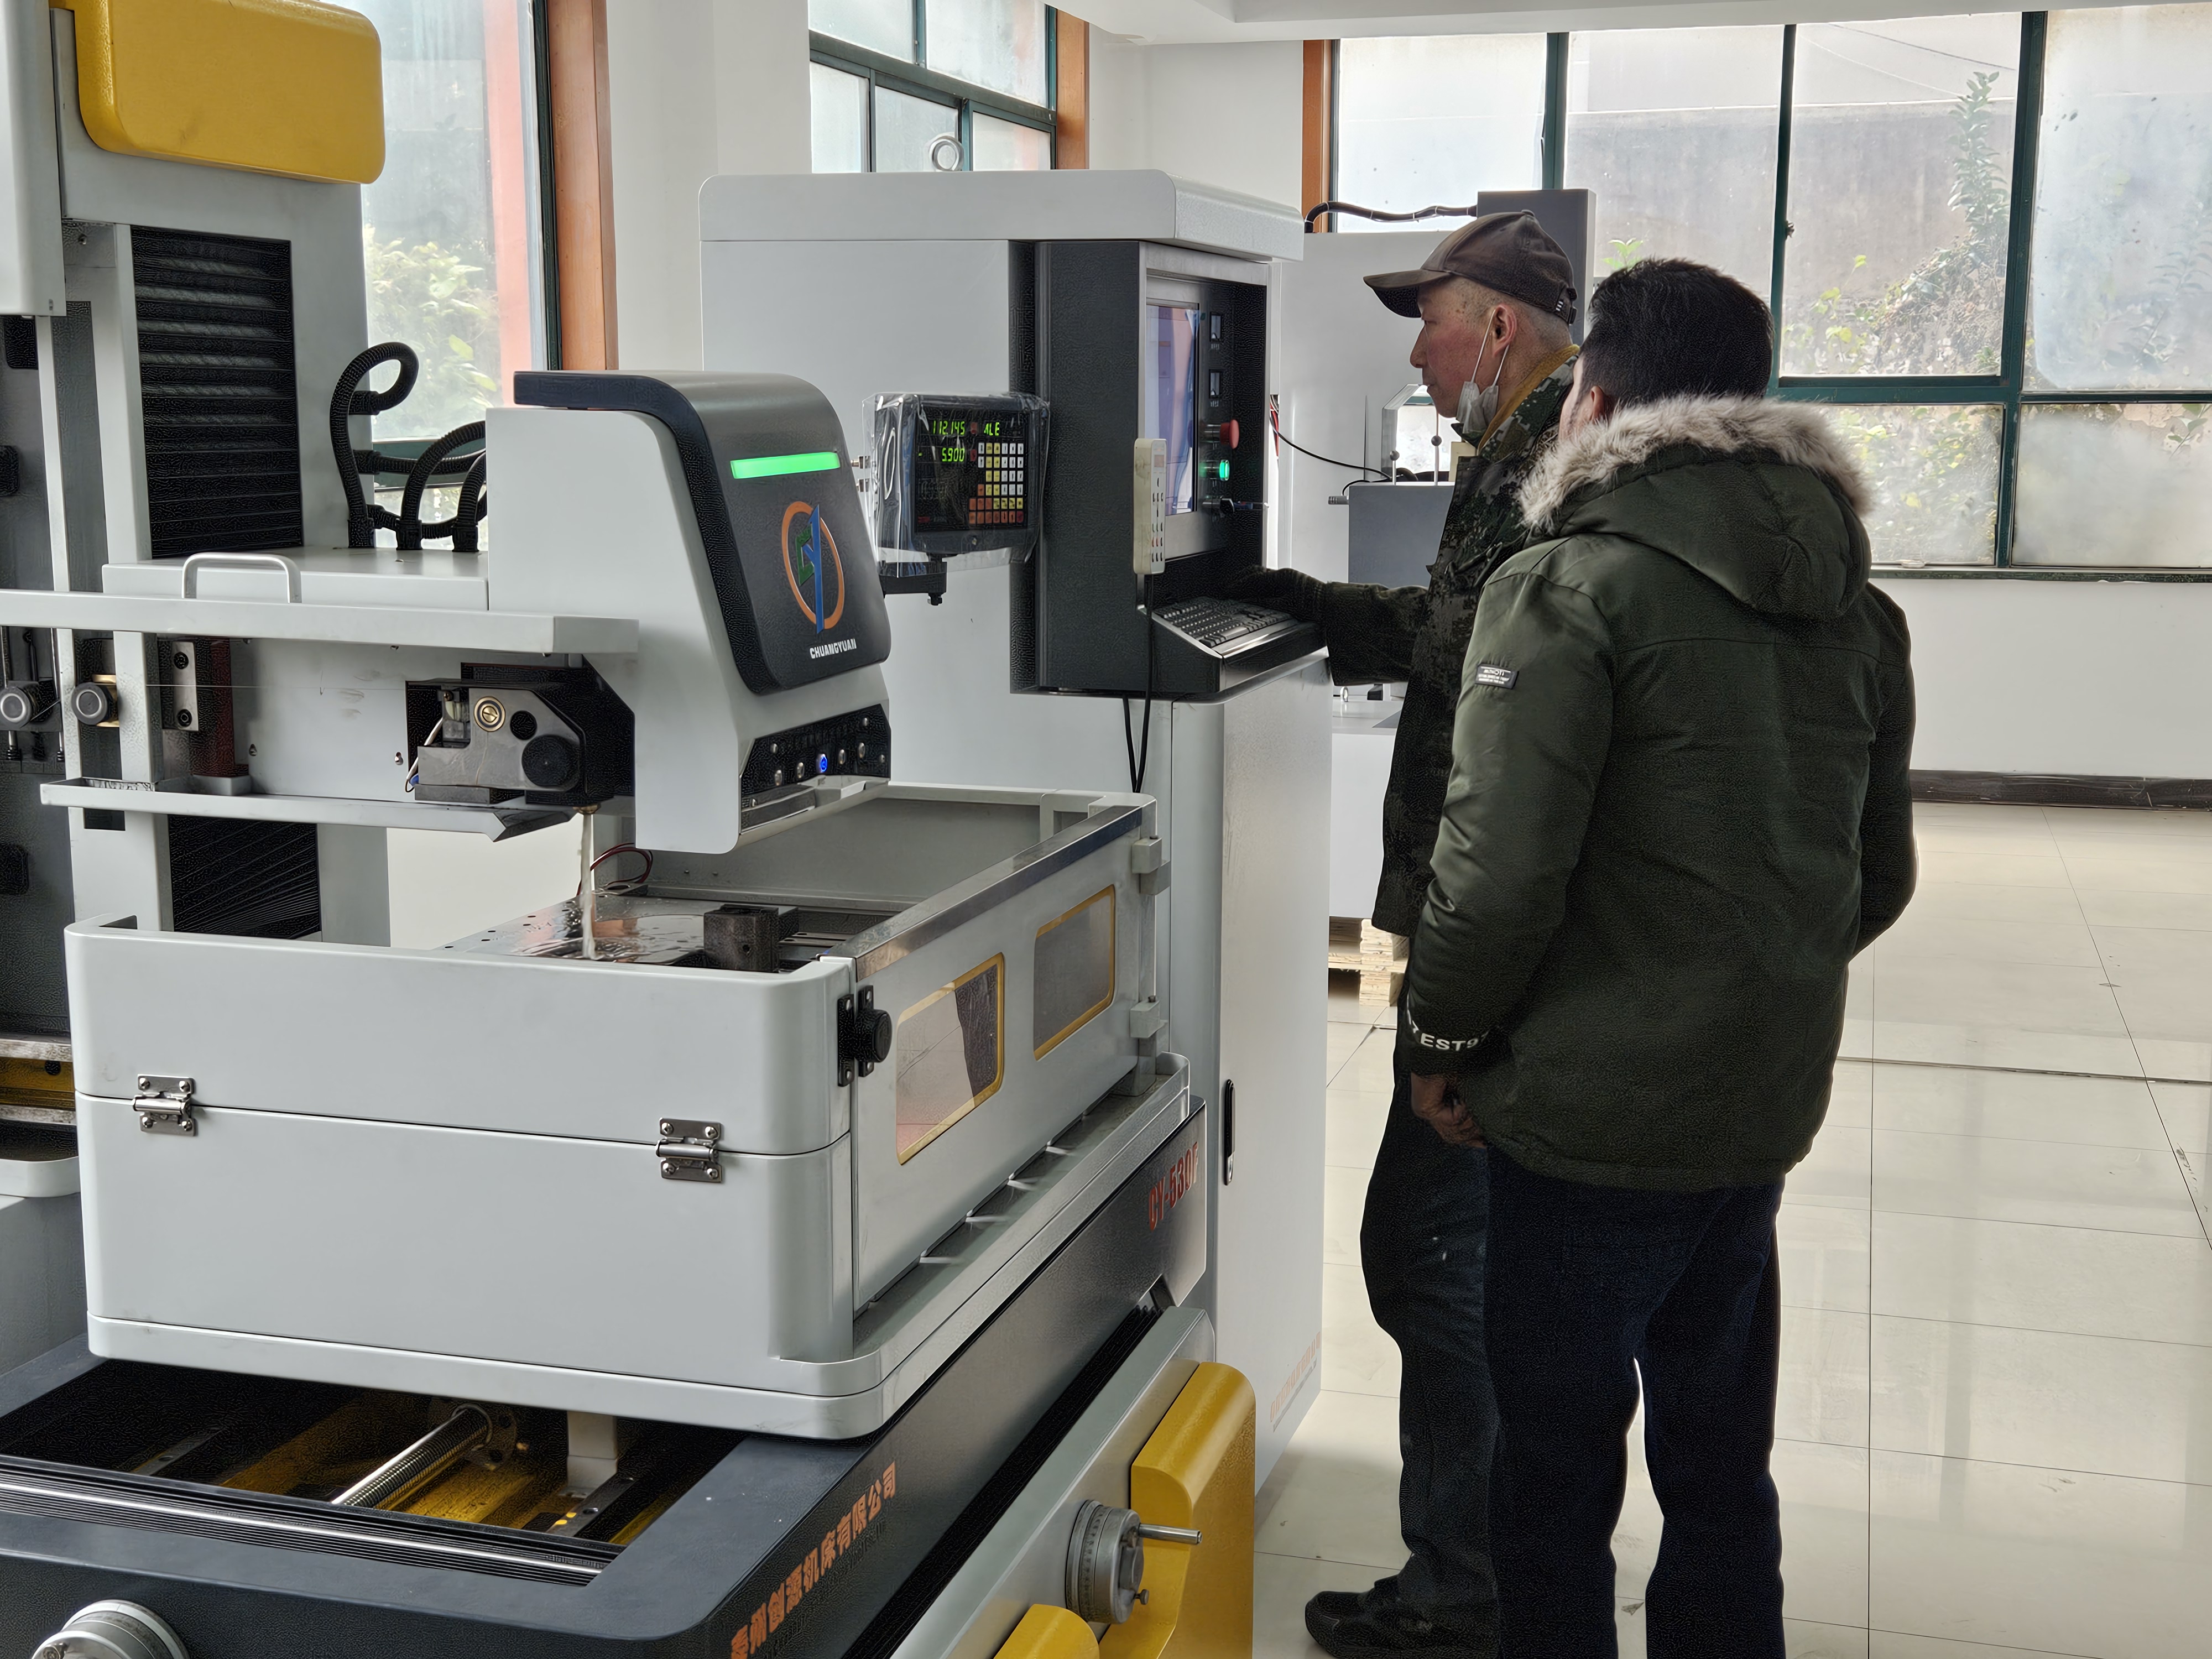
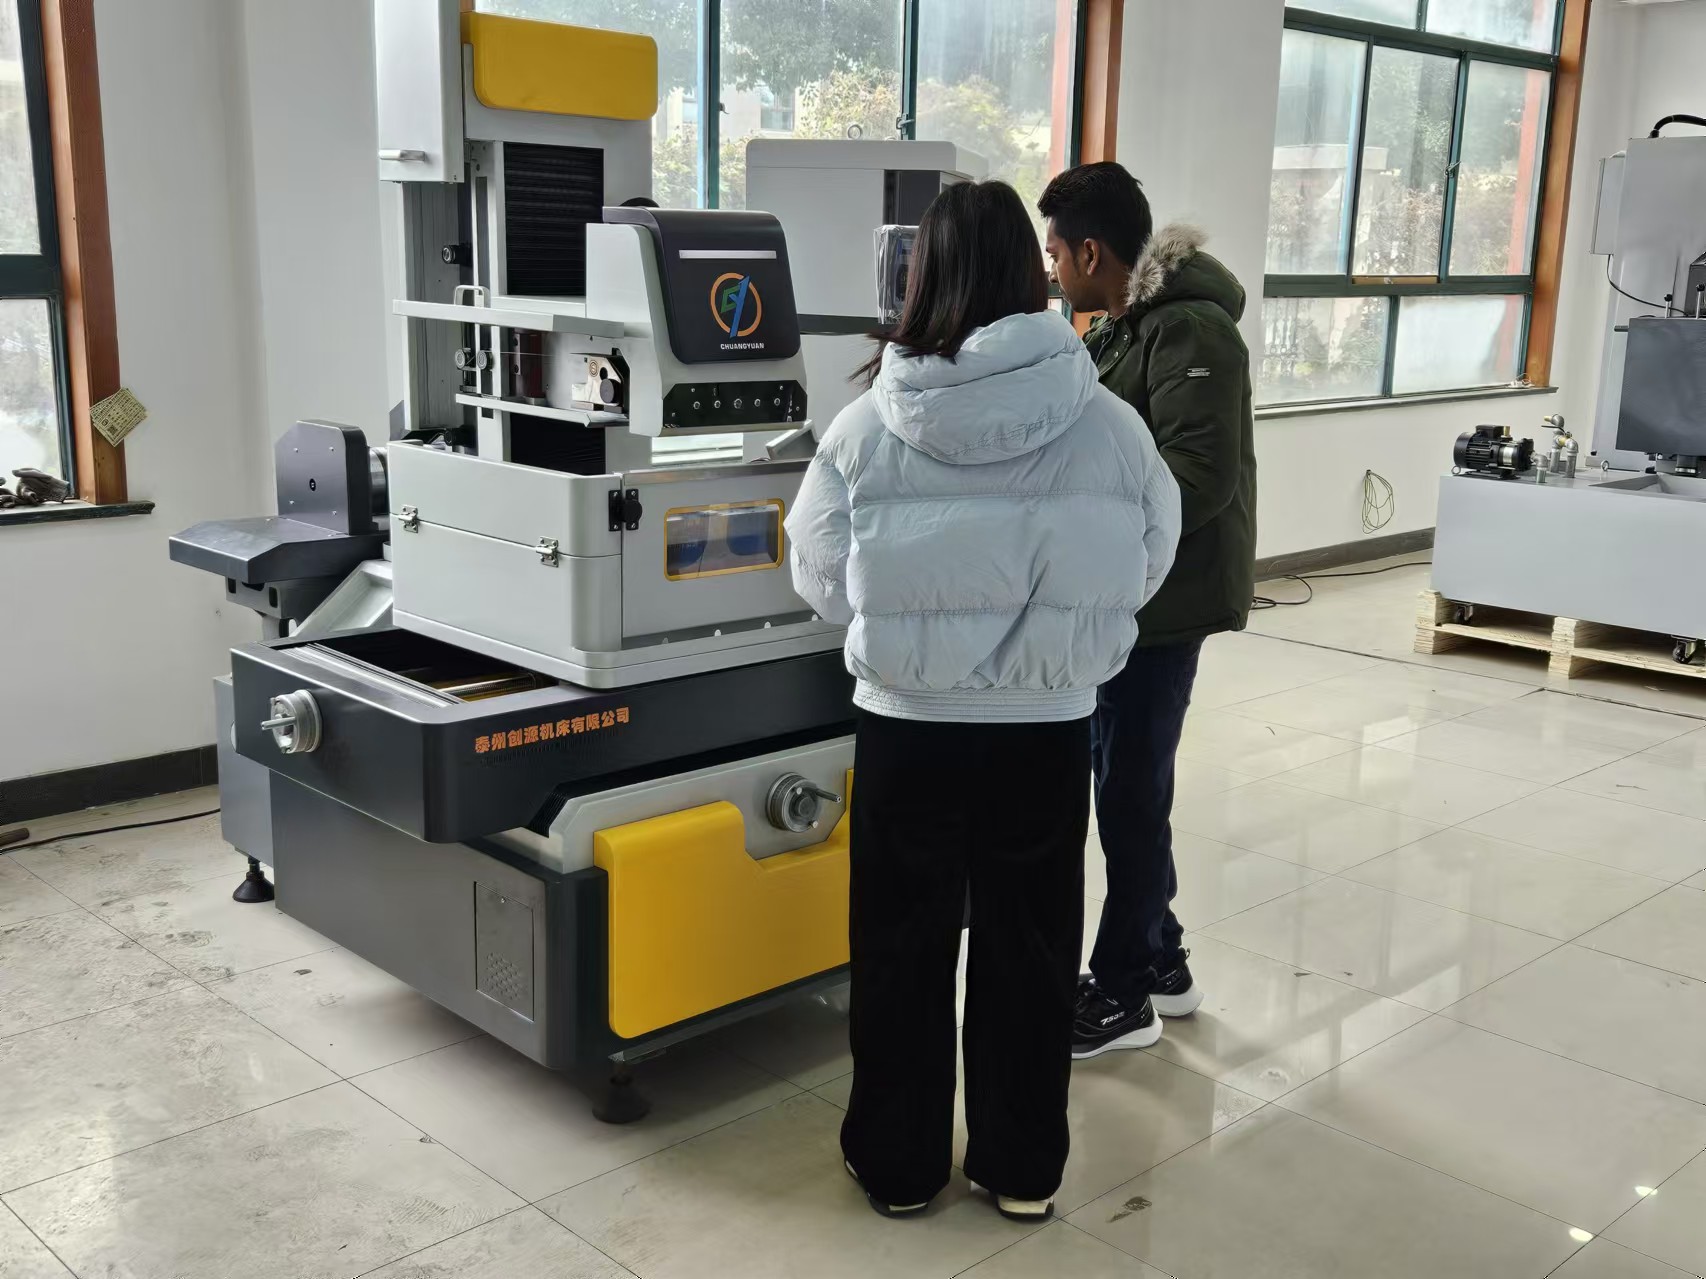
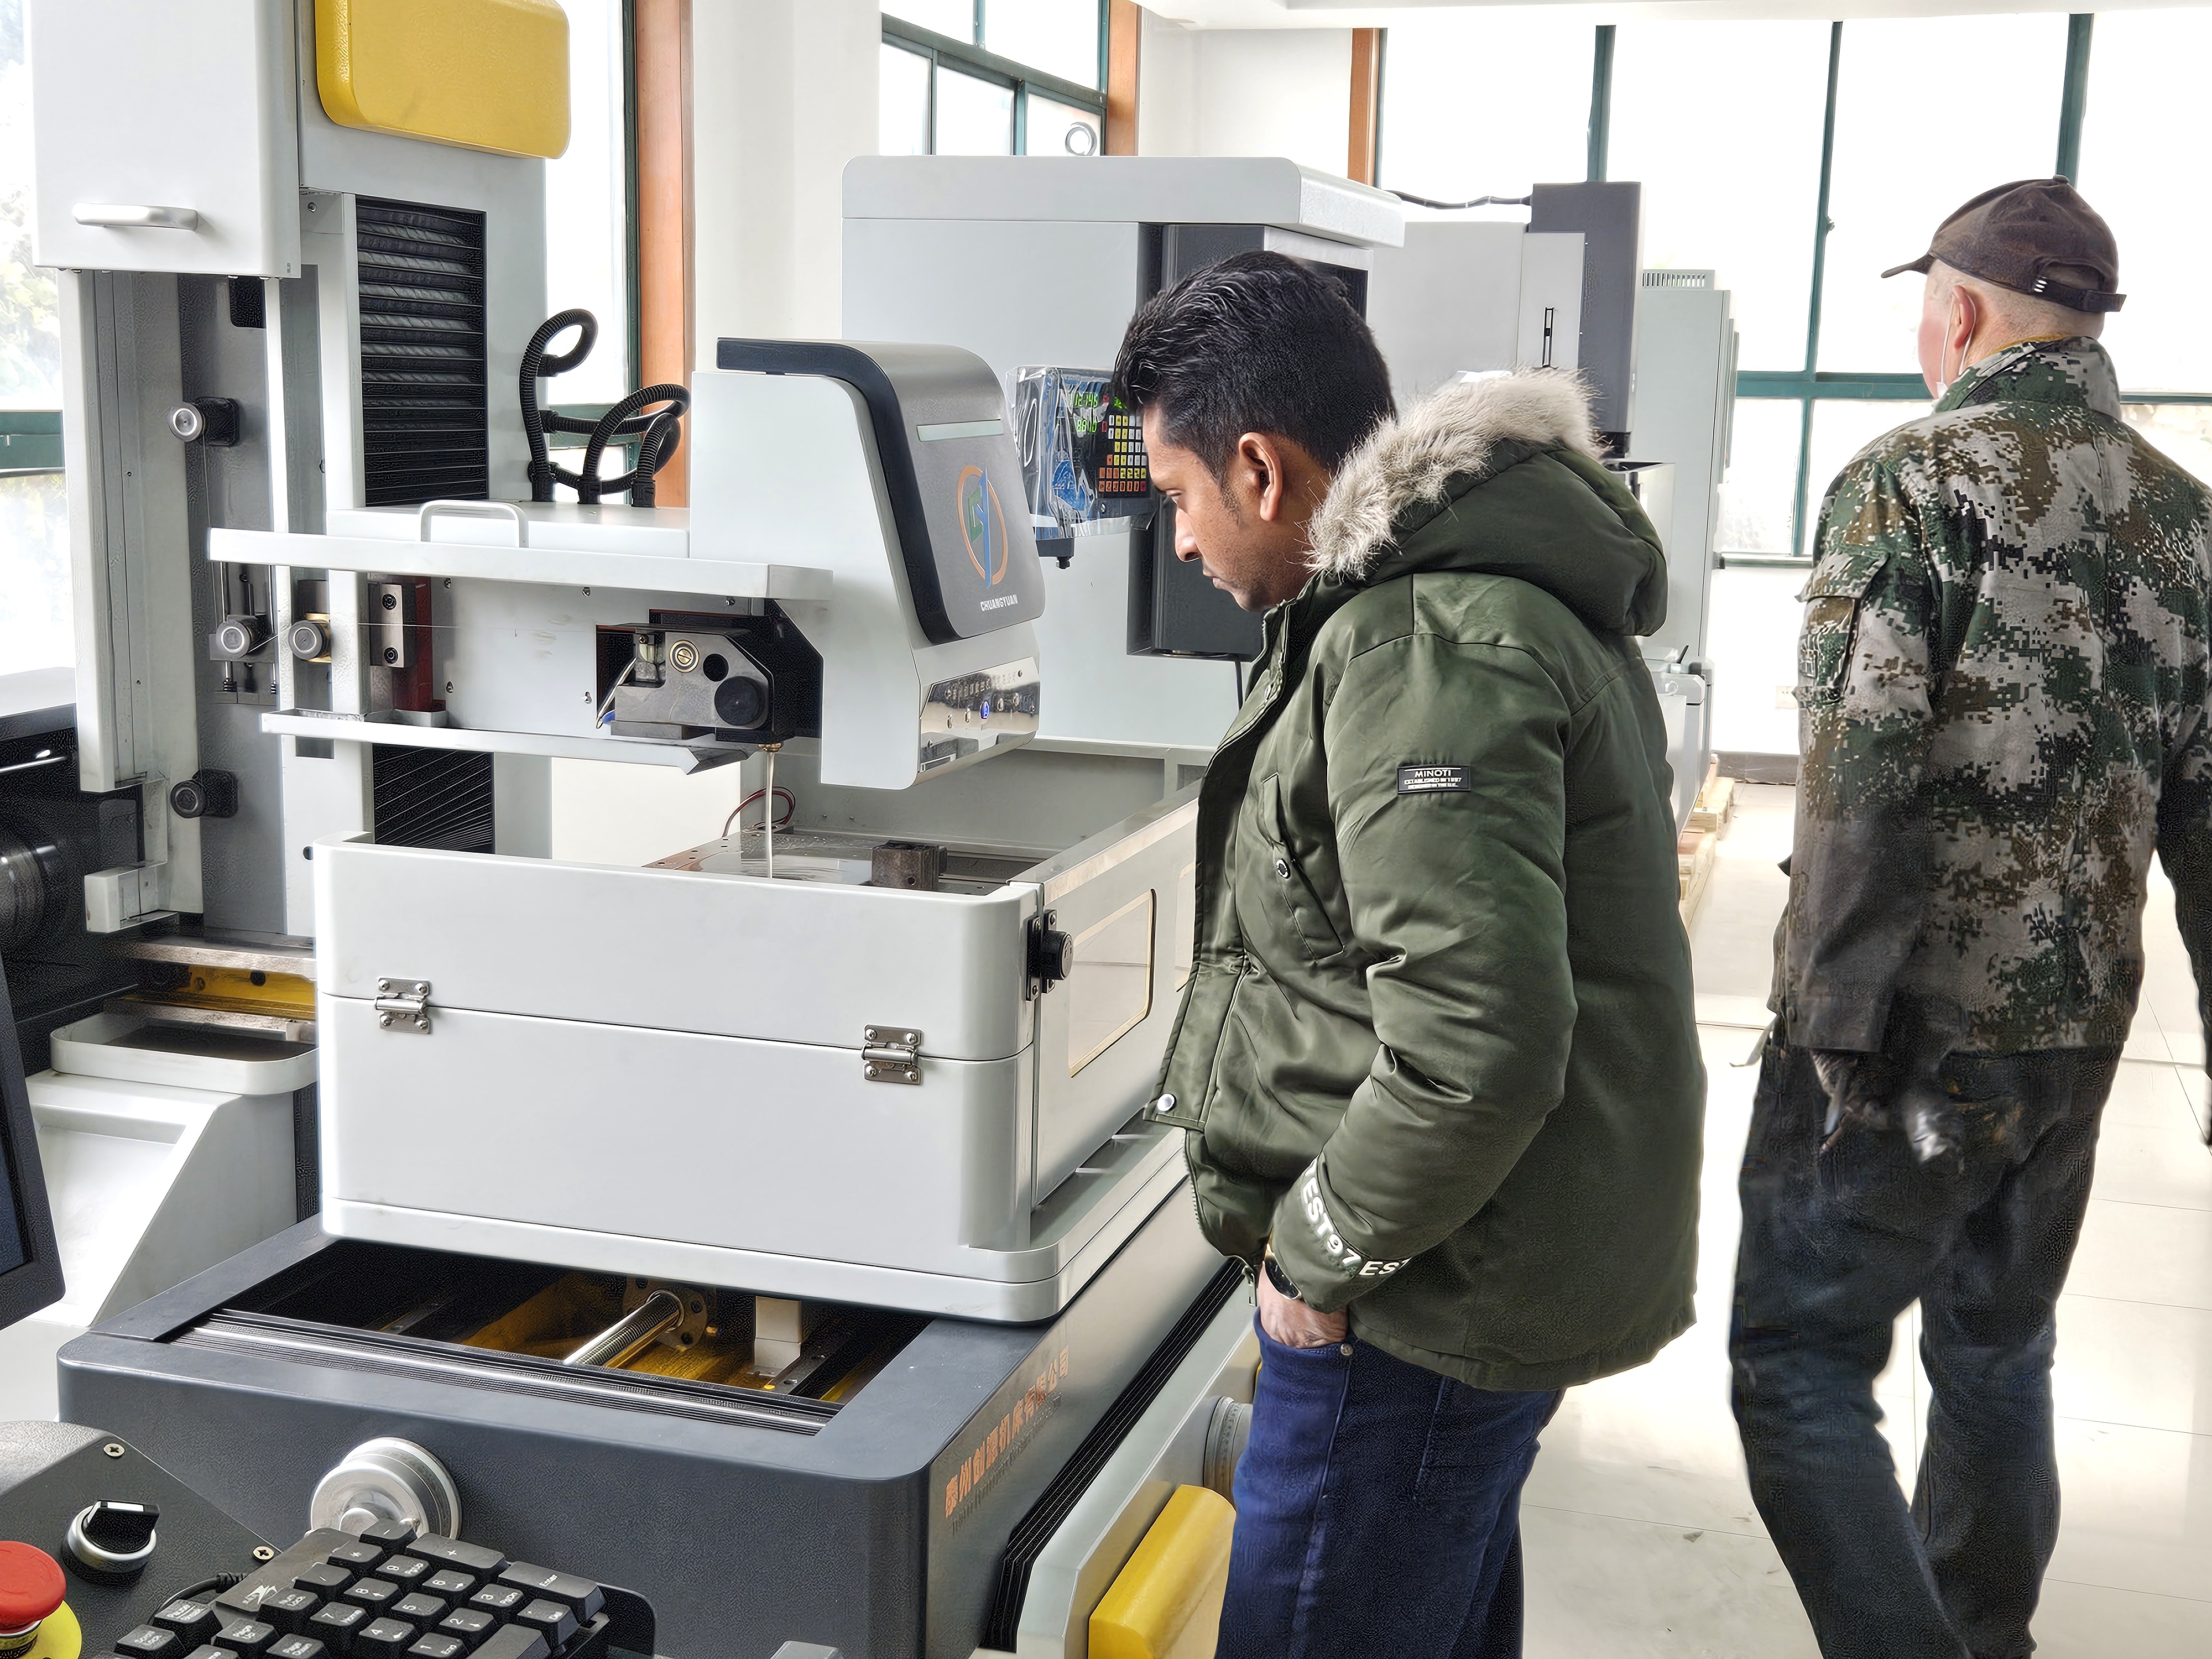
Taizhou Chuang Yuan Machine Tool Co., Ltd., established in 2003, builds Desktop Wire EDM systems that give mold shops, stamping die makers, and precision component manufacturers a compact, stable, and repeatable cutting platform. Our Desktop Wire EDM units deliver positioning accuracy of +/-0.003 mm and surface finishes down to Ra 0.6 um, cutting hardened tool steel from 45 to 62 HRC with typical material removal rates of 120 to 180 mm2 per minute. Because the generator, dielectric system, and linear guide structure are engineered as one integrated package, operators achieve first-cut accuracy without lengthy trial runs. In practical shop-floor use, a die repair team in Poland reduced electrode dressing time by 38 percent after switching two benchtop units into their brass-electrode workflow, while a connector mold maker in Mexico held slot tolerances of +/-0.005 mm across 2,400 consecutive cavities.
Get A Quote

Case Study

Cutting Stamping Die Inserts with +/-0.004 mm Repeatability in Germany

A German stamping die manufacturer needed to restore worn carbide inserts without losing punch-to-die clearance. Their previous manual method caused 0.02 mm variation and frequent rework. We supplied two Desktop Wire EDM machines configured with 0.25 mm brass wire and adaptive flushing. After 90 days, the team reported repeatability of +/-0.004 mm across 640 repaired inserts, scrap falling from 7 percent to 1.2 percent, and average repair cycle time dropping from 5.5 hours to 3.2 hours. The compact footprint allowed installation beside existing grinders, keeping the repair cell organized.

High-Volume Connector Mold Production in Mexico

A Mexican mold shop producing electrical connector molds required sharp internal corners and mirror-like side walls. Their existing equipment could not hold Ra 0.8 um on deep ribs. Our Desktop Wire EDM, equipped with multi-pass cutting technology, achieved Ra 0.6 um on 2,400 cavities with tolerance held at +/-0.005 mm. Production yield improved to 98.6 percent, and the customer expanded from one unit to three units within 14 months, using the machines for both new mold production and after-sales repair service.

Aerospace Fixture Component Repair in Turkey

A Turkish aerospace supplier needed to rework hardened fixture plates with complex profiles while maintaining traceability. Manual milling caused distortion and rejected parts. Using our Desktop Wire EDM with closed-loop cooling and precision wire tension control, they repaired 310 fixture plates with zero distortion and held profile accuracy within +/-0.006 mm. Inspection pass rate reached 99.4 percent, and the workshop reduced outsourced EDM spending by 42 percent in the first year.

Related products

Desktop Wire EDM has become a strategic asset for workshops that need high accuracy without occupying a large floor area. At Taizhou Chuang Yuan Machine Tool Co., Ltd., founded in 2003 in Taizhou City, Jiangsu Province, we integrate research, development, production, and sales under one roof, which allows strict control over the complete manufacturing chain. Each Desktop Wire EDM begins with finite element analysis of the machine bed, followed by high-temperature stress relief and precision grinding of the cast structure. The X, Y, and Z axes use preloaded linear guideways and C3-grade ball screws, then undergo laser interferometer calibration to verify positioning accuracy of +/-0.003 mm and repeatability of +/-0.002 mm.

During assembly, technicians align the wire transport system, tension servo, and dielectric nozzles, then validate flushing pressure at 0.8 to 1.2 MPa for reliable debris removal. The pulse generator is tuned to deliver stable discharge energy, enabling cutting of hardened steel from 45 to 62 HRC at 120 to 180 mm2 per minute while maintaining surface finishes from Ra 1.6 um in roughing to Ra 0.6 um in multi-pass finishing. Every unit runs a 72-hour continuous cutting test on representative workpieces before shipment, and inspection records are archived for traceability.

Globally, our Desktop Wire EDM machines serve mold makers, stamping die repair shops, medical instrument manufacturers, and aerospace fixture builders. In 20+ exporting countries, customers use them for insert repair, punch and die production, small-batch precision components, and prototype development. A workshop in Italy uses two units for micro-mold inserts and reports 30 percent shorter delivery times; a partner in South Korea applies them to hardened connector molds and maintains 99 percent first-pass inspection. The intuitive CNC supports ISO programming and conversational input, while remote diagnostics and multilingual documentation reduce downtime for international teams. Because spare parts are stocked regionally and training materials are structured for different skill levels, customers achieve stable production quickly and scale capacity as their market grows.

Frequently Asked Questions

What materials can a Desktop Wire EDM cut effectively?

Our Desktop Wire EDM machines cut hardened tool steel, carbide, copper, brass, aluminum, and specialty alloys. They perform reliably from 45 to 62 HRC, making them suitable for stamping dies, mold inserts, and precision fixtures. Typical removal rates reach 120 to 180 mm2 per minute, and multi-pass finishing achieves Ra 0.6 um.
The compact design fits workshops with limited space, typically occupying about 2.2 by 1.8 meters including the control cabinet and dielectric tank. This lets you install the machine beside grinders or milling centers without reorganizing the entire shop.
Positioning accuracy is +/-0.003 mm with repeatability of +/-0.002 mm. Surface finish ranges from Ra 1.6 um in roughing to Ra 0.6 um after multi-pass cutting, depending on material and wire diameter.
Yes. We provide English operation manuals, video training, and remote diagnostic support. Most operators reach production confidence within three days, and spare parts are stocked for 20+ exporting countries to minimize downtime.
Share your workpiece material, maximum thickness, tolerance, and surface finish targets. Our engineers recommend the correct generator configuration, wire diameter, and flushing setup, then confirm performance with a cutting test before shipment.

Related Articles

The correct handling method for insufficient machining accuracy of fast wire cutting machine

13

Dec

The correct handling method for insufficient machining accuracy of fast wire cutting machine

View More
What after sales service should reliable edm drilling machine suppliers provide

14

Jul

What after sales service should reliable edm drilling machine suppliers provide

The Evolution of Flexible Manufacturing Through Modular Architecture Modern industrial landscapes demand a high degree of adaptability, where the ability to transition production configurations quickly defines a facility’s operational rhythm....
View More
How to customize spring machine mold fixtures for special shaped spring production

03

Aug

How to customize spring machine mold fixtures for special shaped spring production

Mastering Complex Spring Production Challenges Navigating the intricacies of high-speed industrial manufacturing demands a profound understanding of wire feed dynamics, mechanical tolerances, and multi-axis bending mechanics across modern automated...
View More
How to reduce drill bit wear during continuous deep hole machine processing tasks

03

Aug

How to reduce drill bit wear during continuous deep hole machine processing tasks

Understanding the Mechanics of Deep Hole Thermal Stress Executing continuous boring and high-depth machining tasks on industrial production lines presents severe thermal and mechanical challenges that routinely test the limits of cutting tooling. W...
View More

Customer Testimonials

Klaus Berger, Tooling Manager, Germany
Repeatable Accuracy That Cut Our Rework in Half

We repair stamping dies daily, and the Desktop Wire EDM from Taizhou Chuang Yuan holds +/-0.004 mm across long shifts. Scrap dropped from 7 percent to 1.2 percent, and our repair cycle time fell by 40 percent. The remote support team responds quickly, which matters when production is running around the clock.

Carlos Mendoza, Production Director, Mexico
Compact Machine, Big Improvement in Mold Quality

We installed two Desktop Wire EDM units for connector molds and achieved Ra 0.6 um on deep ribs with +/-0.005 mm tolerance over 2,400 cavities. Yield reached 98.6 percent. The machines are easy to program, and our operators were productive within three days.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
High-Accuracy Motion System Validated by Laser Interferometer

High-Accuracy Motion System Validated by Laser Interferometer

Every Desktop Wire EDM uses preloaded linear guideways, C3-grade ball screws, and a stress-relieved cast bed that resists thermal drift during long cutting cycles. After assembly, each axis is calibrated with a laser interferometer to confirm positioning accuracy of +/-0.003 mm and repeatability of +/-0.002 mm. For mold makers cutting deep ribs or stamping die repair teams restoring punch-to-die clearance, this means fewer trial cuts and predictable first-part accuracy. A German customer held +/-0.004 mm across 640 repaired inserts, reducing scrap from 7 percent to 1.2 percent. The rigid structure also supports cutting hardened steel from 45 to 62 HRC without vibration marks, so surface quality remains consistent from the first cut to the last part of the shift. This level of mechanical stability is the foundation of reliable Desktop Wire EDM performance in demanding tool rooms.
Intelligent Pulse Generator for Fast, Consistent Cutting

Intelligent Pulse Generator for Fast, Consistent Cutting

The adaptive pulse generator in our Desktop Wire EDM continuously monitors discharge conditions and adjusts energy output to maintain stable cutting. Material removal rates reach 120 to 180 mm2 per minute, while multi-pass finishing delivers surface finishes down to Ra 0.6 um. This balance helps workshops increase throughput without sacrificing accuracy. A Turkish aerospace supplier used this technology to repair 310 hardened fixture plates with zero distortion and profile accuracy within +/-0.006 mm, achieving a 99.4 percent inspection pass rate. The generator also supports ISO code and conversational programming, allowing operators of different skill levels to run production confidently. For job shops handling mixed orders, the ability to switch between roughing and finishing strategies quickly keeps lead times short and machine utilization high.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop