Large EDM Machine for Heavy-Duty Precision | 300A, 12T Capacity

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Large EDM Machine Built for Heavy-Duty Precision Manufacturing

Large EDM Machine Built for Heavy-Duty Precision Manufacturing

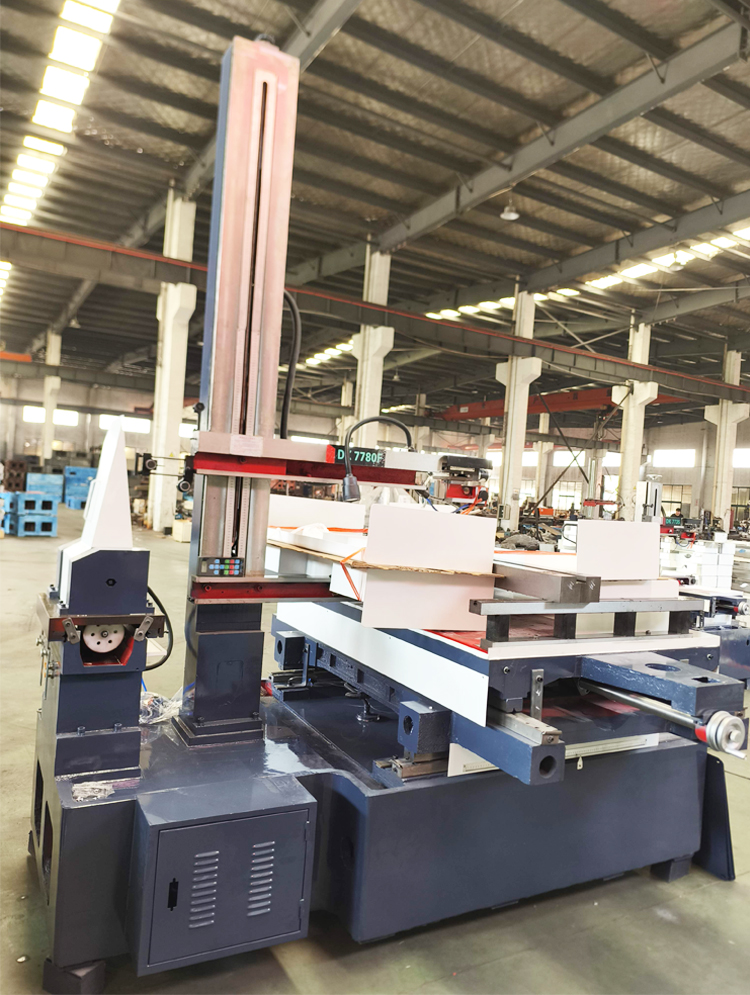
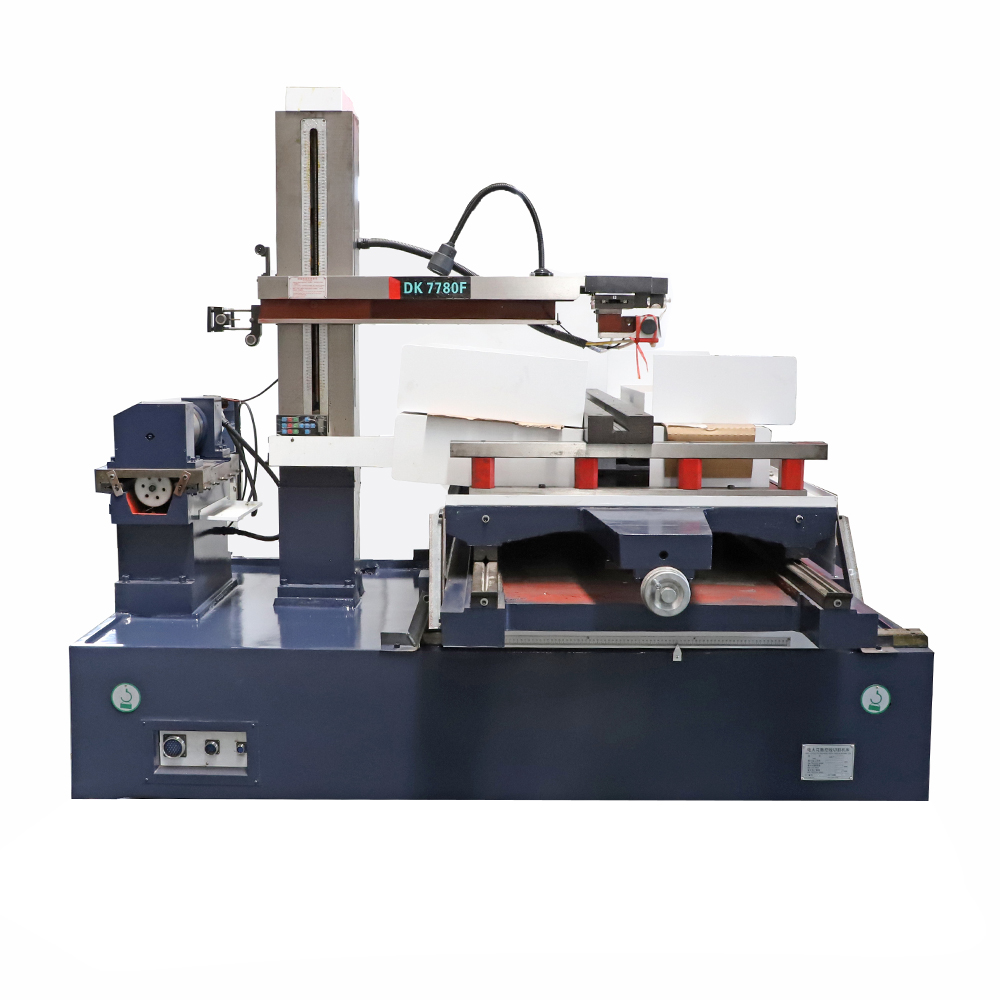
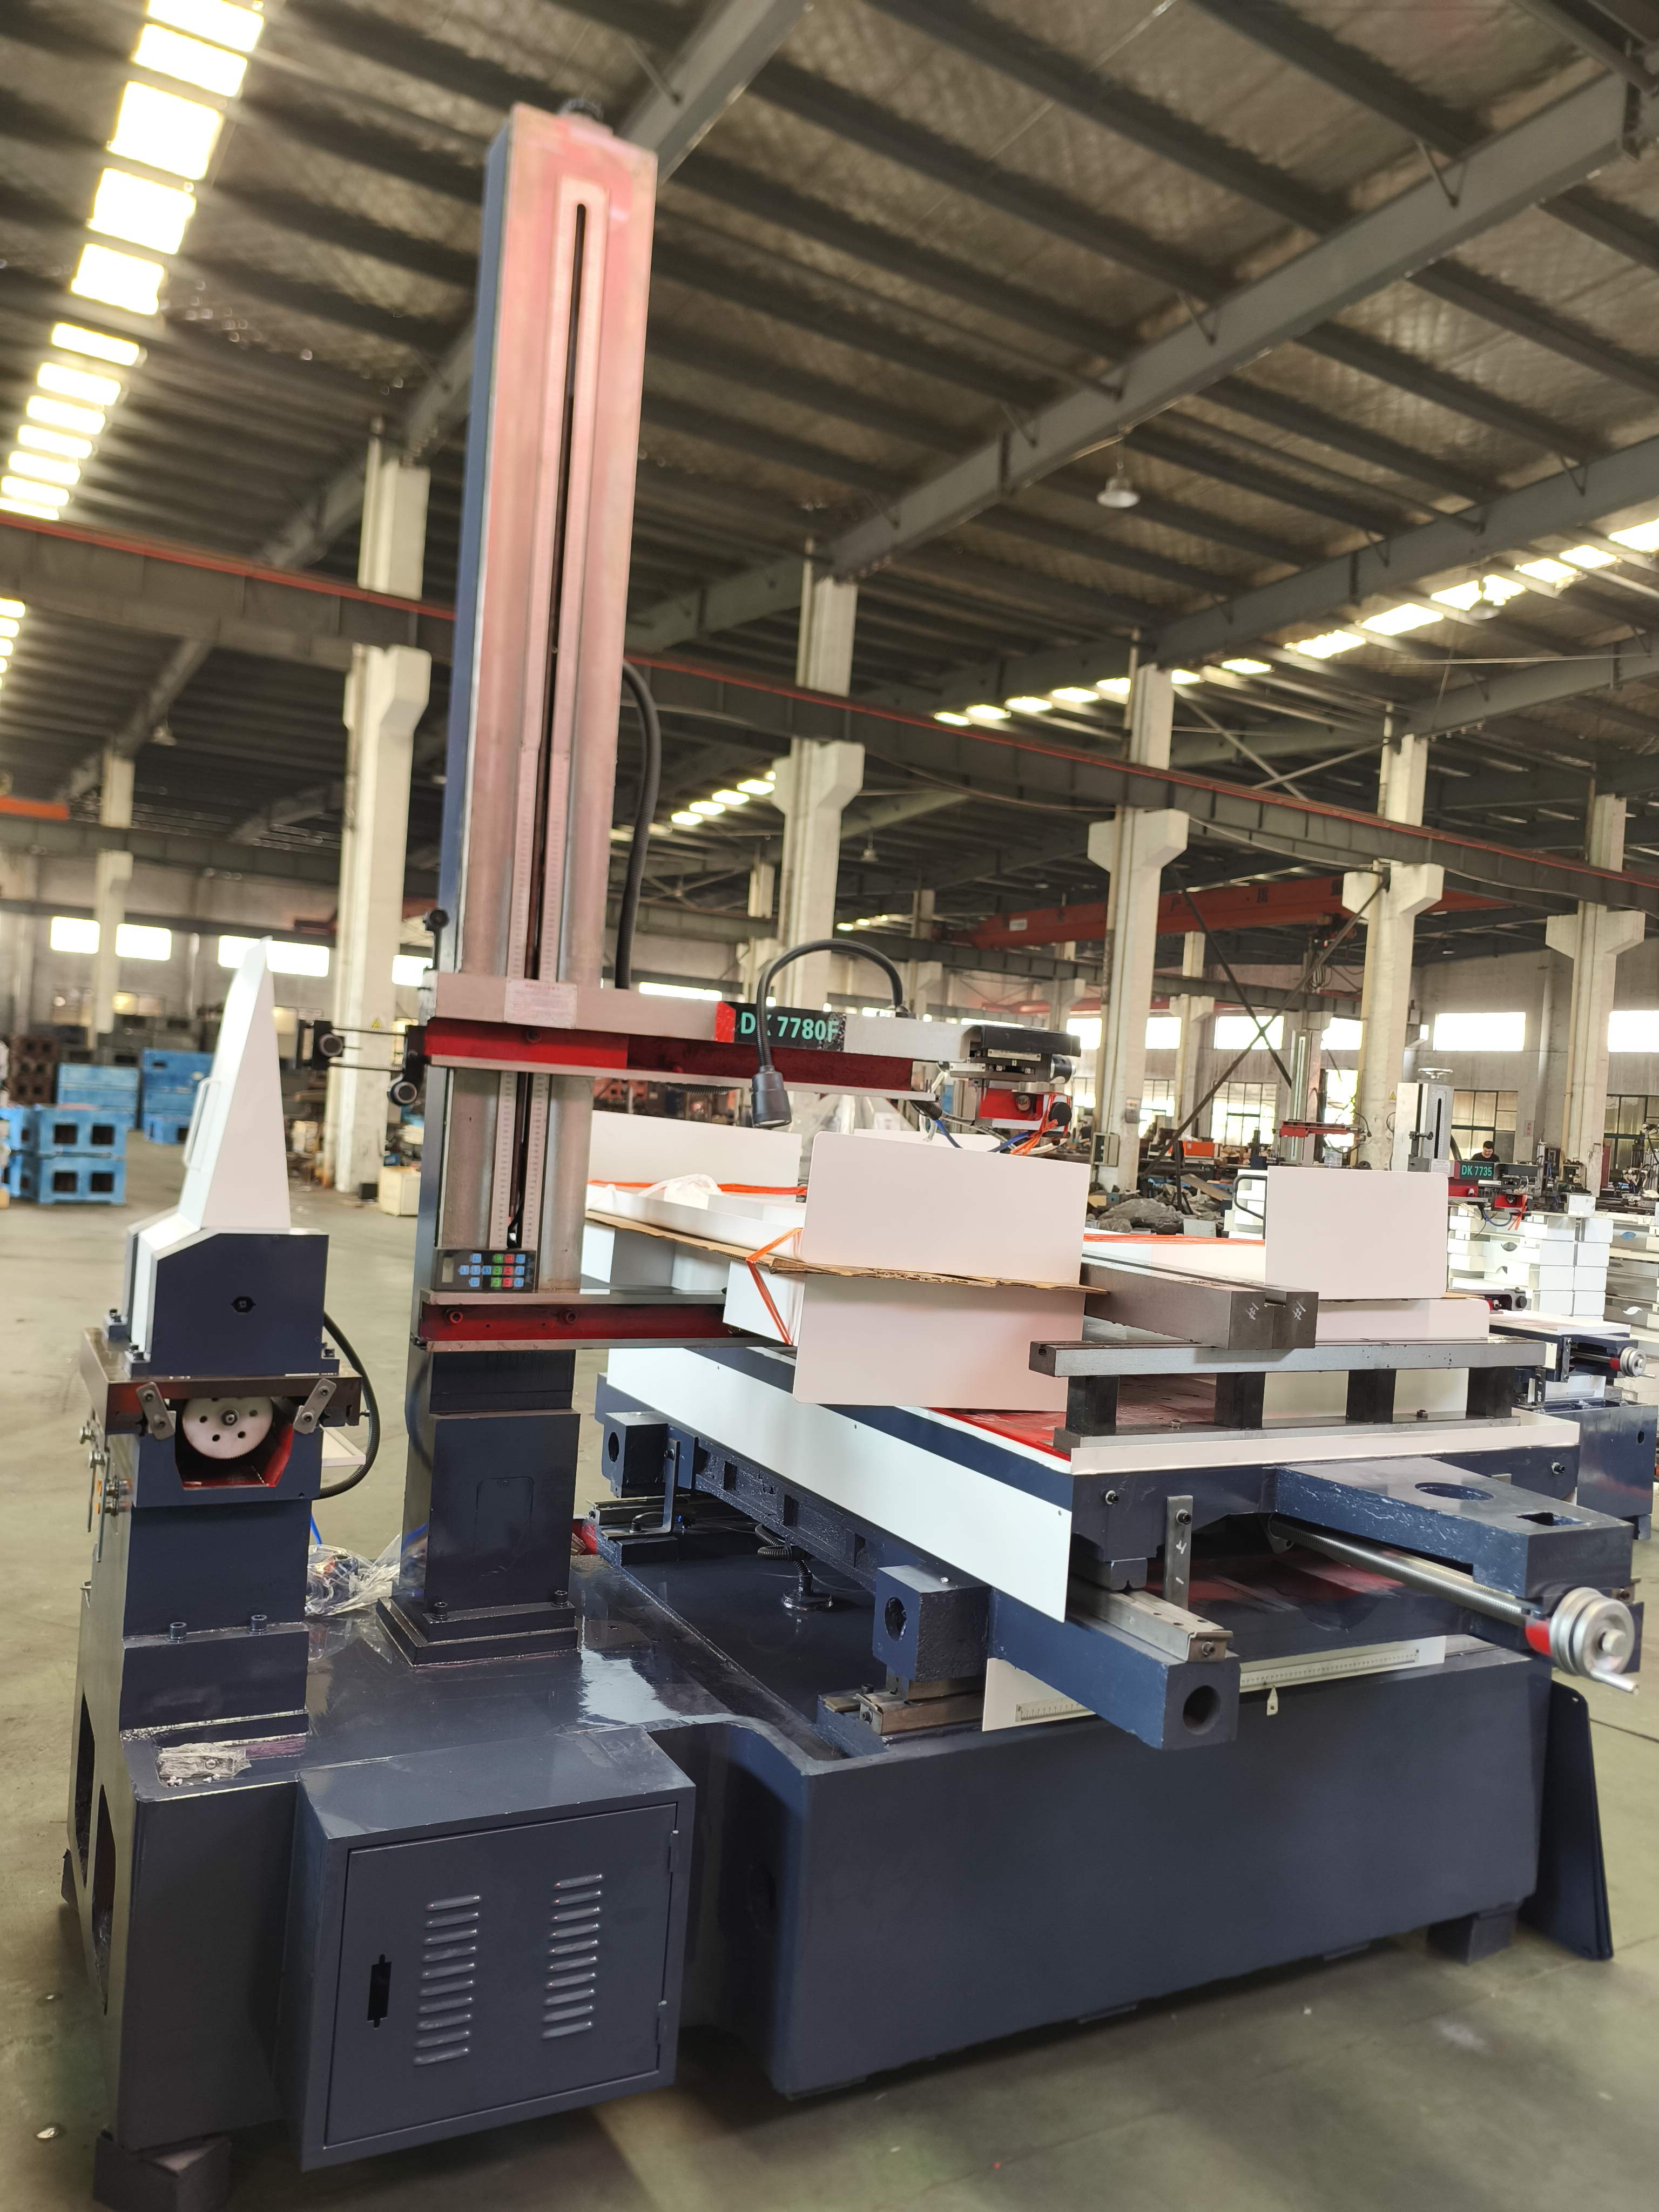
Taizhou Chuang Yuan Machine Tool Co., Ltd., established in 2003 in Taizhou City, Jiangsu Province, China, is a professional manufacturer integrating research and development, production, and sales of precision machine tools. Our Large EDM Machine is engineered for die and mold shops, aerospace component suppliers, and heavy equipment manufacturers that require deep cavity burning, large workpiece capacity, and long unattended runs. With worktable sizes from 1200 x 800 mm to 3000 x 1600 mm, maximum workpiece weights up to 12,000 kg, and Z-axis travel up to 800 mm, these machines handle oversized forging dies, stamping molds, and turbine housings that smaller units cannot accommodate. A 300 A high-current generator delivers a material removal rate of up to 1,200 mm3/min on 1.2738 tool steel, reducing roughing time by roughly 35 percent compared with conventional 100 A systems.
Get A Quote

Case Study

Large EDM Machine Cuts Forging Die Lead Time for a German Mold Shop

A German forging die manufacturer struggled with a 3,800 kg hammer die that exceeded the capacity of its existing 800 mm table EDM units. After installing a Chuang Yuan Large EDM Machine with a 2500 x 1250 mm table and 400 A generator, the shop machined the entire die cavity in one setup. Roughing time dropped from 76 hours to 48 hours, a 37 percent reduction, and electrode consumption fell by 22 percent. The shop now quotes 12 day turnarounds instead of 20 days, winning two additional automotive forging contracts within six months.

Large EDM Machine Solves Deep-Rib Burn for an Aerospace Tooling Supplier

An aerospace tooling supplier in Turkey needed to burn 240 mm deep ribs into a titanium alloy fixture with a surface finish below Ra 0.8 micrometres. Standard EDM machines drifted beyond tolerance at that depth. Using a Chuang Yuan Large EDM Machine equipped with linear glass scales and adaptive flushing, the supplier held straightness within 0.01 mm over the full depth. Scrap rate on the fixture line fell from 8 percent to 1.5 percent, saving an estimated 45,000 USD annually.

Large EDM Machine Supports 24 Hour Mold Production in Southeast Asia

A Malaysian plastic injection mold maker ran two shifts but lost nights to manual electrode changes. A Large EDM Machine with a 24 station automatic tool changer and remote monitoring enabled unattended overnight burning. Output rose from 18 to 29 mold inserts per month, on-time delivery improved from 82 percent to 96 percent, and the payback period was under 14 months. Products Title: Discover Our Large EDM Machine Series for Oversized Precision Work

Related products

Manufacturing a Large EDM Machine begins long before assembly. At Taizhou Chuang Yuan Machine Tool Co., Ltd., production starts with finite element analysis of the machine bed, followed by stress-relieved castings that are aged for six months to stabilise geometry. The bed and column are then precision-ground on five-face machining centres, with flatness verified to 0.01 mm per metre. Guideways are hand-scraped and laser-interferometer calibrated, ensuring each axis repeats within plus or minus 0.003 mm. The dielectric system is pressure-tested at 8 bar to confirm leak-free circulation for deep-cavity flushing, a critical requirement when burning ribs deeper than 200 mm. Generator cabinets undergo a 72 hour burn-in at full load, and every finished Large EDM Machine is test-cut on a certified sample before shipment. Quality control follows ISO 9001 procedures, and each unit ships with a calibration report traceable to national standards.

Globally, these machines serve die and mold shops in Germany, automotive tool rooms in Mexico, aerospace suppliers in Turkey, and heavy machinery plants across Southeast Asia. In one documented case, a Large EDM Machine with a 3000 x 1600 mm table machined a 9.5 tonne press die in a single setup, eliminating two repositioning operations and cutting total machining time by 31 percent. Another customer in India reduced electrode wear from 0.4 percent to 0.18 percent by using the machine's adaptive pulse control on copper-tungsten electrodes. In the Middle East, a customer running 45 degree ambient temperatures relied on the integrated chiller and thermal compensation to keep dimensional drift under 0.006 mm during a 16 hour unattended cycle. Our engineering team supports clients through remote diagnostics, on-site commissioning, and operator training, and we have exported to more than 20 countries and regions. Spare parts are stocked for fast dispatch, and typical response time for technical support is under 24 hours. Whether the application is a forging die, an injection mold, or a turbine component, the Large EDM Machine is configured with the generator, flushing, and automation package that matches the job, not a one-size-fits-all specification. This approach keeps cycle times competitive and total cost of ownership predictable.

Frequently Asked Questions

What workpiece size can a Large EDM Machine handle?

Our Large EDM Machine range covers worktables from 1200 x 800 mm up to 3000 x 1600 mm, with maximum workpiece weights from 3,000 kg to 12,000 kg. Z-axis travel reaches 800 mm, allowing deep cavity burning on forging dies, large injection molds, and heavy fixtures. If you share your typical part dimensions and weight, we will recommend the correct table size and generator configuration.
With a 300 A generator, material removal rate reaches up to 1,200 mm3/min on common tool steels such as 1.2738. That is roughly 35 percent faster than a 100 A system on the same job. Actual speed depends on electrode material, flushing conditions, and depth of cut.
Yes. With the optional 24 station automatic tool changer and remote monitoring, the machine can run lights-out. Customers report reducing electrode changeover from 90 minutes to 12 minutes per shift and increasing monthly output significantly.
Linear glass scales, thermal compensation, and a temperature-controlled dielectric system keep positioning within plus or minus 0.005 mm over a 20 hour run. Each machine is laser-calibrated before shipment and delivered with a traceable accuracy report.

Related Articles

How to choose a machining center?

12

Dec

How to choose a machining center?

View More
Why multi functional edm machine meets mixed mold and part production factory demands

14

Aug

Why multi functional edm machine meets mixed mold and part production factory demands

Navigating the Complexities of High-Mix Manufacturing Environments Running a modern industrial production plant often feels like juggling a dozen spinning plates at once, especially when dealing with high-mix, low-volume manufacturing schedules. Pl...
View More
What output benefits enterprises gain by updating old edm spark erosion machine equipment

03

Aug

What output benefits enterprises gain by updating old edm spark erosion machine equipment

Identifying Legacy Constraints in Spark Erosion Production Operating mature, decades-old equipment on high-precision manufacturing shop floors often creates hidden operational penalties that quietly erode profit margins over time. When production f...
View More
What export quality standards international clients require for wire cutting machine products

03

Aug

What export quality standards international clients require for wire cutting machine products

Understanding International Export Compliance in Precision Machining Navigating the complex landscape of global industrial trade requires a thorough understanding of the stringent technical benchmarks that overseas buyers mandate for advanced metal...
View More

Customer Testimonials

Klaus Berger
Cut Our Deep-Cavity Burn Time by More Than a Third

We purchased a Large EDM Machine for forging die work, and the difference was immediate. Our roughing time on a 3.2 tonne die dropped from 68 hours to 43 hours, and surface finish improved enough to reduce manual polishing by 20 percent. The thermal stability is excellent even in summer. Support has been responsive and professional.

Ayse Demir
Reliable Accuracy on Titanium Aerospace Fixtures

Our aerospace fixtures require tight tolerances at depth, and this Large EDM Machine holds them. Scrap dropped from 8 percent to under 2 percent, and we now run overnight without an operator. The automatic tool changer alone saves us about 40 hours per month.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Massive Worktable Capacity for Oversized Dies and Molds

Massive Worktable Capacity for Oversized Dies and Molds

The defining strength of our Large EDM Machine is its ability to accept workpieces that most EDM units simply cannot hold. Table sizes range from 1200 x 800 mm to 3000 x 1600 mm, with load capacities up to 12,000 kg. This means a complete forging die, a full injection mold base, or a large progressive stamping die can be set up once and machined without repositioning. In practice, eliminating one repositioning on a 9.5 tonne press die cut total machining time by 31 percent for a European customer. Deep Z-axis travel of up to 800 mm supports cavity depths that would require multiple setups on smaller machines, and the reinforced bed casting resists deflection under heavy electrode loads. For die and mold shops handling automotive, appliance, or heavy equipment tooling, this capacity translates directly into fewer setups, less handling risk, and shorter lead times.
High-Current Generator with Adaptive Pulse Control

High-Current Generator with Adaptive Pulse Control

Our Large EDM Machine uses a 300 A generator that reaches material removal rates up to 1,200 mm3/min on 1.2738 tool steel, roughly 35 percent faster than conventional 100 A systems. Adaptive pulse control continuously adjusts on-time and off-time based on gap conditions, which reduces electrode wear and protects fine details. One customer in India lowered electrode wear from 0.4 percent to 0.18 percent using copper-tungsten electrodes, cutting electrode replacement costs and improving dimensional consistency. The generator also delivers fine-finish capability below Ra 0.8 micrometres when required, so a single machine can handle both roughing and finishing. This reduces the need to move work between machines, saving handling time and preserving accuracy. For tool rooms running mixed production, the ability to switch from aggressive roughing to fine detail burning without changing setup is a major efficiency gain. The generator cabinet is burn-in tested for 72 hours at full load.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop