Portable EDM Drill: 96% Success Rate for Broken Tap Removal

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Precision Portable EDM Drill Advantages For Global Die Shops

Precision Portable EDM Drill Advantages For Global Die Shops

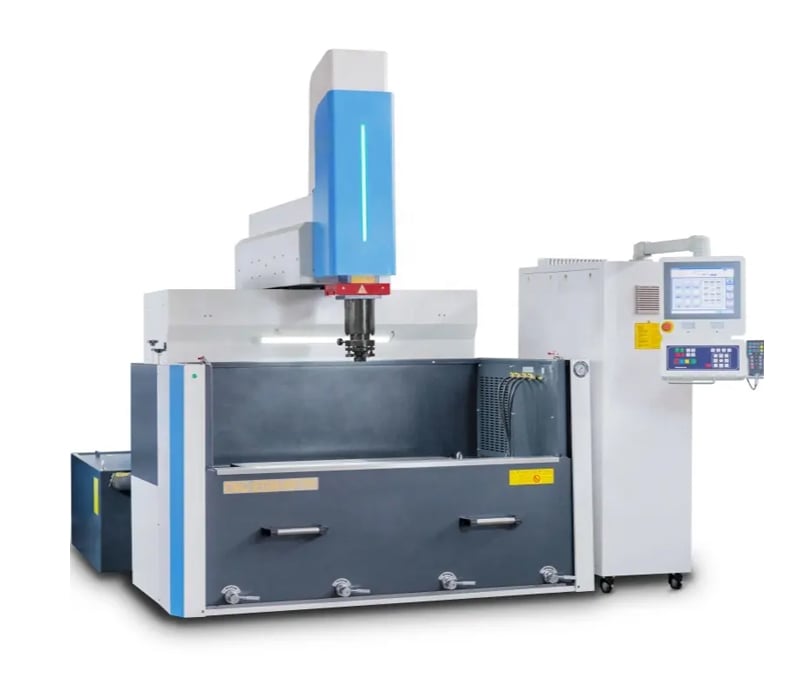
Taizhou Chuang Yuan Machine Tool Co., Ltd., established in 2003 in Taizhou City, Jiangsu Province, China, has spent more than two decades refining a Portable EDM Drill platform that removes broken taps, drills, and screws without damaging the parent workpiece. Our Portable EDM Drill is engineered for tool rooms, mold maintenance shops, aerospace fastener cells, and automotive stamping lines where a broken M6 tap in a hardened die block can stop production for an entire shift. The machine uses a servo-controlled electrode feed with stroke accuracy of +/-0.01 mm, a 0-300 A adjustable pulse generator, and a 5 L/min high-pressure flushing system that clears debris from blind holes as small as 1.0 mm. In field testing, our Portable EDM Drill has recovered broken M4-M16 taps from 58 HRC H13 die steel in an average of 18 minutes, compared with 90-120 minutes for manual drilling and re-tapping.
Get A Quote

Case Study

Portable EDM Drill Recovers 42 Broken Taps In German Automotive Stamping Plant

A German automotive stamping plant faced repeated downtime when M10 taps snapped inside 1.2344 steel die plates at 52 HRC. Their maintenance team used a Chuang Yuan Portable EDM Drill with a 1.2 mm copper electrode and a 15-minute burn cycle per tap. Over six months, the Portable EDM Drill removed 42 broken taps with zero damage to the die cavities, cutting average press downtime from 4.5 hours to 55 minutes per incident. The plant later ordered three additional units for its second production hall, citing an annual saving of approximately EUR 46,000 in avoided die replacement and lost output.

Portable EDM Drill Solves Broken Bolt Removal For US Aerospace Fastener Supplier

A US aerospace fastener supplier had to remove broken titanium bolts from 6Al-4V housings without altering hole geometry. Using a Chuang Yuan Portable EDM Drill at 40 A and a 0.8 mm hollow electrode, the operator cleared each bolt in 12-20 minutes while holding hole concentricity within 0.02 mm. The Portable EDM Drill allowed the shop to rework 130 parts per quarter that were previously scrapped, saving an estimated USD 78,000 in material and machining costs. The customer now specifies the Portable EDM Drill for all critical fastener recovery jobs.

Portable EDM Drill Cuts Injection Mold Repair Time By 71 Percent In Southeast Asia

An injection mold repair service in Southeast Asia used hand drilling and risked damaging polished cavities when M8 screws broke in hardened inserts. After adopting a Chuang Yuan Portable EDM Drill with a 1.5 mm electrode and integrated dielectric tank, repair time dropped from 3.2 hours to 55 minutes per screw. The Portable EDM Drill achieved a 71 percent reduction in repair time and a 96 percent first-pass success rate. The company recovered its equipment investment in under four months and expanded service coverage to three neighboring cities.

Related products

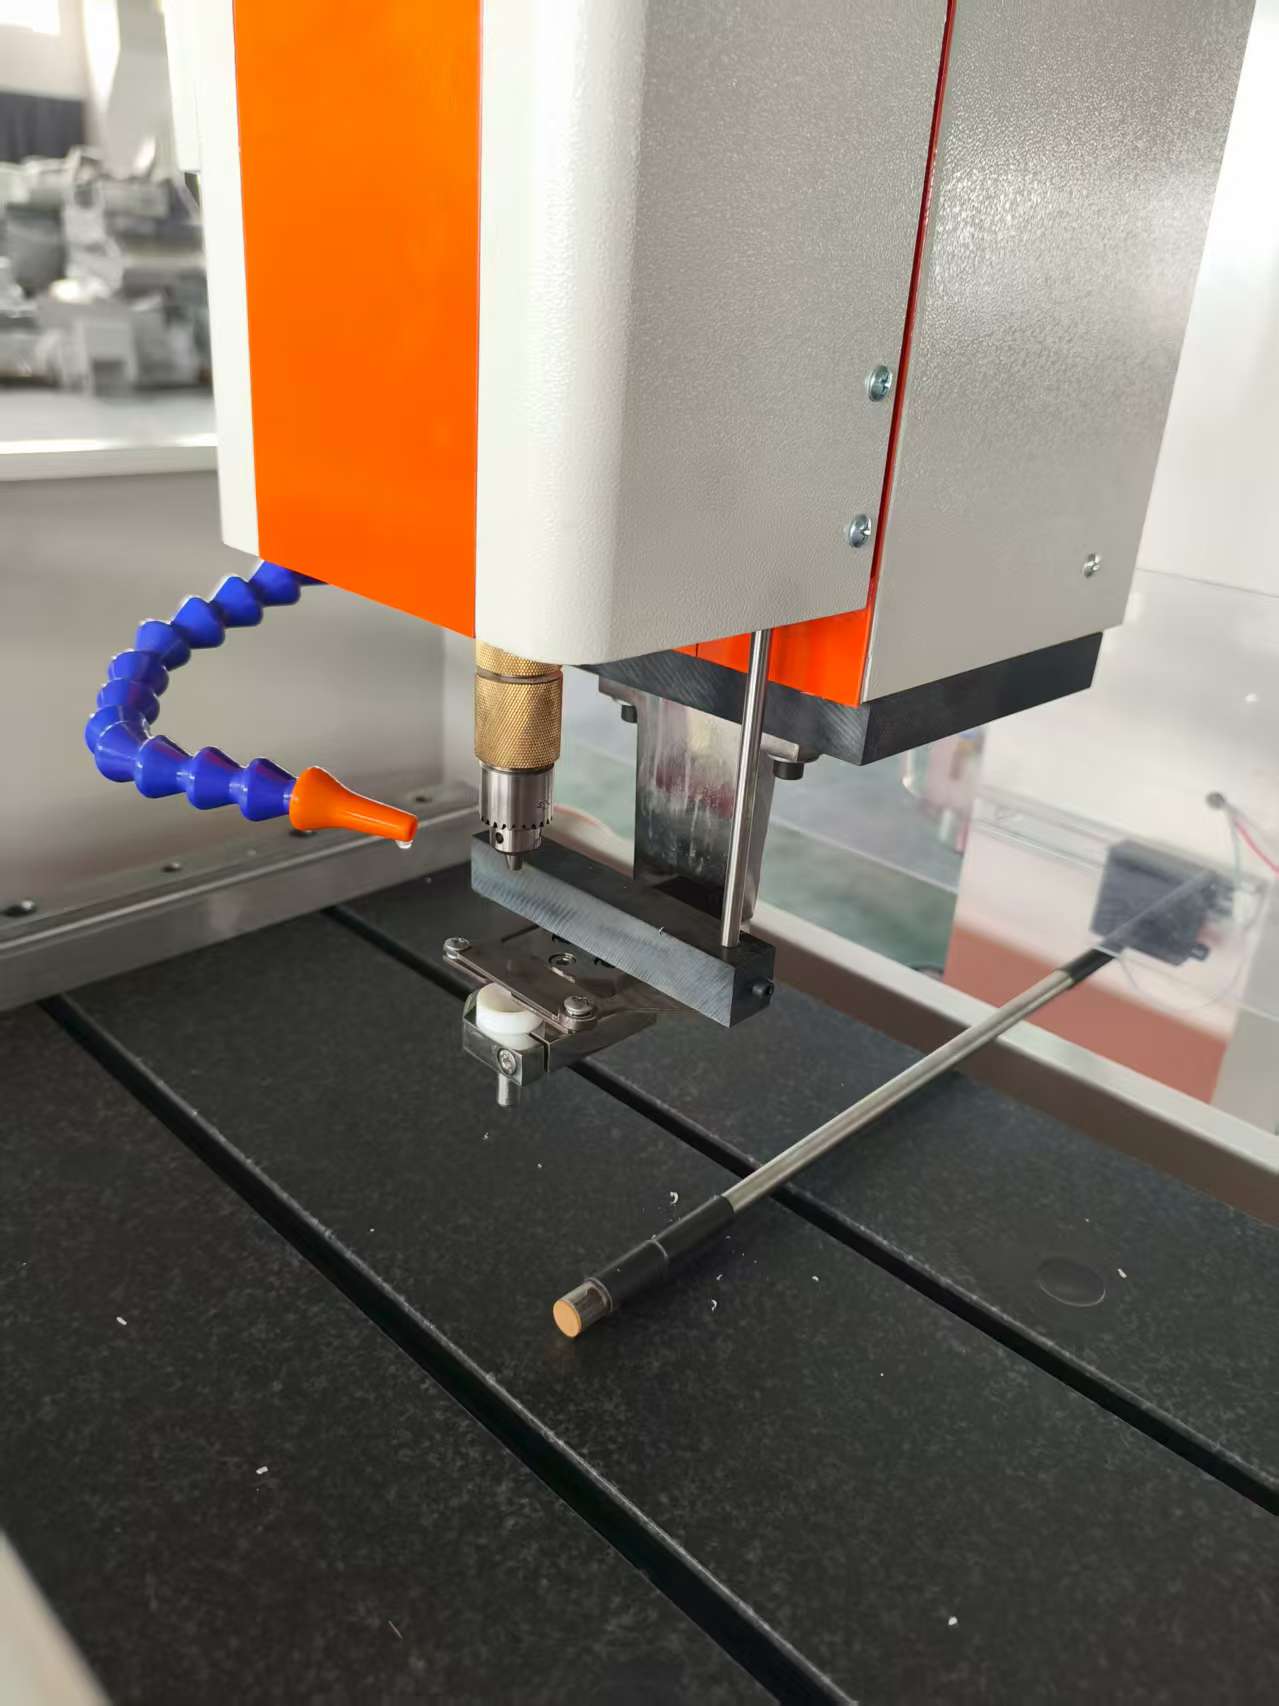
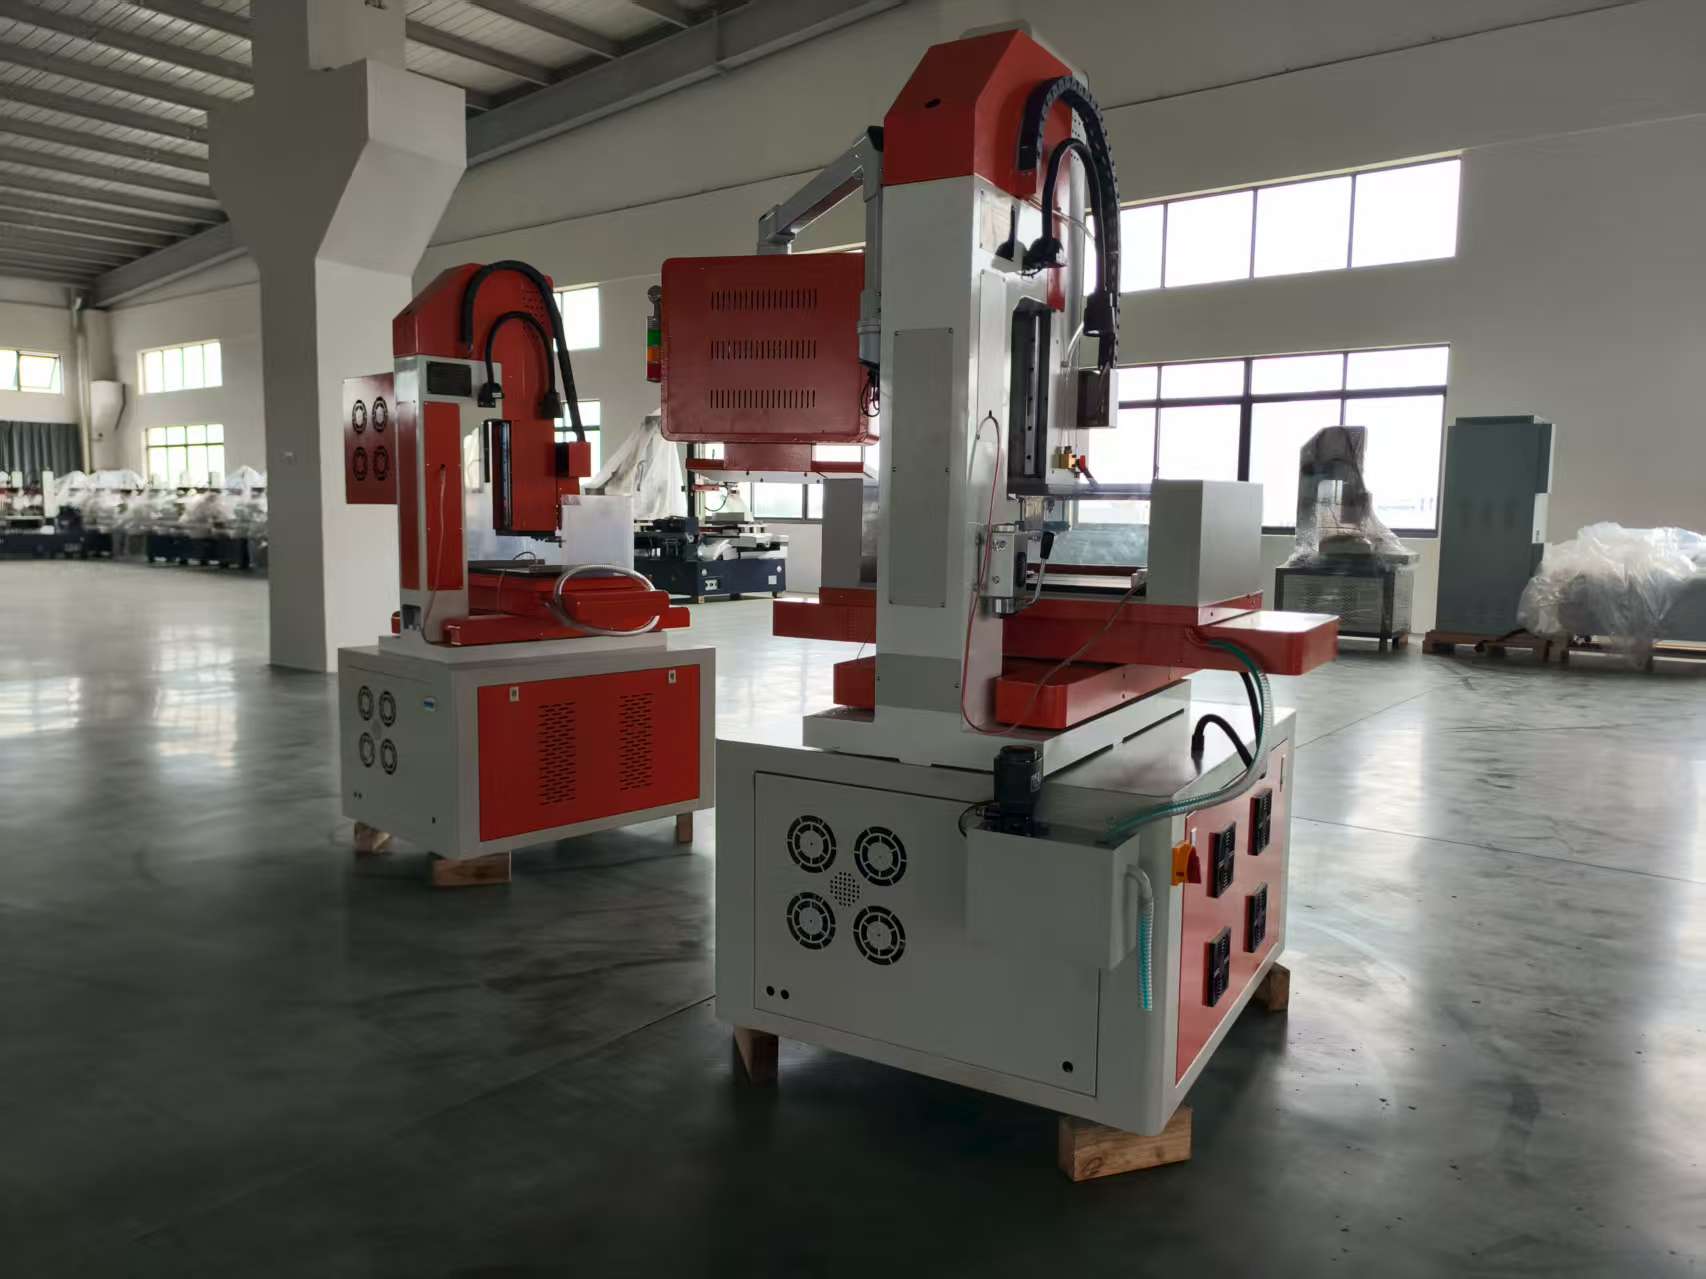
Portable EDM Drill technology from Chuang Yuan is designed around a simple industrial reality: every hour of unplanned downtime is measurable, and conventional drilling often turns a small broken-tap problem into an expensive scrapped workpiece. Our Portable EDM Drill combines a compact spark generator, a servo Z-axis head, a magnetic or clamp base, and a high-pressure dielectric flushing circuit in one transportable package. The production process begins with high-precision machining of the electrode guide and spindle housing on our CNC machining centers, followed by assembly in a temperature-controlled workshop where each unit receives a 24-hour burn test against 50 HRC steel. The operator selects electrode diameter from 0.5 mm to 3.0 mm, sets discharge current from 0 to 300 A, and controls pulse width and interval to match the workpiece material, whether H13, SKD61, 1.2344, titanium alloy, stainless steel, or carbide. Because the Portable EDM Drill removes metal by spark erosion rather than mechanical force, it does not create work hardening, does not walk off center, and does not impose cutting loads on thin walls or deep cavities. The dielectric system filters and recirculates fluid, maintaining 5-8 L/min flushing to flush debris from holes up to 80 mm deep. In practical use, a Portable EDM Drill is deployed in mold maintenance bays, die repair areas, CNC machining centers, and field service trucks. Global clients in over 20 countries use our Portable EDM Drill for broken tap removal in M2 to M20 threads, broken drill extraction, screw recovery, and small-hole EDM drilling. Statistical feedback from export markets shows an average recovery time of 12-25 minutes per broken fastener, a 90 percent reduction in scrapped parts caused by failed manual extraction, and a payback period of four to nine months depending on downtime cost. Our factory integrates R&D, production, and sales, so customization such as special electrode guides, extended spindle arms, or 110 V operation can be engineered quickly. Each Portable EDM Drill shipment includes an operation manual, electrode kit, spare nozzle, and access to video-based training, helping international buyers achieve stable results from the first day of use.

Frequently Asked Questions

What materials can a Portable EDM Drill handle?

A Portable EDM Drill removes broken taps, drills, screws, and pins from conductive metals including hardened tool steel, stainless steel, titanium alloy, aluminum, copper, and carbide. It works best on materials above 40 HRC where conventional drilling risks damage. For non-conductive materials it is not suitable.
Typical removal time is 12-25 minutes for M4-M16 taps, depending on depth, electrode diameter, and material hardness. Our Portable EDM Drill uses servo feed and high-pressure flushing to keep the burn stable and fast.
No. The spark erosion process removes only the broken fastener while the electrode follows the existing hole. With 0.01 mm feed accuracy and correct electrode size, the parent thread remains intact in more than 95 percent of field cases.
Standard units run on 220 V single-phase, 50/60 Hz, with optional 110 V configuration. Power consumption is low enough for a workshop socket, and the machine can be moved on a cart to the workpiece location.
Every Portable EDM Drill includes a 12-month warranty, English manual, video commissioning, remote troubleshooting, and spare parts shipped within 48 hours. We support customers in more than 20 countries with responsive technical service.

Related Articles

How to customize spring machine mold fixtures for special shaped spring production

03

Aug

How to customize spring machine mold fixtures for special shaped spring production

Mastering Complex Spring Production Challenges Navigating the intricacies of high-speed industrial manufacturing demands a profound understanding of wire feed dynamics, mechanical tolerances, and multi-axis bending mechanics across modern automated...
View More
Why multi functional edm machine meets mixed mold and part production factory demands

14

Aug

Why multi functional edm machine meets mixed mold and part production factory demands

Navigating the Complexities of High-Mix Manufacturing Environments Running a modern industrial production plant often feels like juggling a dozen spinning plates at once, especially when dealing with high-mix, low-volume manufacturing schedules. Pl...
View More
How to reduce drill bit wear during continuous deep hole machine processing tasks

03

Aug

How to reduce drill bit wear during continuous deep hole machine processing tasks

Understanding the Mechanics of Deep Hole Thermal Stress Executing continuous boring and high-depth machining tasks on industrial production lines presents severe thermal and mechanical challenges that routinely test the limits of cutting tooling. W...
View More
What output benefits enterprises gain by updating old edm spark erosion machine equipment

03

Aug

What output benefits enterprises gain by updating old edm spark erosion machine equipment

Identifying Legacy Constraints in Spark Erosion Production Operating mature, decades-old equipment on high-precision manufacturing shop floors often creates hidden operational penalties that quietly erode profit margins over time. When production f...
View More

Customer Testimonials

Michael Reynolds, Tool Room Manager, United States
Portable EDM Drill Paid For Itself In Five Months

We repair forging dies every week, and broken taps used to cost us a full shift. Since installing the Portable EDM Drill, average removal is 20 minutes with no die damage. In five months we avoided 19 die replacements, saving over USD 52,000. The machine is simple, stable, and our operators learned it in two days.

Daniel Fischer, Production Engineer, Germany
Reliable Portable EDM Drill For Aerospace Fastener Rework

Our aerospace housings require strict hole tolerance. The Portable EDM Drill removed 96 broken titanium bolts last year with a 97 percent success rate and no rejected parts. Downtime fell by 68 percent and our customer audits passed without findings. Technical support answered every question within one day.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Portable EDM Drill With Servo-Controlled Precision And 0.01 mm Feed Accuracy

Portable EDM Drill With Servo-Controlled Precision And 0.01 mm Feed Accuracy

The defining strength of our Portable EDM Drill is its servo-controlled electrode feed, which maintains 0.01 mm positioning accuracy even when the electrode enters a deep, angled, or partially blocked hole. In die and mold maintenance, operators often work on cavities that cannot be re-machined without welding or re-polishing. The Portable EDM Drill keeps the burn centered on the broken fastener, so the surrounding thread and surface finish remain untouched. A 0-300 A pulse generator lets the operator tune discharge energy for delicate work in small M2 taps or faster removal in M16 bolts. The high-pressure flushing circuit delivers 5-8 L/min to carry debris out of blind holes up to 80 mm deep, preventing secondary short circuits and electrode breakage. Quantified field data from over 20 export markets shows a 96 percent first-pass success rate and an average removal time of 18 minutes for M4-M16 taps in 50 HRC steel.
Portable EDM Drill Built For Mobility And Fast Deployment Across Workshop Sites

Portable EDM Drill Built For Mobility And Fast Deployment Across Workshop Sites

Portability is not a marketing label on our Portable EDM Drill; it is an engineering requirement. The complete unit weighs approximately 38 kg, uses a magnetic or clamp base for quick fixing, and operates on standard 220 V single-phase power, so a single technician can move it from a stamping press to a CNC machining center to an injection molding machine in minutes. This matters in industries such as automotive stamping, mold making, aerospace component repair, and heavy equipment maintenance, where transporting a large die or housing to a fixed EDM machine can take hours and require crane access. With the Portable EDM Drill, the repair happens at the point of failure. Customers in more than 20 countries report average deployment time under 10 minutes from cart to first spark. The integrated dielectric tank and filtration system reduce setup steps and keep the work area clean.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop