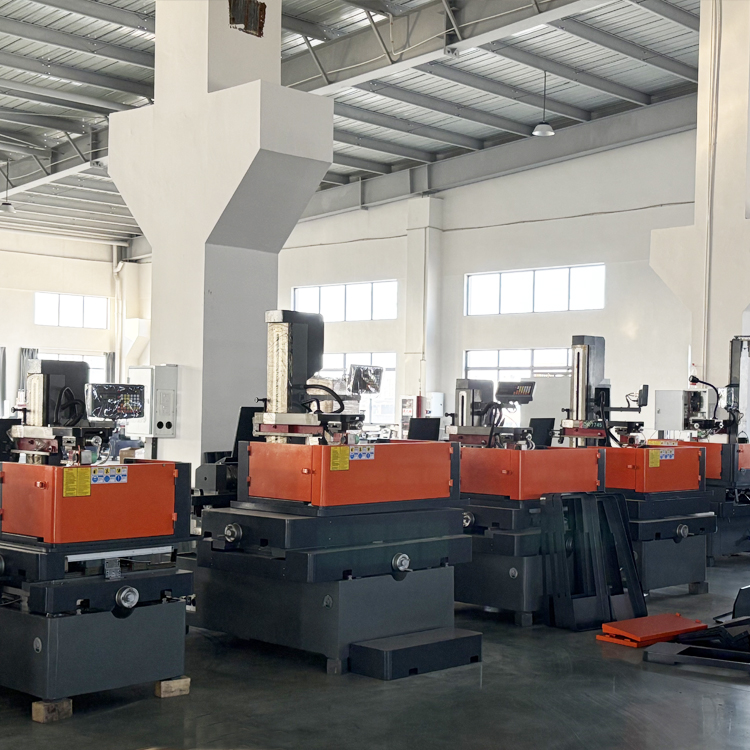
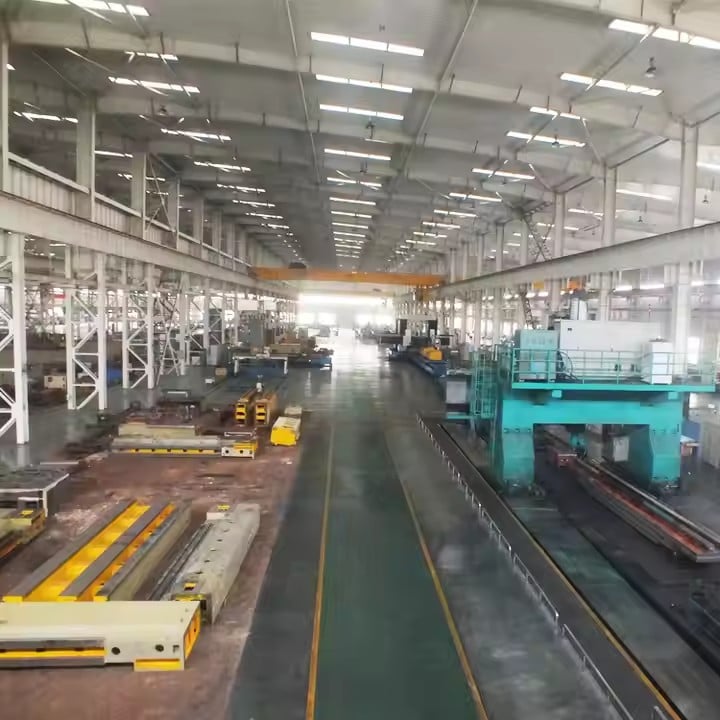
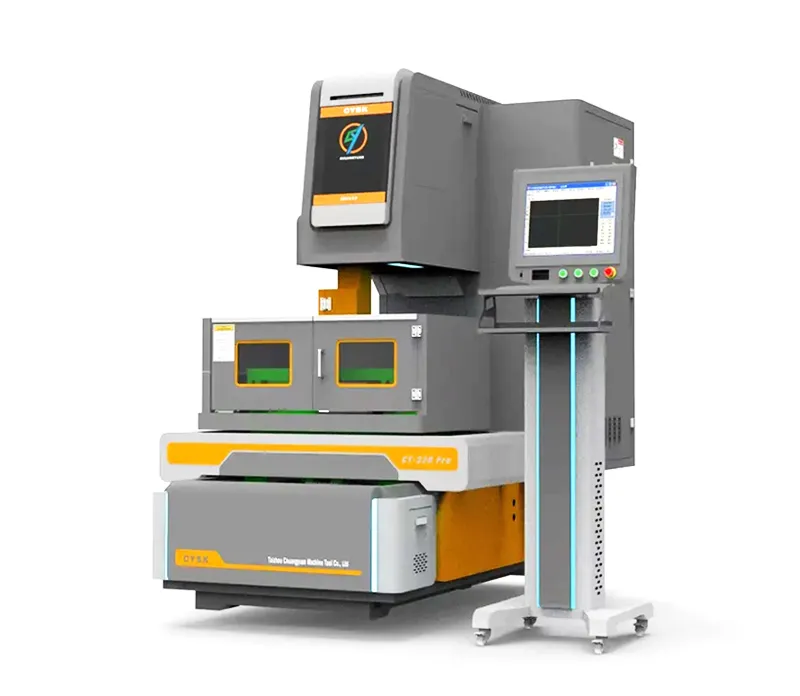
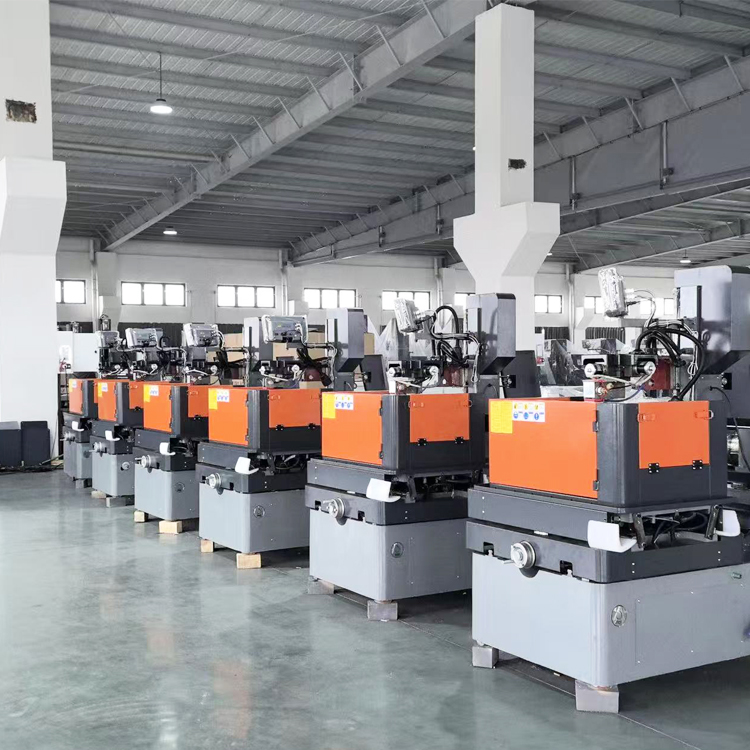
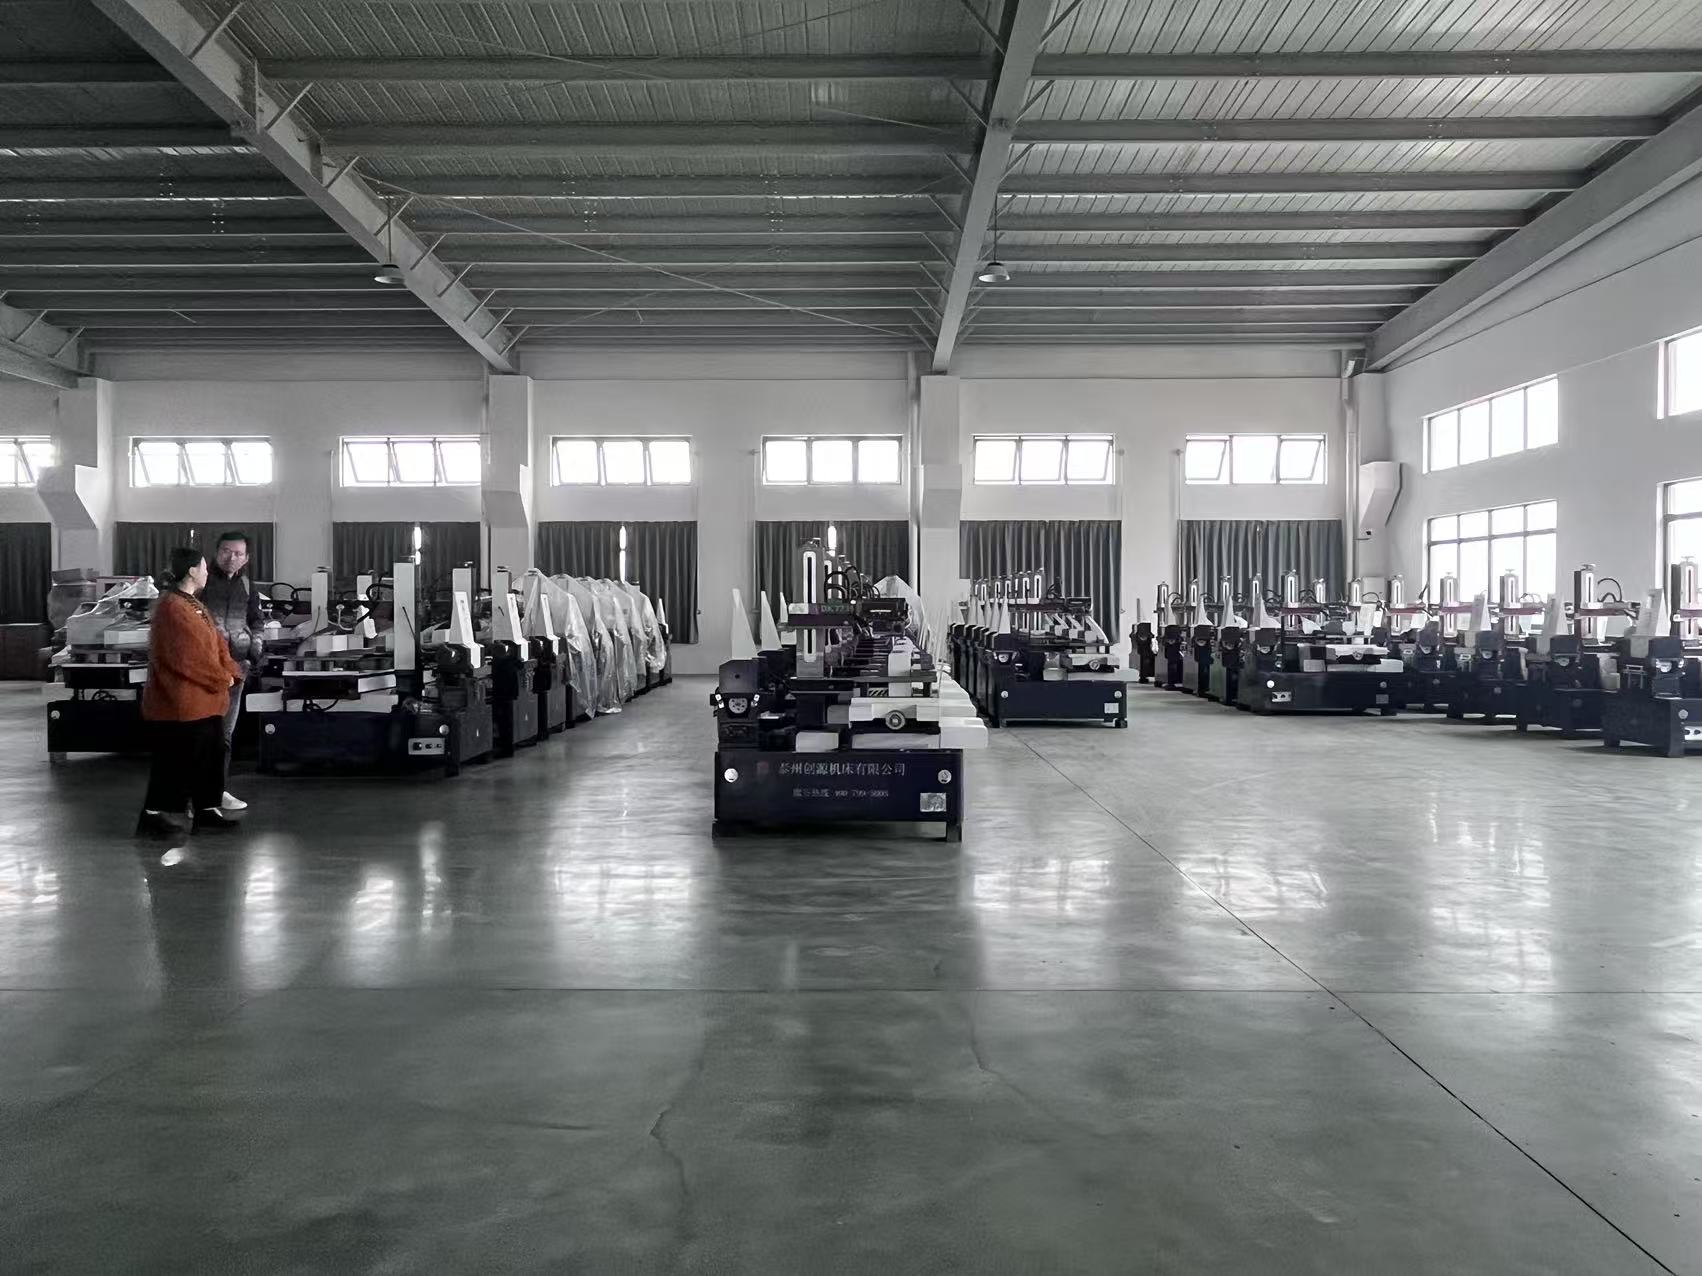
The production of a reliable Mesin Edm Wire Cut machine begins long before assembly. At Taizhou Chuang Yuan Machine Tool Co., Ltd., founded in 2003 in Jiangsu Province, China, each Mesin Edm Wire Cut platform passes through a structured chain of research, casting, machining, assembly, calibration, and validation. We start with finite element analysis of the C-frame and column, selecting high-grade cast iron that is naturally aged for six months to relieve internal stress. This step matters because thermal drift of even 2 degrees Celsius can shift wire position by several microns during a 10-hour unattended cut. After rough machining on our own gantry mills, the bed, column, and table are ground to flatness within 0.01 mm per meter, then hand-scraped at critical guide interfaces to ensure long-term geometric stability. The wire transport system uses precision diamond guides and sealed bearings rated for more than 8,000 hours, while the pulse generator is tuned per machine to deliver stable discharge at currents from 1 A to 12 A. On the software side, our engineers preload cutting parameter libraries for common materials such as SKD11, SKD61, 718H, NAK80, carbide, copper, and aluminum. Operators in different markets work differently: European shops tend to prioritize surface finish and full traceability, Southeast Asian factories often run lights-out shifts and prioritize wire threading reliability, and Middle Eastern job shops value quick changeovers between jobs. Our parameter library and English, Spanish, and Russian interfaces reflect those habits. Before shipment, every Mesin Edm Wire Cut unit runs a 72-hour continuous cutting test on hardened steel, and dimensional reports are recorded with a laser interferometer; axial positioning is verified to +/-0.003 mm and repeatability to +/-0.002 mm. Globally, our Mesin Edm Wire Cut systems serve mold makers in Germany, die stampers in Mexico, aerospace subcontractors in Turkey, and electronics tooling plants in Vietnam. In one documented project, a Vietnamese connector mold producer cut 0.3 mm wide slots in 55 HRC steel at 150 mm2/min, holding tolerance within +/-0.004 mm across a 300 mm workpiece, which eliminated a secondary grinding operation and shortened lead time by four days. Service data shows that more than 90 percent of technical tickets are resolved remotely within one business day, supported by a spare parts warehouse that ships critical components within 48 hours. We also provide on-site commissioning, operator training, and preventive maintenance schedules that keep wire consumption predictable, typically 0.28 to 0.35 kg per hour of cutting. This end-to-end discipline is how a Mesin Edm Wire Cut machine from Chuang Yuan delivers repeatable accuracy, documented uptime, and lower cost per part for buyers in more than 20 countries.