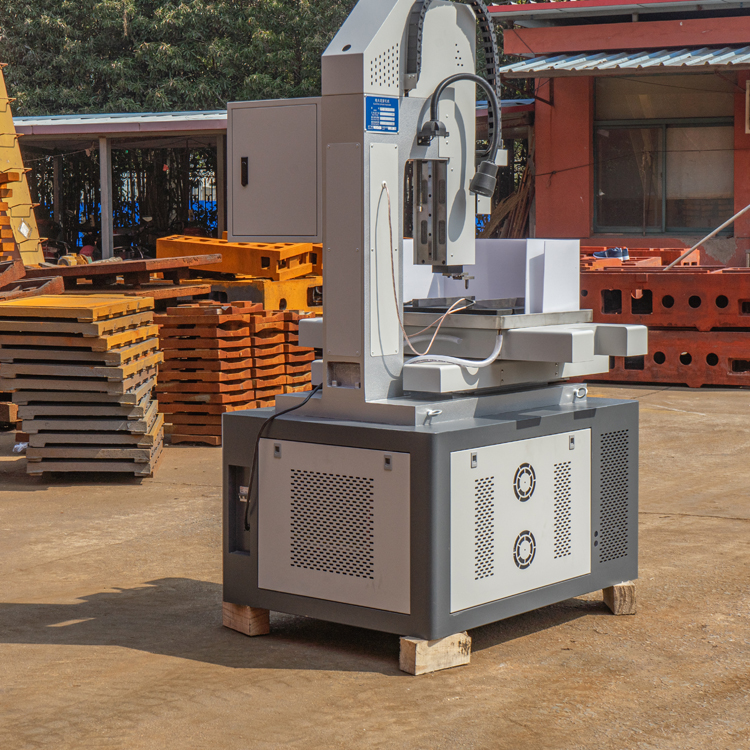
Small EDM Drilling Machine | 0.2–3.0 mm Micro-Hole Precision

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Small EDM Drilling Machine Built by Taizhou Chuang Yuan Machine Tool Co., Ltd. for Precision Micro-Hole Drilling

Small EDM Drilling Machine Built by Taizhou Chuang Yuan Machine Tool Co., Ltd. for Precision Micro-Hole Drilling

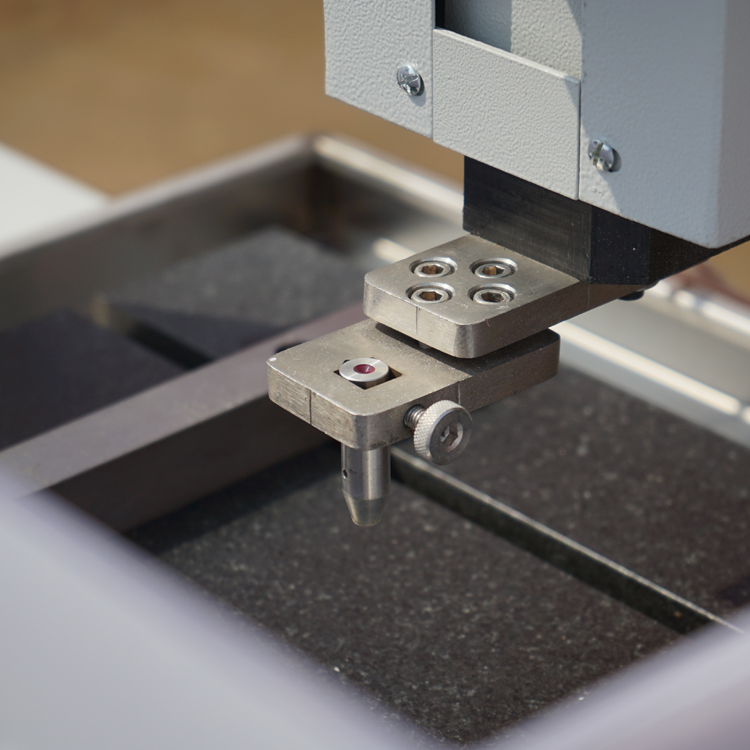
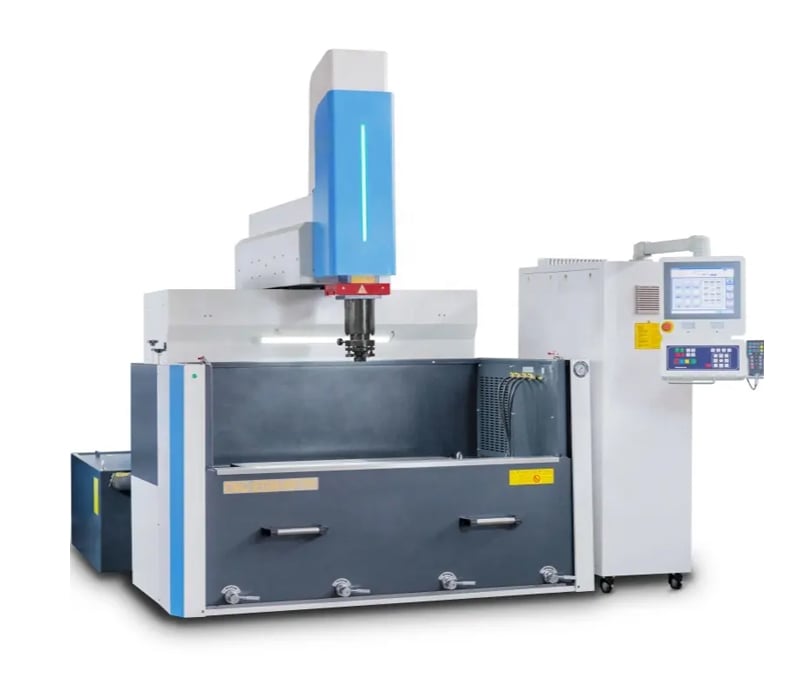
Since 2003, Taizhou Chuang Yuan Machine Tool Co., Ltd. has engineered a small EDM drilling machine that helps mold shops, aerospace suppliers, and medical device manufacturers drill precise micro-holes in hardened steel, carbide, and heat-resistant alloys. Our small EDM drilling machine uses a servo-controlled spindle, high-frequency pulse power supply, and granite base to hold positioning accuracy within 0.005 mm and repeatability within 0.003 mm, while the 0.2-3.0 mm electrode range covers cooling holes, fuel injector orifices, and wire-cut start holes. In a typical 8-hour shift, the machine completes 180-260 holes in 54 HRC tool steel, cutting drilling time by up to 60% compared with manual methods for holes below 1.0 mm. The small EDM drilling machine operates with deionized water, avoiding thermal deformation from conventional drilling and reducing tooling costs. A European mold maker used our small EDM drilling machine to produce 0.6 mm ejector-pin holes in a 48-cavity mold.
Get A Quote

Case Study

German Mold Maker Cuts 0.6 mm Hole Cycle Time by 40 Percent

A German mold maker producing 48-cavity injection molds needed 0.6 mm ejector-pin holes in hardened 1.2344 steel at 50 HRC. Manual drilling caused frequent electrode breakage and required secondary polishing. After installing our small EDM drilling machine, they used a 0.6 mm brass electrode, 120 V open-circuit voltage, and 1.5 A peak current. Hole position accuracy reached 0.005 mm, surface roughness Ra 1.6 um, and cycle time dropped from 14 minutes to 8 minutes per hole, a 40% reduction. The shop now completes 240 holes per shift and reduced electrode consumption by 25%. The small EDM drilling machine also provided a stable start hole for their wire EDM, improving overall mold delivery by 3 days.

Indian Fuel Injector Plant Raises Throughput by 35 Percent

An Indian fuel injector manufacturer drills 0.25 mm spray holes in 17-4PH stainless steel at 42 HRC. Before the small EDM drilling machine, the plant averaged 220 pieces per shift with 8% scrap. After installing the small EDM drilling machine, they applied a 0.25 mm tungsten electrode, 100 V discharge voltage, and 0.8 A current. Throughput rose to 300 pieces per shift, a 35% gain, while scrap fell to 1.8%. The machine's servo control maintained the 0.25 mm hole diameter within a 0.01 mm tolerance, cutting inspection time by 20%. The plant now exports to European automakers and credits the small EDM drilling machine for meeting strict IATF 16949 quality requirements.

US Aerospace Supplier Solves 0.5 mm Cooling Hole Challenge in Inconel 718

A US aerospace supplier needed 0.5 mm cooling holes in Inconel 718 turbine blades at 38 HRC. Conventional drilling caused work hardening and tool failure. Our small EDM drilling machine used a 0.5 mm copper-tungsten electrode, 140 V voltage, and 2.0 A current to drill 120 holes per blade with 0.004 mm positioning accuracy and no recast layer above 0.01 mm. The supplier reduced scrap from 12% to 2.5% and cut drilling time from 22 minutes to 9 minutes per blade. With the small EDM drilling machine, they now produce 60 blades per week and passed NADCAP audit. The supplier plans to add a second small EDM drilling machine to meet rising demand.

Related products

Taizhou Chuang Yuan Machine Tool Co., Ltd. has manufactured precision machine tools since 2003, and our small EDM drilling machine reflects more than two decades of research, production, and sales experience. The machine is built around a rigid granite base, a precision linear guideway, and a servo-controlled Z-axis that together limit vibration during micro-hole drilling. Its high-frequency pulse power supply delivers stable discharges from 0.2 mm to 3.0 mm electrodes, making the small EDM drilling machine suitable for hardened steel, carbide, Inconel, titanium, and stainless steel. In production, the operator loads the workpiece, sets the electrode, and selects a discharge program; the small EDM drilling machine then drills automatically, reducing dependence on operator skill. We produce key components in-house, including the spindle assembly, power supply, and control cabinet, and each small EDM drilling machine undergoes a 48-hour test run and laser interferometer verification before shipment. Our quality system follows ISO 9001, and our export team has served customers in more than 20 countries, including Germany, India, the United States, Turkey, and Brazil. A European mold shop uses our small EDM drilling machine to drill 0.6 mm holes in 48-cavity molds, cutting cycle time by 40%. An Indian fuel injector plant increased throughput by 35% with a 0.25 mm electrode, while a US aerospace supplier reduced scrap from 12% to 2.5% on Inconel 718 turbine blades. These results come from a machine that consumes low power, uses deionized water, and requires minimal floor space, so even small workshops can adopt it. We also provide remote support, spare parts kits, and English manuals. Our engineers help customers integrate the small EDM drilling machine with existing wire EDM and milling equipment for a complete micro-hole process. With growing demand for miniaturized parts in automotive, medical, and aerospace industries, the small EDM drilling machine gives buyers a practical path to higher precision and faster delivery schedules.

Frequently Asked Questions

What materials can a small EDM drilling machine process?

A small EDM drilling machine can process conductive materials such as hardened steel, tool steel, carbide, Inconel, titanium, stainless steel, and copper alloys. It is widely used for holes from 0.2 mm to 3.0 mm, including cooling holes, injector orifices, and wire EDM start holes. For non-conductive materials, EDM is not suitable, so we recommend discussing your workpiece with our engineers before purchase.
Our small EDM drilling machine can drill holes as small as 0.2 mm with a suitable electrode and stable discharge parameters. For best results, we recommend a 0.3 mm or larger electrode for deep holes. Accuracy is typically within 0.005 mm positioning and 0.003 mm repeatability. Actual results depend on material, hole depth, and electrode condition, so our team provides a process recommendation for your specific application.
Installation usually takes one to two days, depending on site preparation, power supply, and water system readiness. Our engineers provide on-site training for operators and maintenance staff, covering setup, program editing, electrode replacement, and daily maintenance. For remote locations, we offer video-guided installation and English manuals. Most customers reach stable production within one week after the small EDM drilling machine is installed.
We provide a 12-month warranty on major components, remote technical support, spare parts availability, and English operation manuals. Our export team has served customers in more than 20 countries, so we understand different voltage and plug standards. We can ship spare parts by express and provide video troubleshooting. For complex issues, our engineers coordinate with your team to diagnose the small EDM drilling machine and restore production quickly.
Consider your typical hole diameter, material hardness, workpiece size, and daily output target. Small EDM drilling machines vary in spindle travel, power supply, and control features. Share your drawings and sample parts with our engineers, and we will recommend a model, electrode size, and process parameters. If needed, we can also advise on fixtures and water treatment to help your small EDM drilling machine run reliably.

Related Articles

The correct handling method for insufficient machining accuracy of fast wire cutting machine

13

Dec

The correct handling method for insufficient machining accuracy of fast wire cutting machine

View More
Why modular spring machine supports fast switching of different spring production types

14

Jul

Why modular spring machine supports fast switching of different spring production types

Production Bottlenecks of Traditional Integrated Spring Forming Equipment Modern metal forming manufacturing increasingly features diversified product specifications and mixed batch production. Many production facilities need to process springs ...
View More
What after sales service should reliable edm drilling machine suppliers provide

14

Jul

What after sales service should reliable edm drilling machine suppliers provide

The Evolution of Flexible Manufacturing Through Modular Architecture Modern industrial landscapes demand a high degree of adaptability, where the ability to transition production configurations quickly defines a facility’s operational rhythm....
View More
What export quality standards international clients require for wire cutting machine products

03

Aug

What export quality standards international clients require for wire cutting machine products

Understanding International Export Compliance in Precision Machining Navigating the complex landscape of global industrial trade requires a thorough understanding of the stringent technical benchmarks that overseas buyers mandate for advanced metal...
View More

Customer Testimonials

Klaus Meier, Mold Shop Manager, Germany
Reliable Micro-Hole Drilling for Mold Production

Our small EDM drilling machine has become the bottleneck solver in our mold shop. We drill 0.6 mm ejector-pin holes in 48-cavity molds, and cycle time dropped by 40% after switching to this machine. Scrap from broken electrodes fell by 25%, and the positioning accuracy of 0.005 mm meets our tight tolerances. The training was clear and practical, so our operators were confident within days.

Rajesh Nair, Production Director, India
Strong Support and Consistent Results in Fuel Injector Production

We use the small EDM drilling machine to drill 0.25 mm injector holes in 17-4PH stainless steel. Throughput increased by 35%, and scrap dropped from 8% to 1.8%. The machine holds diameter tolerance within 0.01 mm, which reduced inspection time by 20%. The export team was responsive and helped us adapt the machine to our voltage and water system.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
High-Precision Servo Control for Sub-Millimeter Holes

High-Precision Servo Control for Sub-Millimeter Holes

The small EDM drilling machine uses a servo-controlled Z-axis and a high-frequency pulse power supply to maintain stable discharge during micro-hole drilling. This design holds positioning accuracy within 0.005 mm and repeatability within 0.003 mm, which is critical for 0.2-1.0 mm holes in hardened steel and carbide. In a German mold shop, the small EDM drilling machine drilled 0.6 mm holes in 1.2344 steel at 50 HRC with Ra 1.6 um surface finish, reducing cycle time by 40%. For aerospace and medical applications, the machine minimizes recast layer and heat-affected zones, helping customers pass NADCAP and IATF audits. The control system includes stored programs for common materials, so operators can switch between jobs quickly. Because the small EDM drilling machine drills without mechanical force, it avoids work hardening and tool breakage, especially in Inconel and titanium.
Compact, Low-Consumption Design Suits Small and Medium Workshops

Compact, Low-Consumption Design Suits Small and Medium Workshops

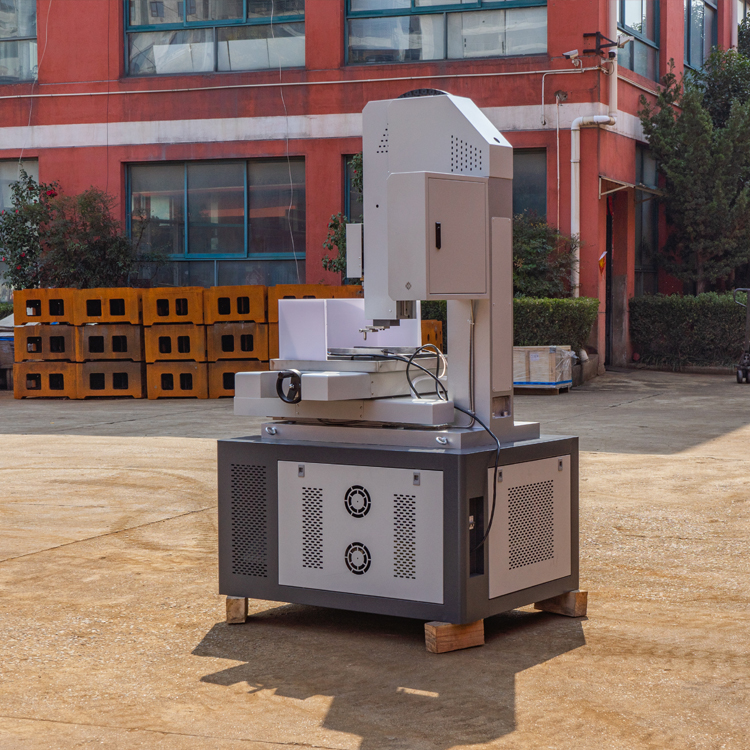
Our small EDM drilling machine is designed with a compact footprint and low power consumption, making it suitable for small and medium workshops with limited floor space. The machine uses deionized water as the dielectric, which reduces operating cost and avoids oil disposal. It requires single-phase or three-phase power depending on model, and the control cabinet is integrated to simplify installation. In an Indian fuel injector plant, the small EDM drilling machine increased throughput by 35% while cutting scrap from 8% to 1.8%, proving that a compact machine can deliver production-level results. The machine's electrode consumption is controlled by optimized discharge parameters, reducing consumable cost by up to 25% in mold applications. For customers in more than 20 countries, we provide voltage adaptation, plug options, and English manuals.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop