Wire Erosion EDM Machines | ±0.003 mm Accuracy & 180 mm²/min Speed

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Wire Erosion EDM Solutions Engineered by Taizhou Chuang Yuan Machine Tool Since 2003

Wire Erosion EDM Solutions Engineered by Taizhou Chuang Yuan Machine Tool Since 2003

Since 2003, Taizhou Chuang Yuan Machine Tool Co., Ltd. has engineered Wire Erosion EDM systems that deliver repeatable micron-level accuracy for tool rooms, aerospace shops, and medical device manufacturers across more than 20 exporting countries and regions. Our Wire Erosion EDM platforms combine rigid cast-iron beds, precision linear guides, and adaptive pulse generators to hold ±0.003 mm positioning accuracy and Ra 0.4 µm surface finish on hardened steel above 60 HRC. In daily use, mold makers in Germany run unattended overnight cycles on hardened die inserts, while automotive fixture builders in Mexico cut 12 mm brass and carbide punches at 180 mm²/min, reducing electrode-related costs by eliminating the need for dedicated electrodes. A Turkish aerospace subcontractor replaced aging equipment with our Wire Erosion EDM line and cut turbine blade root form errors from 0.02 mm to 0.006 mm within one quarter, lowering scrap from 7% to 1.5%. Because we manufacture in-house.
Get A Quote

Case Study

Wire Erosion EDM Cuts Mold Insert Lead Time by 40% for German Toolmaker

A German mold shop producing packaging inserts struggled with 0.015 mm profile deviation on hardened 1.2344 steel, causing seven-day rework loops. They installed our Wire Erosion EDM with a 0.25 mm brass wire package and adaptive flushing. Within six weeks, profile deviation fell to 0.004 mm, polishing time dropped 35%, and insert lead time decreased from 15 days to 9 days. The shop now runs 22 hours of unattended cutting daily, and the owner confirmed that Wire Erosion EDM accuracy directly won them two new beverage mold contracts worth EUR 180,000 annually.

Wire Erosion EDM Boosts Aerospace Blade Root Accuracy to 0.006 mm in Turkey

A Turkish aerospace subcontractor needed tighter blade root forms on Inconel 718. Their legacy machines drifted 0.02 mm over long cuts, creating 7% scrap. Our Wire Erosion EDM with closed-loop thermal compensation and multi-pass trimming held 0.006 mm over 300 mm travel. Scrap fell to 1.5%, machine utilization rose to 88%, and on-time delivery improved from 82% to 97% within two quarters, helping them secure a European engine component order.

Wire Erosion EDM Raises Punch Output 25% for Mexican Automotive Supplier

A Mexican automotive fixture supplier cut 12 mm brass and carbide punches on outdated equipment at 140 mm²/min with frequent wire breaks. Our Wire Erosion EDM, configured with high-speed flushing and automatic wire threading, reached 180 mm²/min and cut wire breakage by 70%. Output per shift rose 25%, tooling cost per part dropped 18%, and the supplier now supports three assembly lines without adding a second shift, directly improving their profitability. Products Title: Precision Wire Erosion EDM Machines Built for Demanding Tool Rooms

Related products

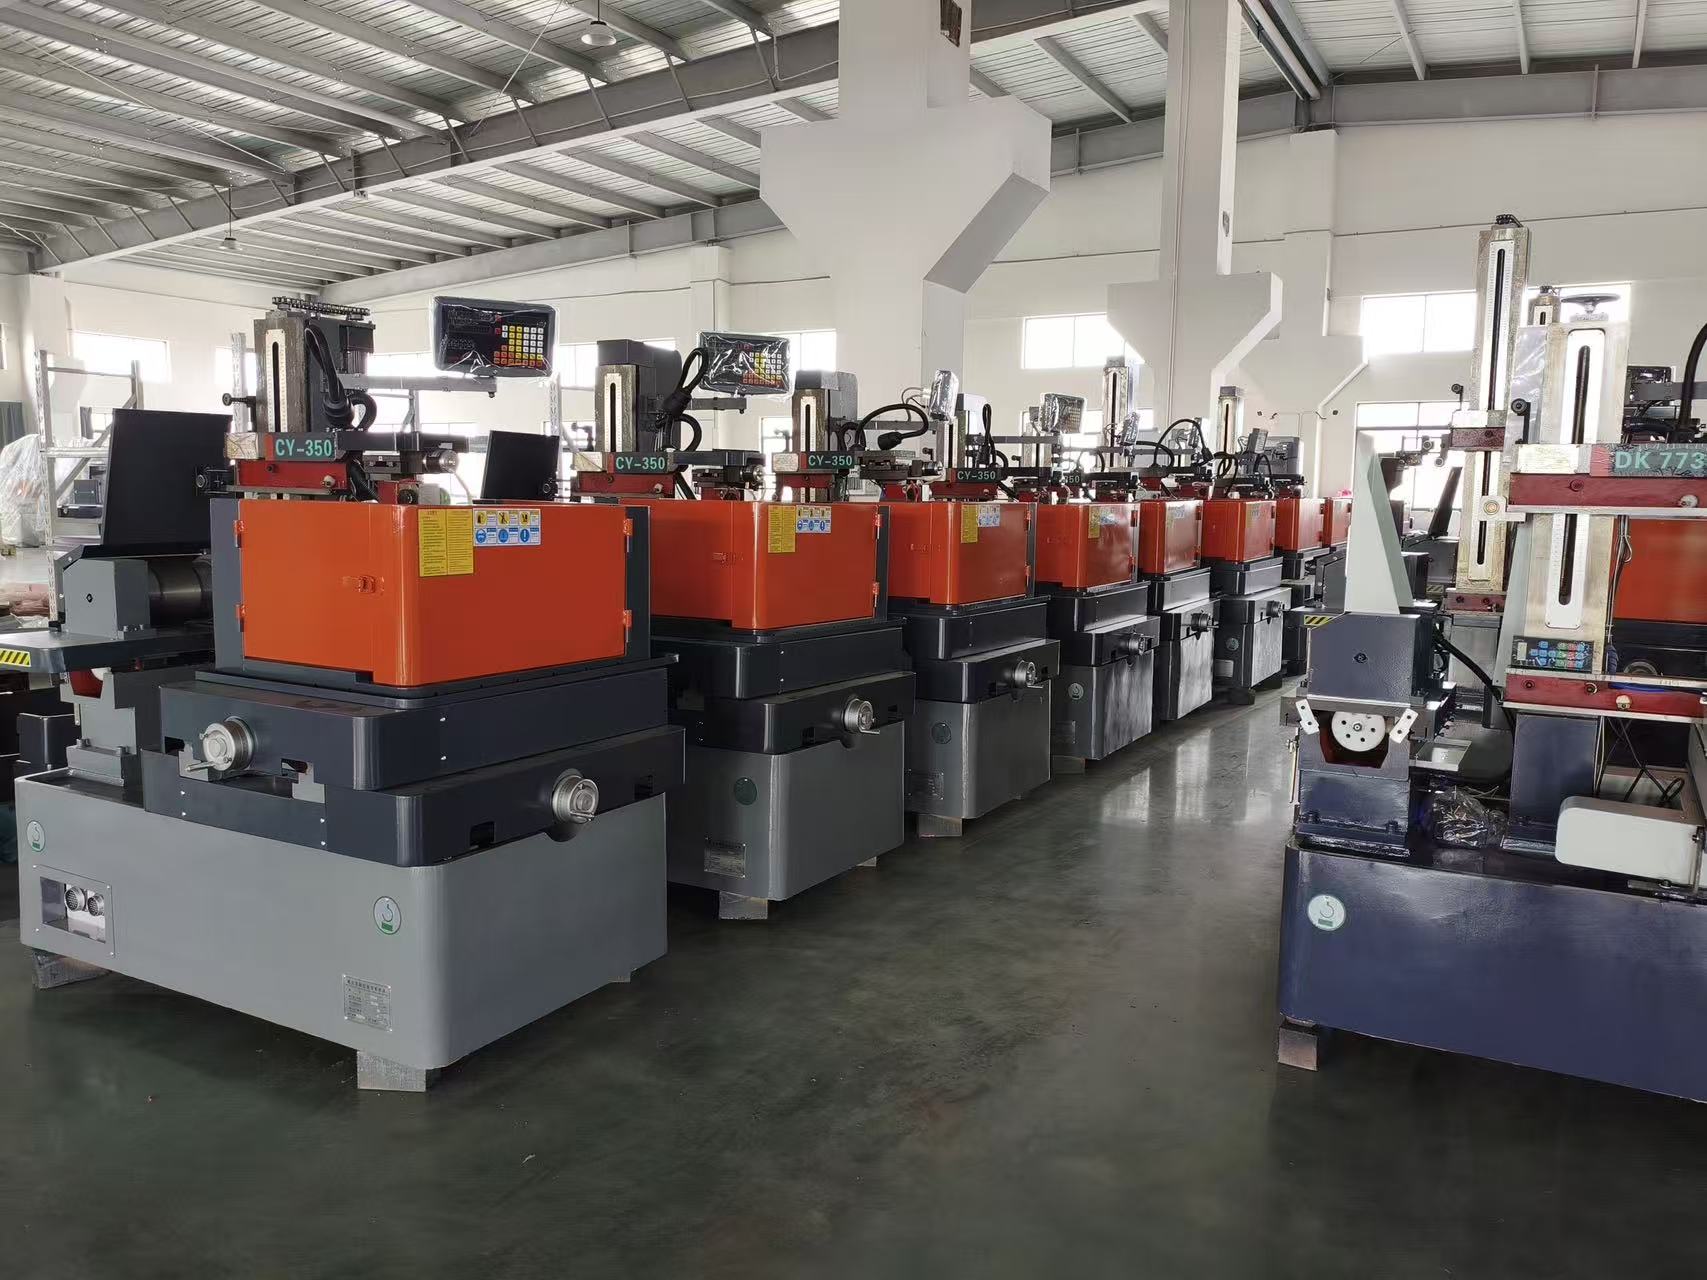
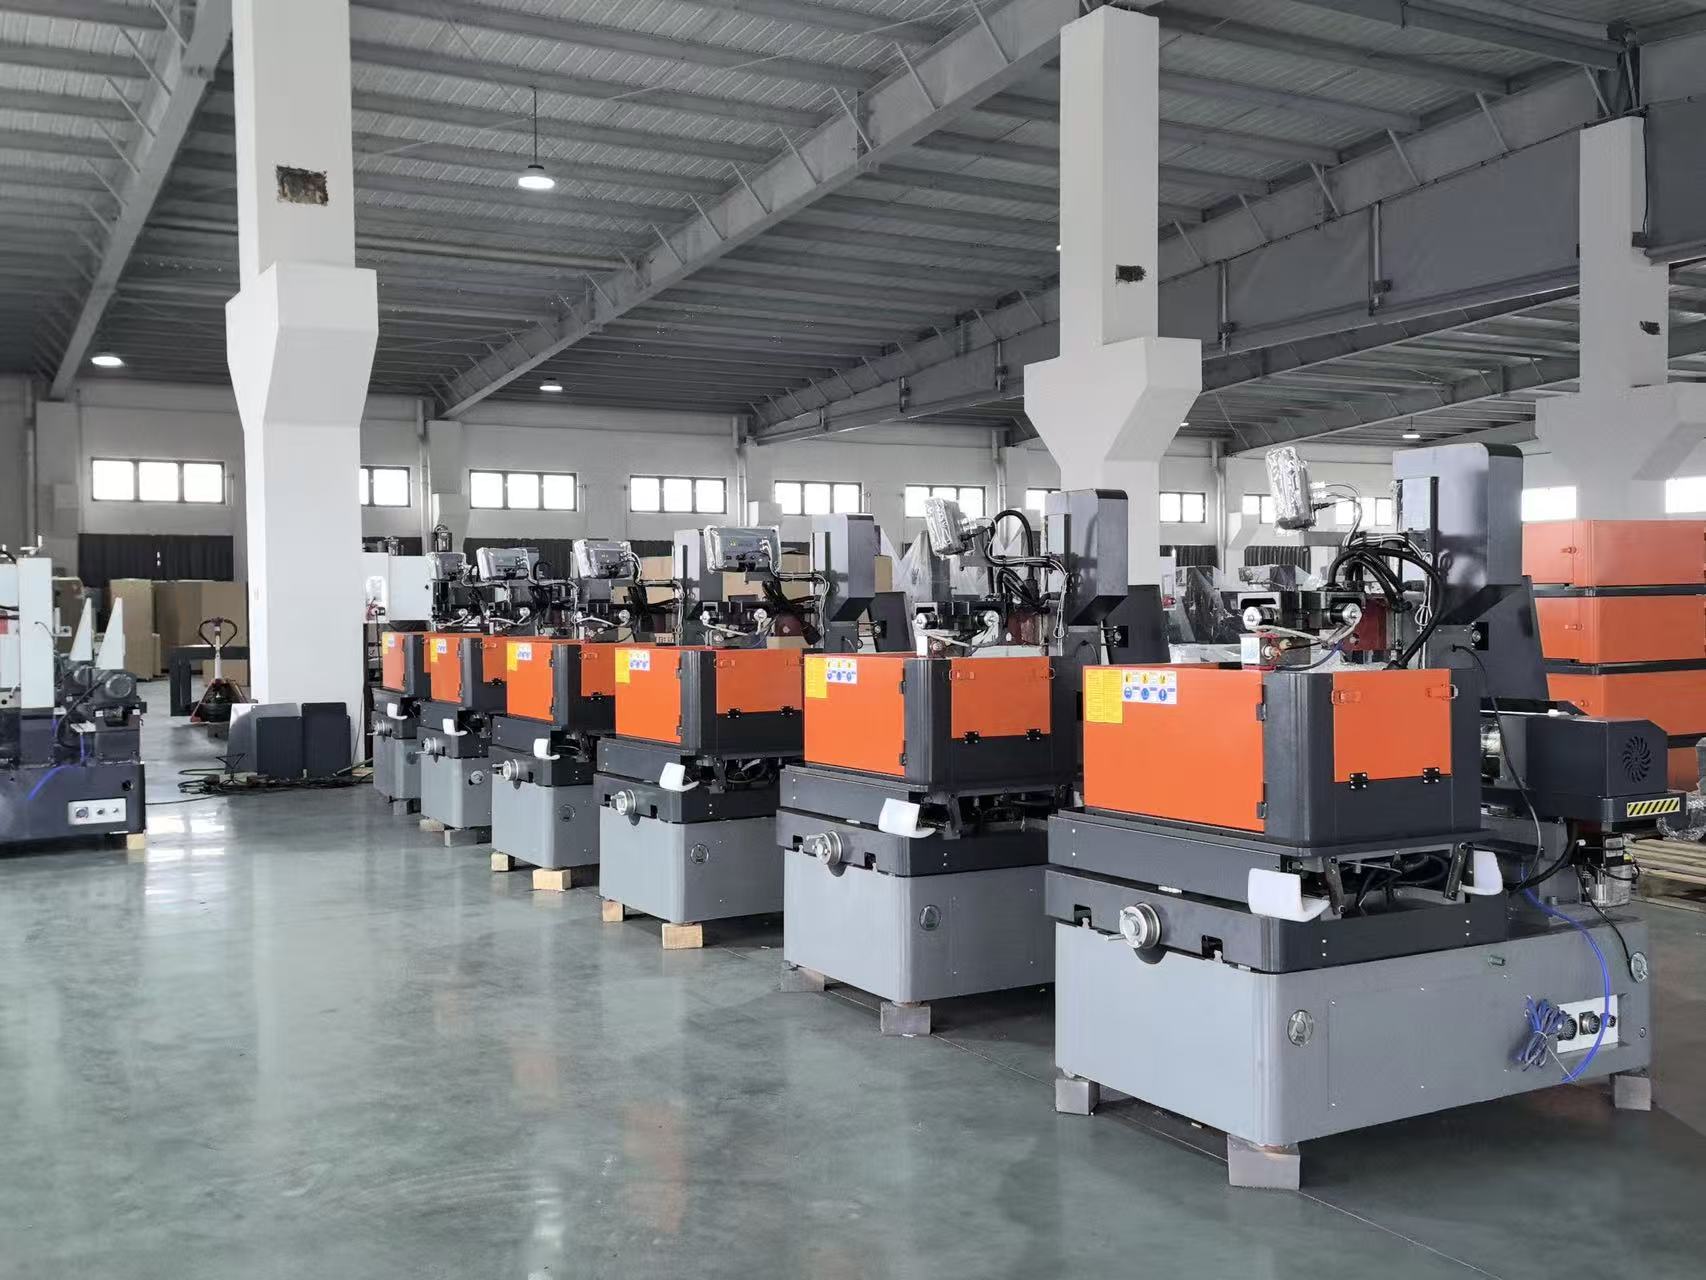
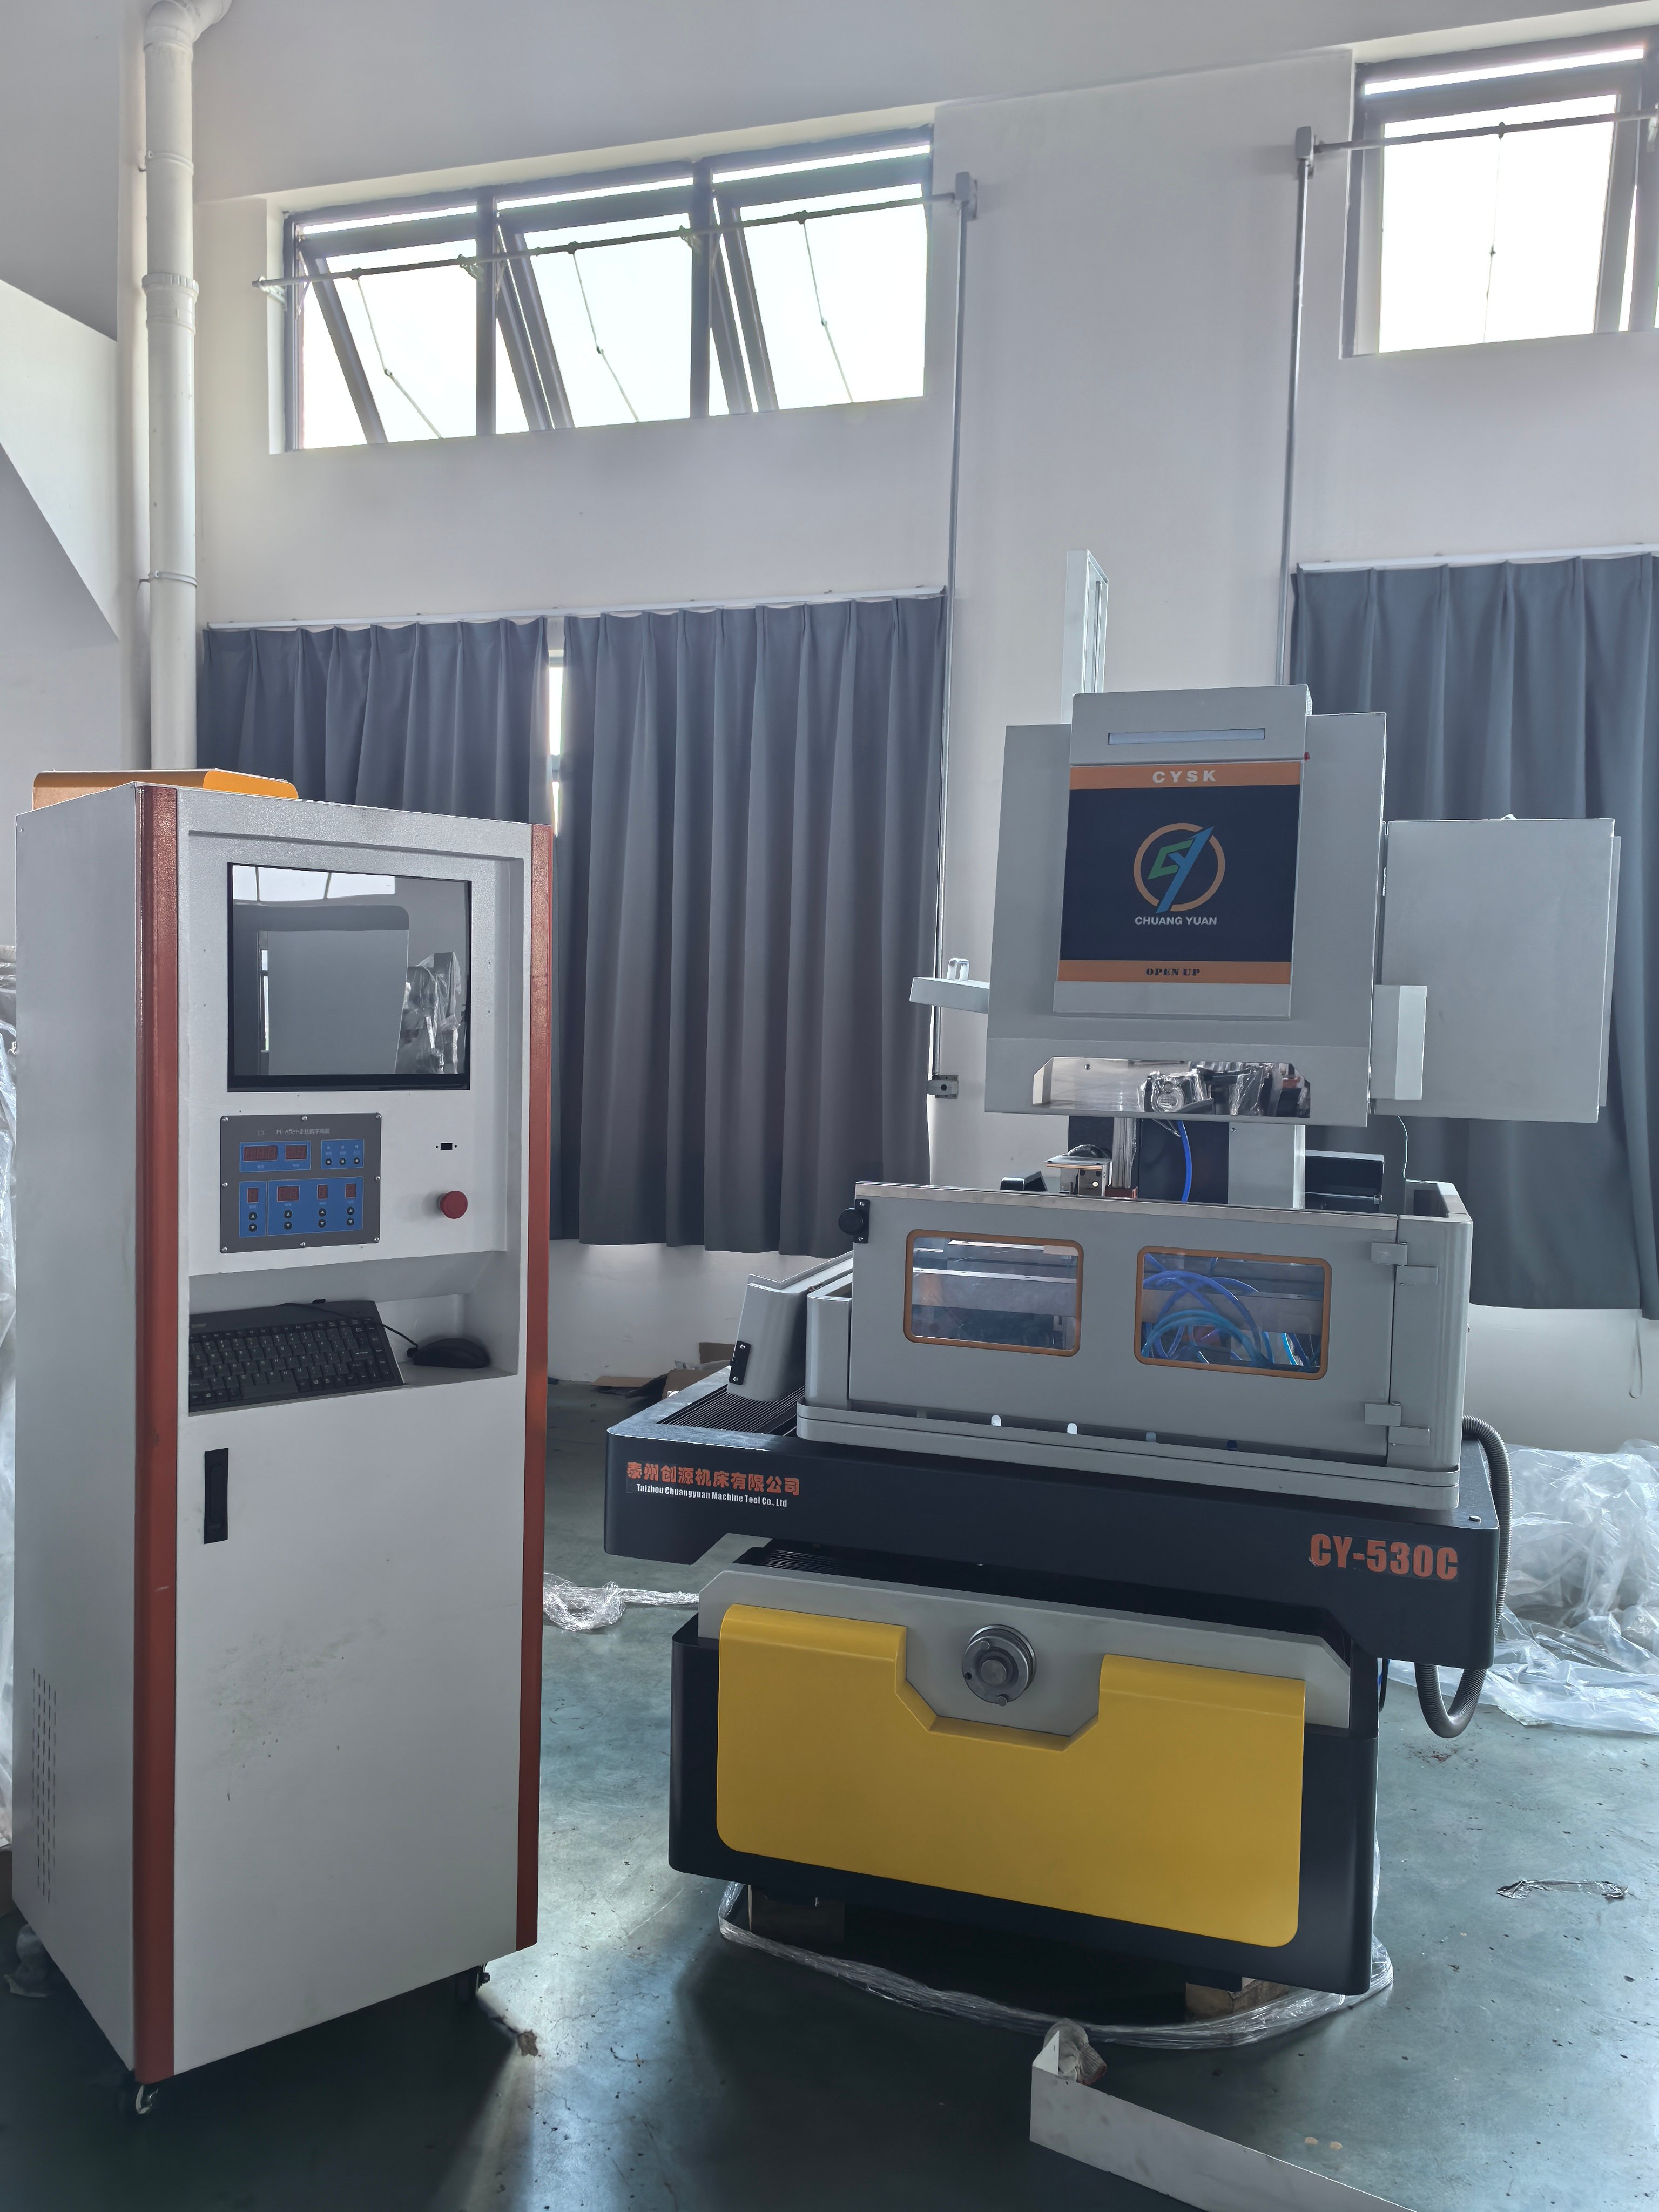
Wire Erosion EDM, also known as wire electrical discharge machining, removes material through controlled spark erosion between a continuously moving wire electrode and the workpiece submerged in deionized water. At Taizhou Chuang Yuan Machine Tool Co., Ltd., established in 2003 in Taizhou City, Jiangsu Province, China, we integrate research and development, production, and sales under one roof, which allows us to tune every Wire Erosion EDM platform for real shop-floor conditions rather than laboratory ideals. Our production process begins with finite element analysis of the machine bed, followed by stress-relieved castings that are machined on our own machining centers, hand-scraped, and laser-calibrated. Each Wire Erosion EDM unit undergoes 72 hours of continuous cutting trials before shipment, verifying positioning accuracy of ±0.003 mm, repeatability of ±0.001 mm, and best surface finish of Ra 0.4 µm. We serve more than 20 exporting countries and regions, and our Wire Erosion EDM systems are used daily in mold making, aerospace, medical instruments, automotive tooling, and precision electronics. In mold making, operators typically run multi-pass trimming with 0.25 mm brass wire to achieve mirror-like cavities; in aerospace, titanium and nickel alloys are cut with adaptive pulse control to prevent recast layers. Our generators adjust on-time and off-time in microseconds, maintaining stable cutting even when flushing conditions change. We also provide remote diagnostics through a cloud gateway, allowing our engineers in Jiangsu to review discharge waveforms and axis feedback in real time, often resolving issues without a site visit. Training is structured around task-based modules, and most operators become confident within five days. Because we manufacture the full machine, including the wire transport system, power supply, and control software, spare parts are available quickly and cost-effectively. This vertical integration, combined with strict quality gates, ensures that every Wire Erosion EDM machine we ship supports years of stable, high-accuracy production.

Frequently Asked Questions

What Materials Can Wire Erosion EDM Cut Reliably?

Wire Erosion EDM cuts any electrically conductive material, including hardened tool steel, carbide, titanium, Inconel, copper, and aluminum. Because it is a thermal erosion process, material hardness does not limit cutting; a 62 HRC die insert cuts as easily as mild steel. For carbide and exotic alloys, we recommend multi-pass trimming and adjusted pulse parameters to minimize recast layers. Our application engineers provide starting parameters for more than 400 material grades, so your team can begin productive cutting quickly.
Our Wire Erosion EDM machines hold ±0.003 mm positioning accuracy and ±0.001 mm repeatability under stable thermal conditions. With closed-loop compensation and proper flushing, accuracy remains within 0.006 mm over 300 mm of travel. We verify each machine using laser interferometry and ball-bar tests, and we supply the measurement report with shipment so you can confirm performance before production begins.
Most customers use 0.25 mm brass wire for general mold work, 0.20 mm for fine details, and 0.30 mm for faster roughing. Coated wires improve cutting speed on carbide and thick sections. Our Wire Erosion EDM generators automatically adapt to wire type, and the automatic threading system handles 0.15 mm to 0.35 mm wire, reducing manual intervention and downtime.
We provide remote commissioning, video-guided installation, and on-site support when required. Our cloud diagnostics let engineers review machine data in real time. Training covers setup, programming, maintenance, and troubleshooting, and most operators reach independent operation within five days. Spare parts ship from our Jiangsu facility, and we maintain stock for fast delivery.
Standard Wire Erosion EDM models ship within 30 to 45 days after deposit, depending on configuration. The warranty covers 24 months for major components, with lifetime technical support. We also offer preventive maintenance plans and operator refresher training to keep accuracy and uptime high throughout the machine's service life.

Related Articles

Processing characteristics of EDM wire cutting machine

24

Dec

Processing characteristics of EDM wire cutting machine

View More
How to choose a machining center?

12

Dec

How to choose a machining center?

View More
The correct handling method for insufficient machining accuracy of fast wire cutting machine

13

Dec

The correct handling method for insufficient machining accuracy of fast wire cutting machine

View More
Why modular spring machine supports fast switching of different spring production types

14

Jul

Why modular spring machine supports fast switching of different spring production types

Production Bottlenecks of Traditional Integrated Spring Forming Equipment Modern metal forming manufacturing increasingly features diversified product specifications and mixed batch production. Many production facilities need to process springs ...
View More

Customer Testimonials

Mehmet Aydin, Aerospace Production Manager, Turkey
Accuracy That Won Us New Aerospace Work

Our Wire Erosion EDM from Chuang Yuan held 0.006 mm on Inconel blade roots, cutting scrap from 7% to 1.5% in one quarter. Delivery performance rose to 97%, and we secured a new engine component order. The remote diagnostics saved us two service trips in the first year, which kept our schedule intact.

Carlos Mendoza, Tooling Supervisor, Mexico
Faster Cutting and Fewer Wire Breaks

We cut 12 mm brass and carbide punches daily. Since installing their Wire Erosion EDM, speed increased from 140 to 180 mm²/min, wire breaks dropped 70%, and output per shift rose 25%. Tooling cost per part fell 18%, and we now support three assembly lines without adding a second shift.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
In-House Manufacturing Ensures Wire Erosion EDM Quality and Fast Delivery

In-House Manufacturing Ensures Wire Erosion EDM Quality and Fast Delivery

Because Taizhou Chuang Yuan Machine Tool Co., Ltd. manufactures Wire Erosion EDM machines in our own facility, we control every stage from casting to final calibration. This vertical integration means we can hold ±0.003 mm accuracy consistently and ship standard models in 30 to 45 days. It also lets us customize stroke, wire diameter range, and generator settings for specific industries such as mold making, aerospace, and medical instruments. Customers in more than 20 exporting countries benefit from faster spare parts availability and lower long-term ownership costs. In practice, a German mold shop received a customized Wire Erosion EDM with extended Z-axis travel and reduced their insert lead time by 40% within six weeks. When every component is made and tested under one roof, quality is not left to chance.
Advanced Pulse Control Delivers Stable Wire Erosion EDM Performance

Advanced Pulse Control Delivers Stable Wire Erosion EDM Performance

Our Wire Erosion EDM generators adjust on-time, off-time, and peak current in microseconds, maintaining stable cutting even when flushing conditions change. This adaptive control reduces wire breakage by up to 70% and supports high-speed cutting at 180 mm²/min on 12 mm brass. For aerospace alloys like Inconel 718, it minimizes recast layers and holds 0.006 mm accuracy over 300 mm travel. Operators appreciate that the control software recommends parameters for more than 400 materials, shortening setup time and reducing reliance on highly experienced staff. A Turkish aerospace subcontractor used this capability to cut blade root scrap from 7% to 1.5%, directly improving their competitiveness on European engine component contracts.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop