Precision CNC Turning Machines | 0.002mm Roundness & Ra 0.4

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Precision CNC Turning Solutions Built For Global Manufacturers By Taizhou Chuang Yuan

Precision CNC Turning Solutions Built For Global Manufacturers By Taizhou Chuang Yuan

Taizhou Chuang Yuan Machine Tool Co., Ltd. has specialized in Precision CNC Turning equipment and deep hole processing machinery since 2003 from Taizhou City, Jiangsu Province, China, serving automotive, aerospace, hydraulic, medical, and energy buyers in more than 20 exporting countries. Our Precision CNC Turning platforms hold roundness within 0.002 mm, surface finish down to Ra 0.4, and repeat positioning accuracy of plus or minus 0.005 mm across batch runs, which is essential for hydraulic valve bodies, fuel injector sleeves, medical bone screws, and aerospace actuator pins where the bore-to-OD concentricity governs sealing and fatigue life. In a typical automotive tier-one program, a client replaced two older lathes with our deep hole Precision CNC Turning system and cut cycle time by 23 percent while reducing scrap from 4.1 to 0.8 percent within one quarter, saving roughly USD 61,000 annually.
Get A Quote

Case Study

Reducing Hydraulic Cylinder Bore Scrap For A German Fluid Power Maker

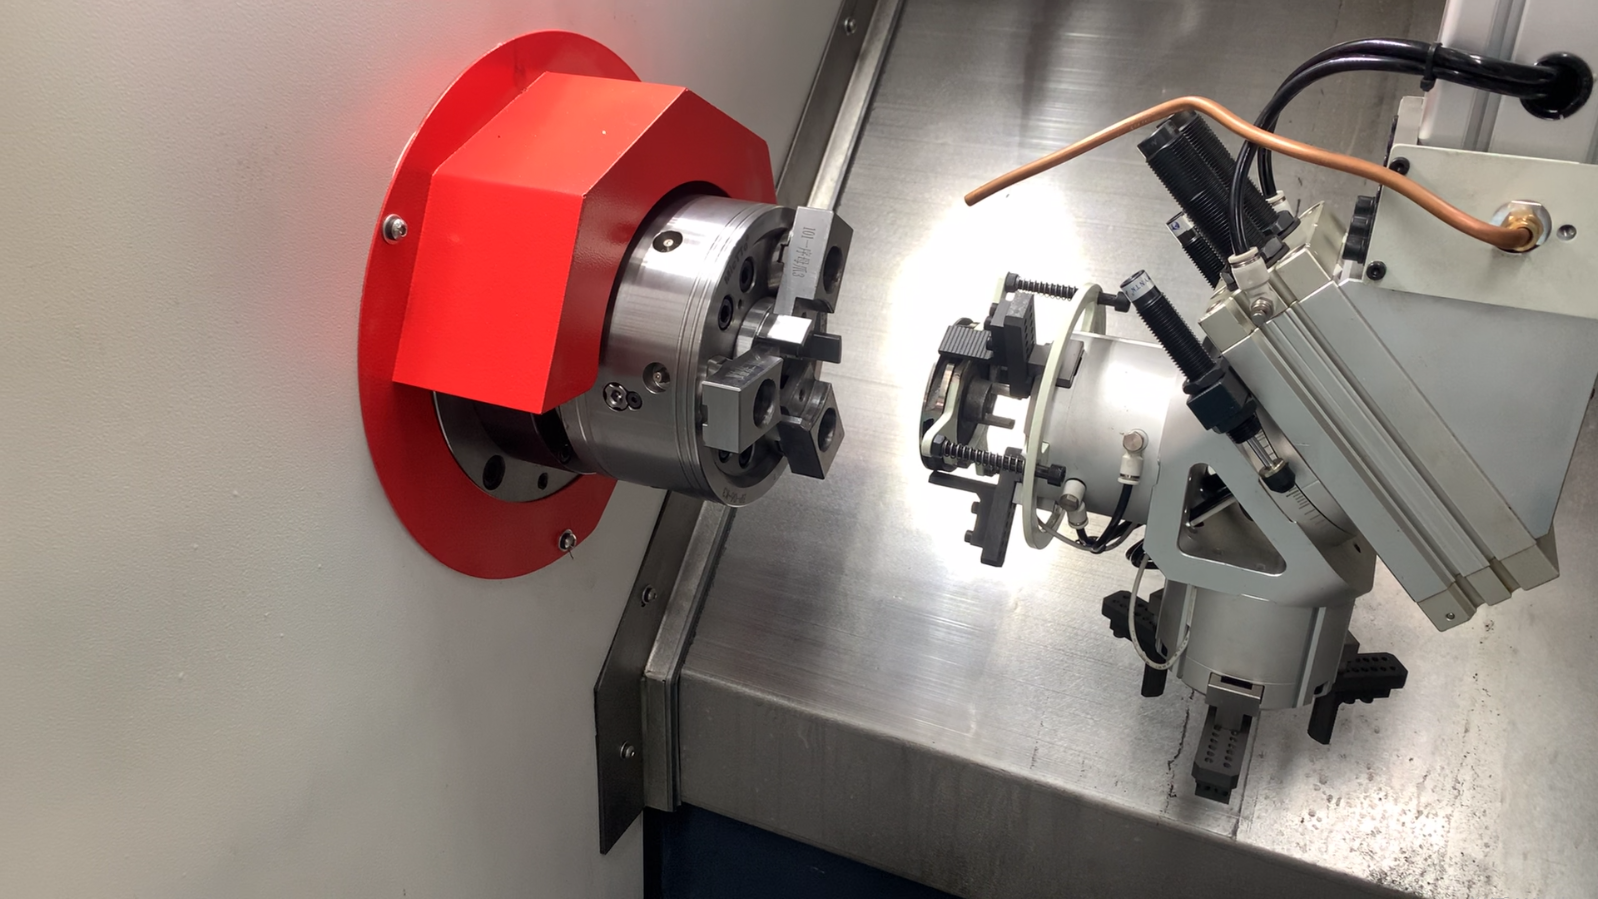
A German fluid power maker faced 5.6% scrap due to chatter and taper when machining 140 mm deep bores in 27MnCr steel. We integrated a deep hole Precision CNC Turning system featuring high-pressure through-coolant, a damped boring bar, and synchronized servo feeds. Roundness reached 0.003 mm, taper stayed under 0.01 mm, and scrap dropped to 0.9%, cutting cycle times by 19% across 12,000 monthly units.

Cutting Cycle Time For A Medical Bone Screw Producer In The United States

A US medical device manufacturer required burr-free titanium bone screws with mirror finishes under strict FDA traceability. Our Precision CNC Turning cell utilized a 12-station live tool turret, sub-spindle pickoff, and Ra 0.4 finishing inserts with probing. Cycle time dropped from 96 to 71 seconds, dimensional Cpk exceeded 1.67, and rework plummeted by 82%, enabling monthly output to scale to 150,000 units.

Improving Fuel Injector Sleeve Precision For A Turkish Automotive Supplier

A Turkish automotive supplier suffered concentricity drift on stainless steel fuel injector sleeves, leading to high field return rates. We supplied a Precision CNC Turning cell featuring automated thermal compensation and in-process wear offsets. Concentricity stabilized at 0.004 mm and wall thickness variation dropped to 0.006 mm, reducing field returns by 74% across 2.4 million annual sleeves.

Related products

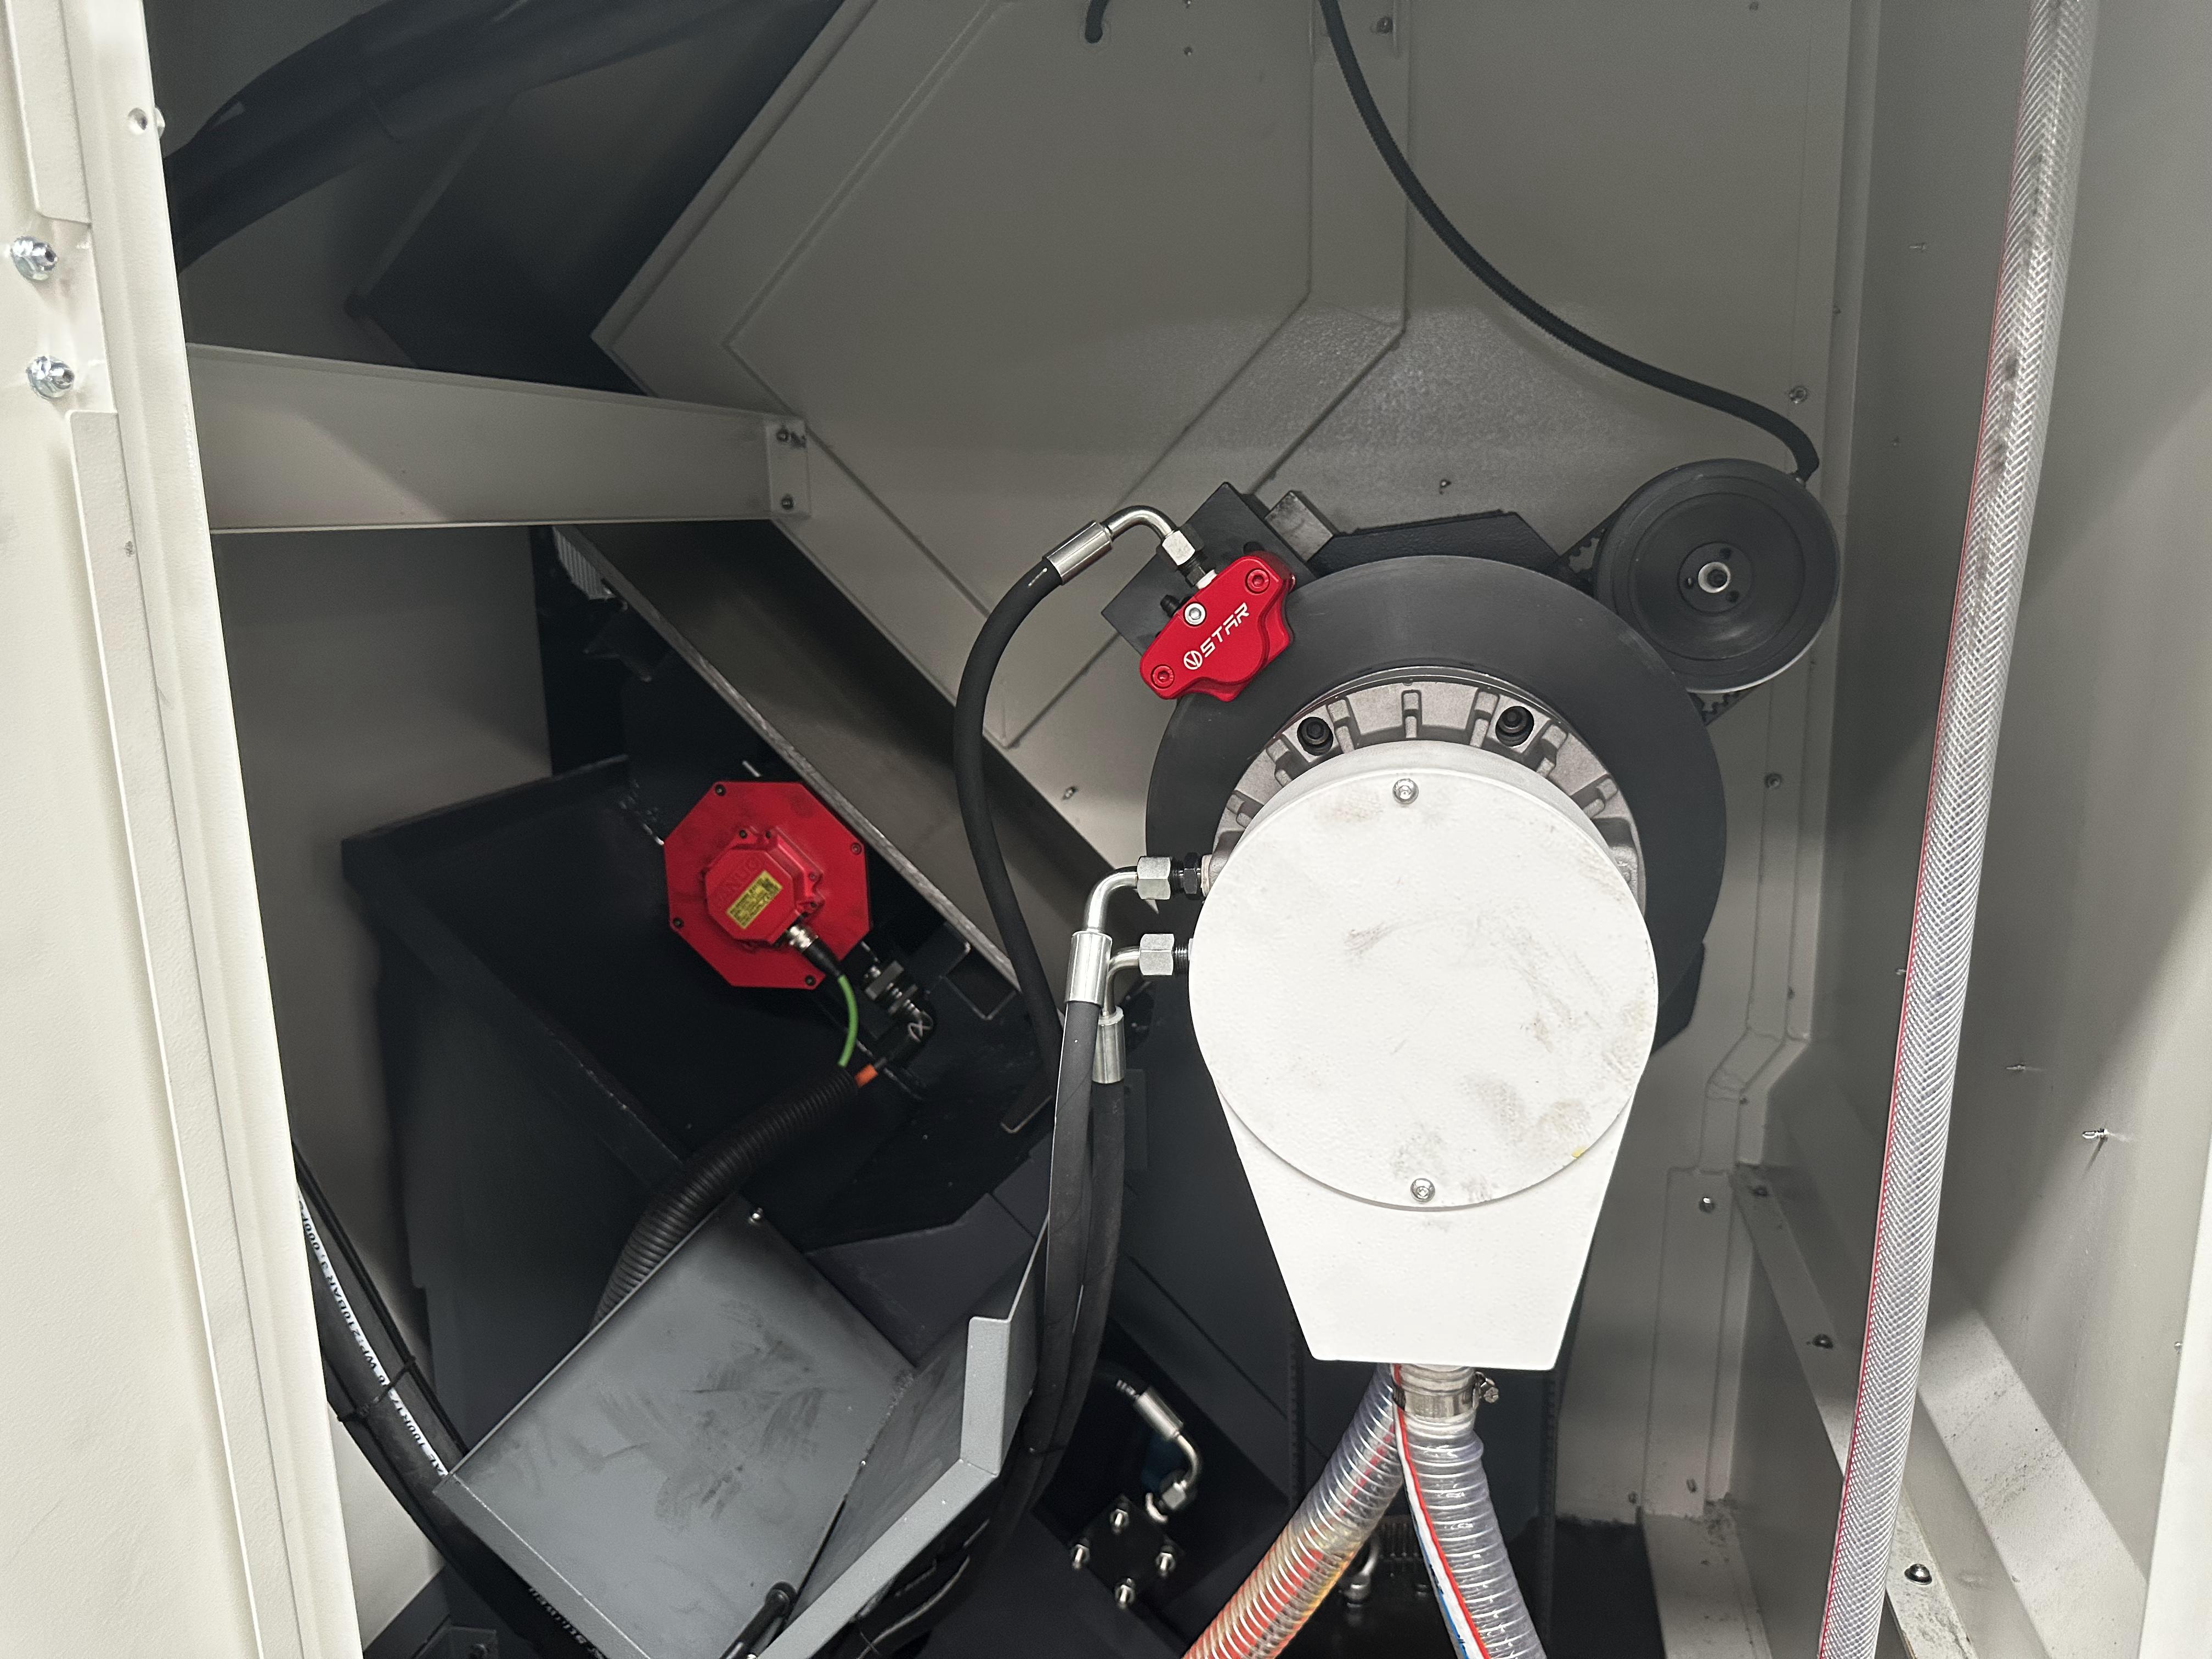
Precision CNC Turning sits at the core of modern metal cutting because it controls roundness, concentricity, and surface integrity in one continuous cycle. Taizhou Chuang Yuan Machine Tool Co., Ltd. builds this capability from the ground up, beginning with finite element analysis of bed and column castings that are aged and machined in-house to damp vibration during heavy interrupted cuts. Spindle assemblies are preloaded and dynamically balanced, then mated to high-resolution servo drives and absolute encoders so every tool path repeats within 0.005 mm. On deep hole models, counter-rotation between workpiece and tool, high-pressure coolant up to 70 bar, and intelligent feed control remove chips reliably even at length-to-diameter ratios beyond 20 to 1, a critical requirement for hydraulic manifolds, gun barrels, and landing gear pins. Every machine passes laser interferometer accuracy verification, ballbar circularity testing, and a 72-hour continuous cutting trial before packing. In production, a German fluid power client achieved 0.003 mm roundness on 140 mm bores after switching to our deep hole Precision CNC Turning platform, while a Turkish automotive supplier held 0.004 mm concentricity on fuel injector sleeves and cut field returns by 74 percent. A US medical device maker reduced bone screw cycle time from 96 to 71 seconds and lifted Cpk above 1.67. These outcomes come from disciplined process engineering: 300-piece capability studies, tool-life mapping, thermal drift compensation, and operator dashboards that surface wear trends before tolerances drift. Our engineering team supports English speaking customers through remote diagnostics, video commissioning, and documented preventive maintenance schedules, while spare parts ship within 48 hours. CE-aligned electrical design, multi-voltage transformers, and localized documentation ease installation across Asia, Europe, the Americas, and the Middle East. Because we control casting, machining, assembly, and testing under one roof, we can tailor stroke, spindle bore, chucking, chip conveyor, and automation interfaces to specific part families instead of forcing customers to adapt. That flexibility shortens commissioning from months to weeks and keeps total cost per part predictable. With more than 20 years of export experience and long-term partnerships in over 20 countries, we help manufacturers turn demanding geometries into stable, profitable production.

Frequently Asked Questions

What tolerances can Precision CNC Turning realistically hold in daily production?

On properly maintained machines with stable temperature control, Precision CNC Turning routinely holds plus or minus 0.005 mm on diameter and 0.003 mm roundness. Surface finishes reach Ra 0.4 with fine boring or finishing inserts. We verify capability with a 300-piece study so you know the real Cpk before shipment, not just a specification sheet.
Hydraulic and pneumatic components, automotive fuel systems, medical implants and instruments, aerospace actuators, oil and gas fittings, and mold making. These sectors need long bores, tight concentricity, and mirror finishes. More than 20 exporting countries already run our equipment in these applications with documented results.
We combine aged castings, damped boring bars, counter-rotation, high-pressure through-coolant, and thermal compensation in the CNC. Tool wear offsets update automatically. In a German hydraulic program, taper stayed below 0.01 mm across 140 mm bores and scrap fell from 5.6 to 0.9 percent.
English-language installation guidance, remote diagnostics, video commissioning, operator training, and preventive maintenance templates are standard. Spare parts dispatch within 48 hours, and engineers respond within one business day. This keeps uptime above 96 percent for most export customers.

Related Articles

How to choose a machining center?

12

Dec

How to choose a machining center?

View More
The correct handling method for insufficient machining accuracy of fast wire cutting machine

13

Dec

The correct handling method for insufficient machining accuracy of fast wire cutting machine

View More
How to reduce drill bit wear during continuous deep hole machine processing tasks

03

Aug

How to reduce drill bit wear during continuous deep hole machine processing tasks

Understanding the Mechanics of Deep Hole Thermal Stress Executing continuous boring and high-depth machining tasks on industrial production lines presents severe thermal and mechanical challenges that routinely test the limits of cutting tooling. W...
View More
What export quality standards international clients require for wire cutting machine products

03

Aug

What export quality standards international clients require for wire cutting machine products

Understanding International Export Compliance in Precision Machining Navigating the complex landscape of global industrial trade requires a thorough understanding of the stringent technical benchmarks that overseas buyers mandate for advanced metal...
View More

Customer Testimonials

Klaus Reinhardt
Scrap Rate Cut By More Than Half On Deep Bores

We run 27MnCr hydraulic cylinders with 140 mm bores. After installing the deep hole Precision CNC Turning system, roundness improved to 0.003 mm and scrap dropped from 5.6 to 0.9 percent. Cycle time fell 19 percent and two more lines now run on the same platform. Support response has been fast and technically solid.

Emily Carter
Med Device Cpk Above 1.67 And Clean Validation

Our titanium bone screws needed burr-free threads and mirror finishes. The 12-station live tool Precision CNC Turning cell cut cycle time from 96 to 71 seconds, raised Cpk above 1.67, and reduced rework by 82 percent. We passed FDA process validation first time and scaled output fourfold.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Deep Hole Precision CNC Turning That Holds 0.003 mm Roundness At High Volume

Deep Hole Precision CNC Turning That Holds 0.003 mm Roundness At High Volume

For hydraulic, aerospace, and oil and gas parts, bore quality decides sealing, fatigue life, and leak rate. Our deep hole Precision CNC Turning platform pairs counter-rotation, damped boring bars, and 70 bar through-coolant with servo feed synchronized to spindle speed, so chips evacuate instead of scratching the bore. Aging and in-house machining of castings suppress vibration, while absolute encoders and thermal compensation keep size stable through long shifts. In a German fluid power plant, 140 mm bores in 27MnCr steel held 0.003 mm roundness and taper under 0.01 mm, cutting scrap from 5.6 to 0.9 percent and saving about USD 61,000 per year. Each machine is verified with laser interferometry, ballbar testing, and a 72-hour cutting trial plus a 300-piece capability study. Buyers receive English documentation, remote diagnostics, and spare parts within 48 hours, keeping uptime above 96 percent.
Complete Precision CNC Turning Cells That Shorten Prototype To Production

Complete Precision CNC Turning Cells That Shorten Prototype To Production

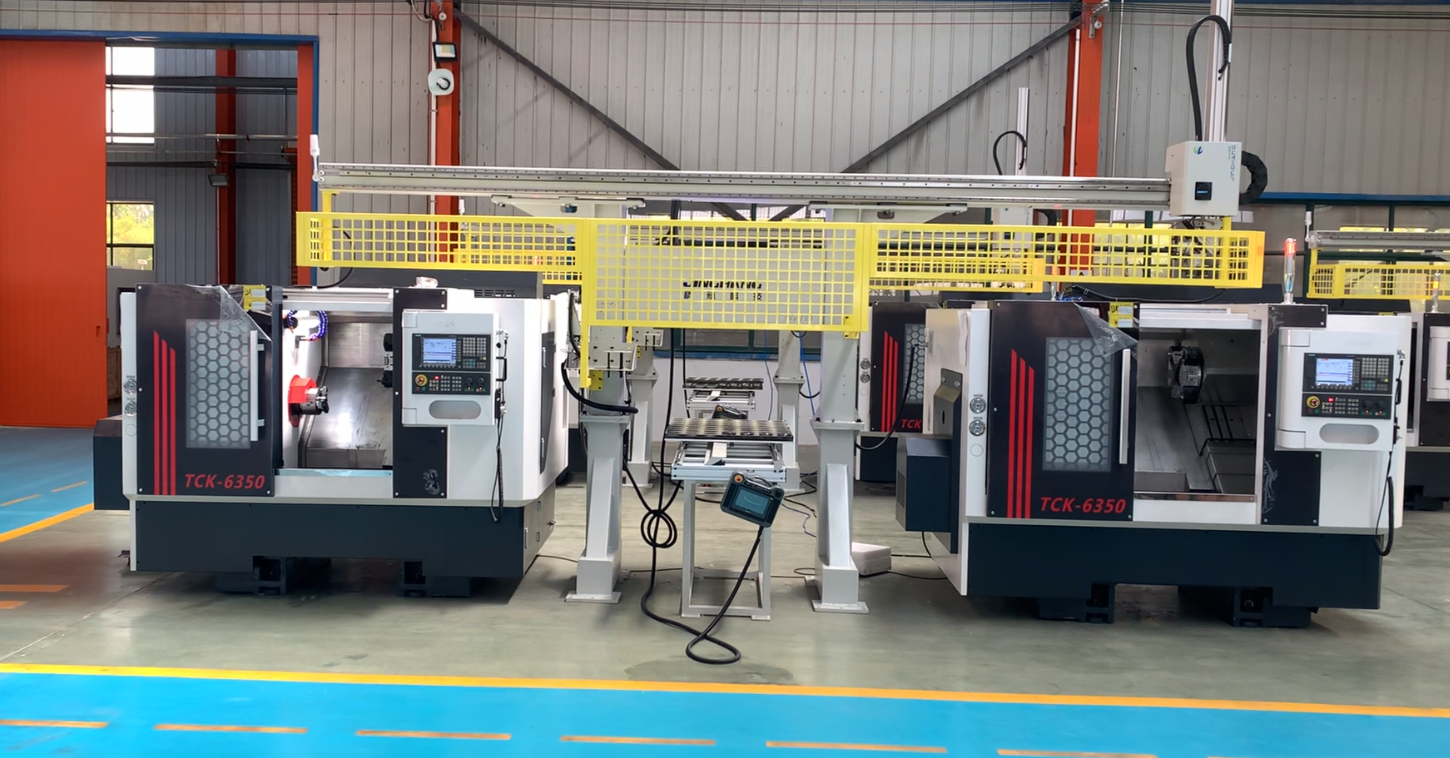
Getting from sample approval to stable output is where most projects lose money. We deliver complete Precision CNC Turning cells including bar feeders, sub-spindle pickoff, live tooling, in-process probing, and chip management, matched to your part family. Engineering reviews cycle time, tool life, and fixturing before build, then proves the process with capability studies and tool-wear mapping. A US medical device maker moved from 96 to 71 seconds per titanium bone screw, lifted Cpk above 1.67, and cut rework by 82 percent, passing FDA validation on the first audit. A Turkish automotive supplier reached 0.004 mm concentricity on stainless fuel injector sleeves and reduced field returns by 74 percent while scaling to 2.4 million units per year. Multi-voltage, CE-aligned electrical design and localized documentation simplify installation in over 20 exporting countries. With in-house casting, machining, assembly, and testing, customization takes weeks, not months.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop