Metal Lathe Tooling: Precision Tool Holders & Inserts for CNC Lathes

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Precision Metal Lathe Tooling Engineered for Global Manufacturers

Precision Metal Lathe Tooling Engineered for Global Manufacturers

Taizhou Chuang Yuan Machine Tool Co., Ltd. has manufactured precision metal lathe tooling since 2003, integrating research, development, production and sales in Taizhou City, Jiangsu Province, China. Our metal lathe tooling covers tool holders, boring bars, turning inserts, chucks, live centers, turret tool posts and deep hole tooling, all hardened and ground to tolerances within 0.005 mm so that batch turning stays repeatable. In automotive transmission plants, our tooling ran 1,200 hours between regrinds on hardened steel shafts, cutting tool change downtime by 28 percent for a German client. In oil and gas valve machining, clients use our deep hole tooling to hold IT7 accuracy on bores up to 3,000 mm, while pipe and tube producers rely on our tooling on slitting and cut to length lines running 24 hours per day. Every set is inspected with CMM and laser interferometry, packed for sea freight, and supported by multilingual documentation.
Get A Quote

Case Study

Metal Lathe Tooling Cuts Shaft Cycle Time 22 Percent for German Auto Supplier

A German automotive supplier turning hardened transmission shafts struggled with chipping inserts and 3.2 micron surface drift. We supplied coated carbide inserts, hardened tool holders and a precision turret tool post system. Cutting speed rose from 180 to 240 m per minute, cycle time fell 22 percent, and tool life reached 1,150 parts per edge. The line now runs three shifts with online tool wear monitoring and 18 months of zero rejection claims.

Deep Hole Metal Lathe Tooling Holds IT7 on 3,000 mm Oil Valve Bores

An oil and gas valve maker needed straight, round bores in forged stainless. Using our deep hole tooling with guided boring bars, we controlled runout to 0.01 mm and surface finish to Ra 0.4 over 3,000 mm. Scrap dropped from 6 percent to 0.8 percent, and annual savings passed USD 210,000 while delivery moved from 30 to 16 days.

Pipe Line Metal Lathe Tooling Increases Output 31 Percent in Turkey

A Turkish pipe producer ran slitting and cut to length lines with unstable centering. Our custom chuck jaws and live centers stabilized clamping at 1,500 rpm, lifting line output 31 percent and reducing setup time from 55 to 22 minutes. The plant now ships 4,200 tons monthly with tooling service every 900 hours. Products Title: Explore Our Complete Metal Lathe Tooling Range

Related products

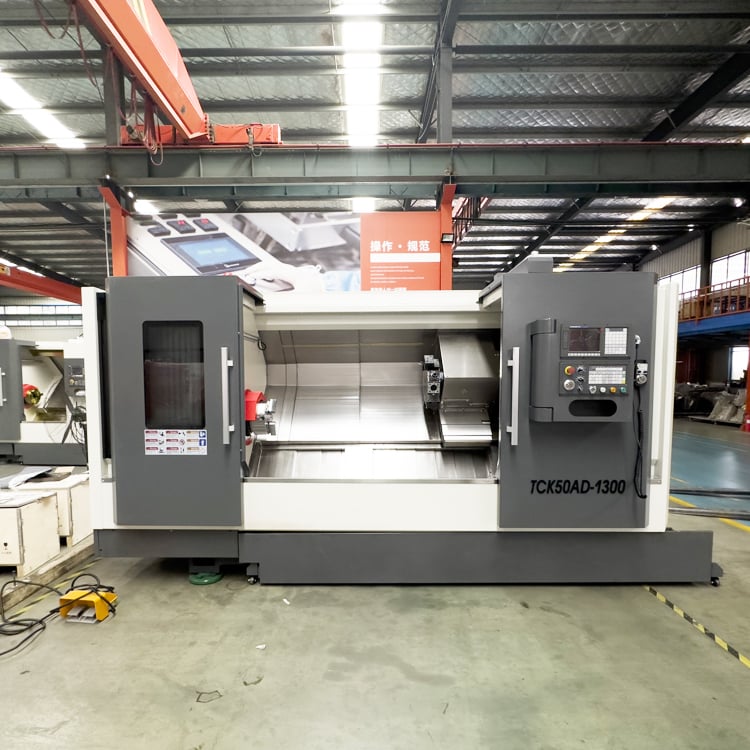
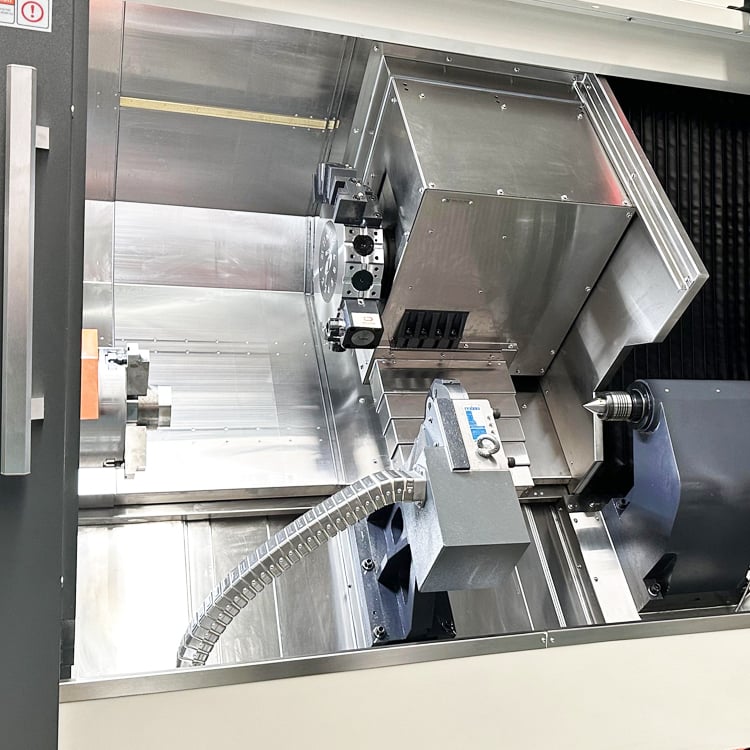
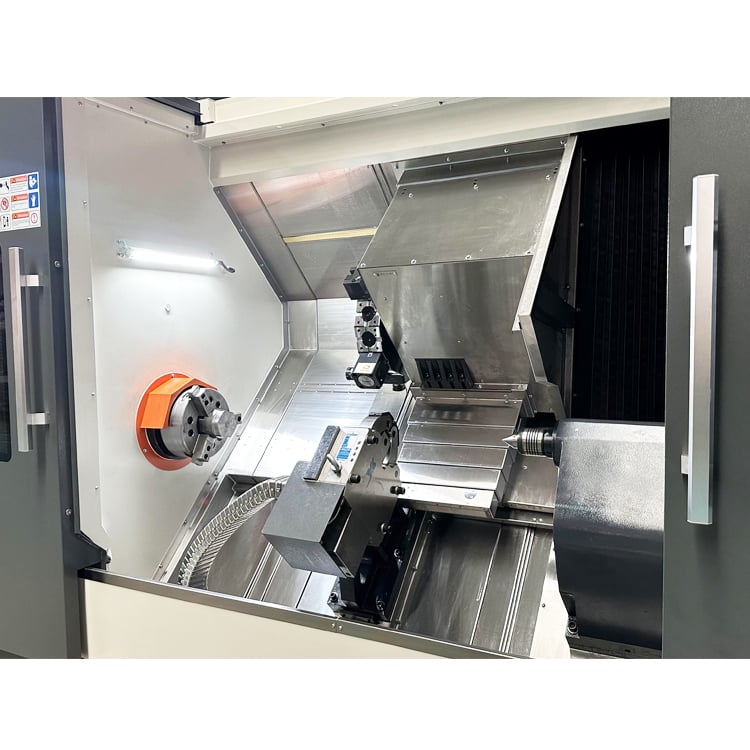
Metal lathe tooling is the interface between a machine spindle and the workpiece, so its accuracy decides the accuracy of every finished part. Taizhou Chuang Yuan Machine Tool Co., Ltd. approaches this from a manufacturing base established in 2003 in Taizhou City, Jiangsu Province, China, where research, development, production and sales operate under one roof. Our metal lathe tooling program begins with material selection: alloy steel forgings are normalized, roughed, heat treated to 58 to 62 HRC, then finish ground on CNC grinders. Tool holders, boring bars, chucks, live centers and turret tool posts pass CMM inspection and laser interferometry, with runout controlled within 0.005 mm and repeatability within 0.003 mm so that automated turning cells stay stable across long shifts. Turning inserts are matched by grade, coating and chip breaker to the work material, from P grades for steel to K grades for cast iron and M grades for stainless, which keeps surface finish between Ra 0.4 and Ra 1.6 in production. Deep hole processing tooling extends our reach to bores up to 3,000 mm at IT7, serving hydraulic cylinders, oil and gas valves and gun drilling shops. Because we also build lathes, EDM machines, machining centers, pipe making machines, slitting lines, cut to length lines and deep hole machines, our engineers understand the whole cutting loop, not just one accessory. That system view lets us tune tooling for specific habits: job shops in North America prefer quick change holders and standard inserts for short runs, European transmission plants want documented tool life and process capability studies, and Asian pipe mills need durable clamping for continuous tube production. Globally, our metal lathe tooling supports more than 20 exporting countries and regions, and we validate every new configuration on customer samples before shipment. Documentation covers material certificates, hardness reports and inspection data, packed for sea freight and supported in English, Russian, Spanish and Arabic. This is how our metal lathe tooling reduces cost per part, protects machine uptime and helps partners grow their local industrial markets.

Frequently Asked Questions

How do I choose Metal Lathe Tooling for hardened steel turning?

Match the insert grade and coating to the hardness and speed. For steel above 45 HRC, use a tough substrate with TiAlN coating, a negative rake holder and rigid clamping. We test on your sample and confirm cutting data, typically 180 to 260 m per minute, so you get stable tool life before volume production.
Standard holders and centers are ground within 0.005 mm runout and 0.003 mm repeatability. In production, clients hold IT7 on bores and Ra 0.4 finish. We supply inspection reports with every batch.
Yes. We provide guided boring bars, deep hole tooling for bores up to 3,000 mm, and chucks and live centers for pipe slitting and cut to length lines. Custom jaws and lengths are available.
Orders ship to more than 20 countries, usually within 25 to 35 days. We provide drawings, cutting parameters, replacement schedules and remote commissioning support.

Related Articles

The correct handling method for insufficient machining accuracy of fast wire cutting machine

13

Dec

The correct handling method for insufficient machining accuracy of fast wire cutting machine

View More
What after sales service should reliable edm drilling machine suppliers provide

14

Jul

What after sales service should reliable edm drilling machine suppliers provide

The Evolution of Flexible Manufacturing Through Modular Architecture Modern industrial landscapes demand a high degree of adaptability, where the ability to transition production configurations quickly defines a facility’s operational rhythm....
View More
How to customize spring machine mold fixtures for special shaped spring production

03

Aug

How to customize spring machine mold fixtures for special shaped spring production

Mastering Complex Spring Production Challenges Navigating the intricacies of high-speed industrial manufacturing demands a profound understanding of wire feed dynamics, mechanical tolerances, and multi-axis bending mechanics across modern automated...
View More
Why multi functional edm machine meets mixed mold and part production factory demands

14

Aug

Why multi functional edm machine meets mixed mold and part production factory demands

Navigating the Complexities of High-Mix Manufacturing Environments Running a modern industrial production plant often feels like juggling a dozen spinning plates at once, especially when dealing with high-mix, low-volume manufacturing schedules. Pl...
View More

Customer Testimonials

Michael Braun
Reliable Metal Lathe Tooling Raised Our Output

We installed their holders, inserts and deep hole tooling on our valve line. Bores now hold IT7 at 3,000 mm and scrap fell from 6 percent to 0.8 percent. Quotations are fast and shipments match the schedule, which keeps our contracts secure.

Emre Yilmaz
Accurate Metal Lathe Tooling for Pipe Production

Their chuck jaws and live centers stabilized our slitting line at 1,500 rpm. Output increased 31 percent and setup time dropped from 55 to 22 minutes. Their team understands pipe production habits, not just catalog numbers.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Hardened, Ground and Inspected Metal Lathe Tooling

Hardened, Ground and Inspected Metal Lathe Tooling

Every metal lathe tooling item is forged, normalized, heat treated to 58 to 62 HRC and finish ground on CNC machines. CMM and laser interferometry verify runout within 0.005 mm and repeatability within 0.003 mm. This matters in aerospace and hydraulic shops where one oversized bore scraps a finished casting. In an oil and gas valve plant, our guided boring bars held IT7 across 3,000 mm bores and cut scrap from 6 percent to 0.8 percent, saving more than USD 210,000 a year. Clients in Europe and North America receive hardness and inspection reports with each batch, so quality is documented before the tooling reaches the spindle. That discipline also shortens commissioning, because the tooling arrives ready to cut, not ready to adjust.
Application Matched Grades and Geometry for Global Machining Habits

Application Matched Grades and Geometry for Global Machining Habits

We match insert grades, coatings and chip breakers to your material and machine culture. North American job shops get quick change holders and standard inserts for short runs; European transmission plants receive documented tool life and capability data; Asian pipe mills get reinforced clamping for continuous operation. In a German automotive plant, this matching lifted cutting speed from 180 to 240 m per minute, cut cycle time 22 percent and delivered 1,150 parts per edge. For a Turkish pipe producer, custom jaws and live centers raised line output 31 percent and reduced setup time from 55 to 22 minutes. Because we also build lathes, EDM machines and deep hole machines, our engineers see the whole cutting loop and tune metal lathe tooling to real production habits, not catalog assumptions.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop