Deep Hole Drilling Machine: 42% Faster Cycles, Ra 0.6 Finish

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Deep Hole Drilling Machine Advantages Built on Two Decades of Precision Manufacturing

Deep Hole Drilling Machine Advantages Built on Two Decades of Precision Manufacturing

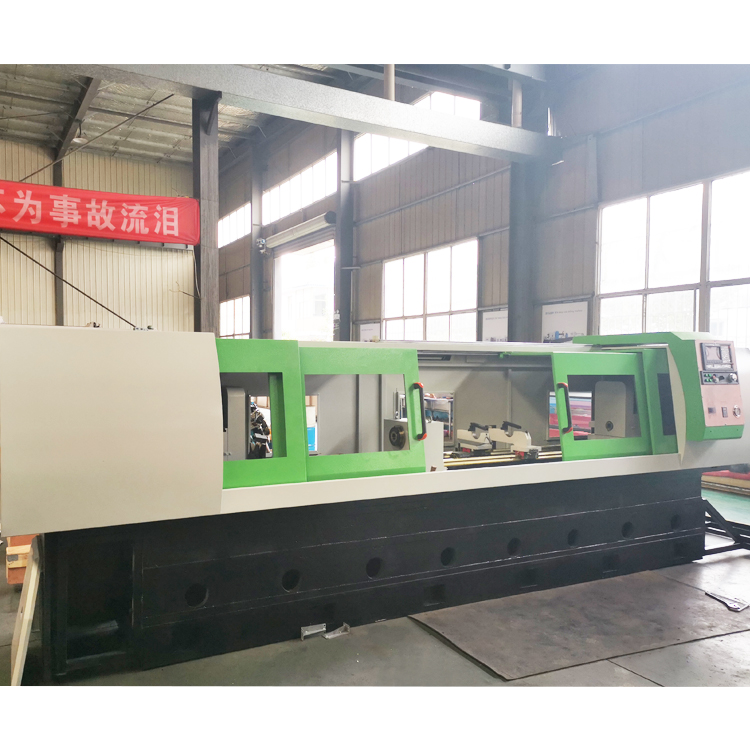
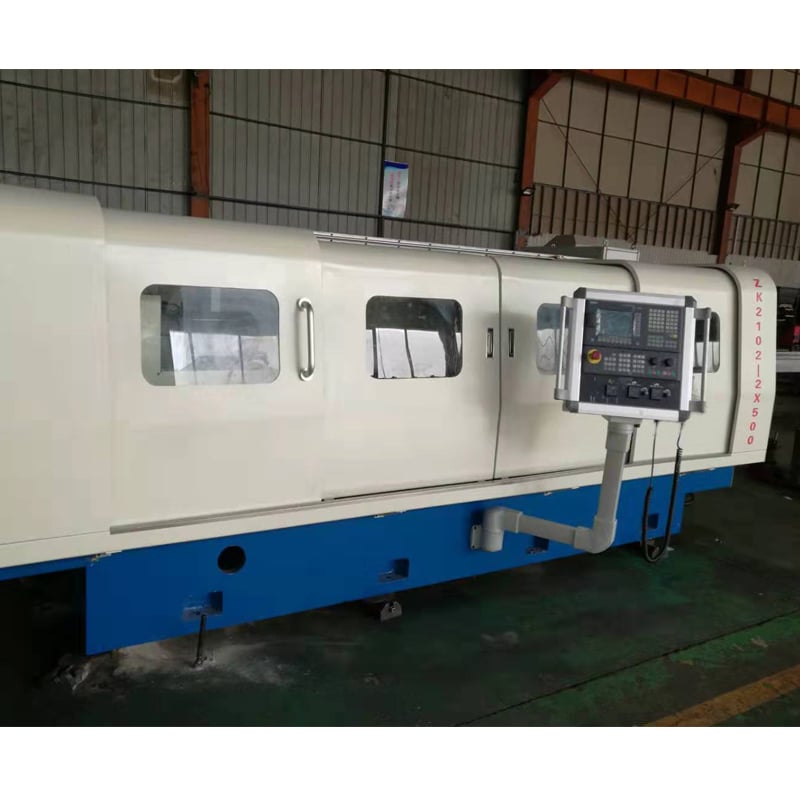
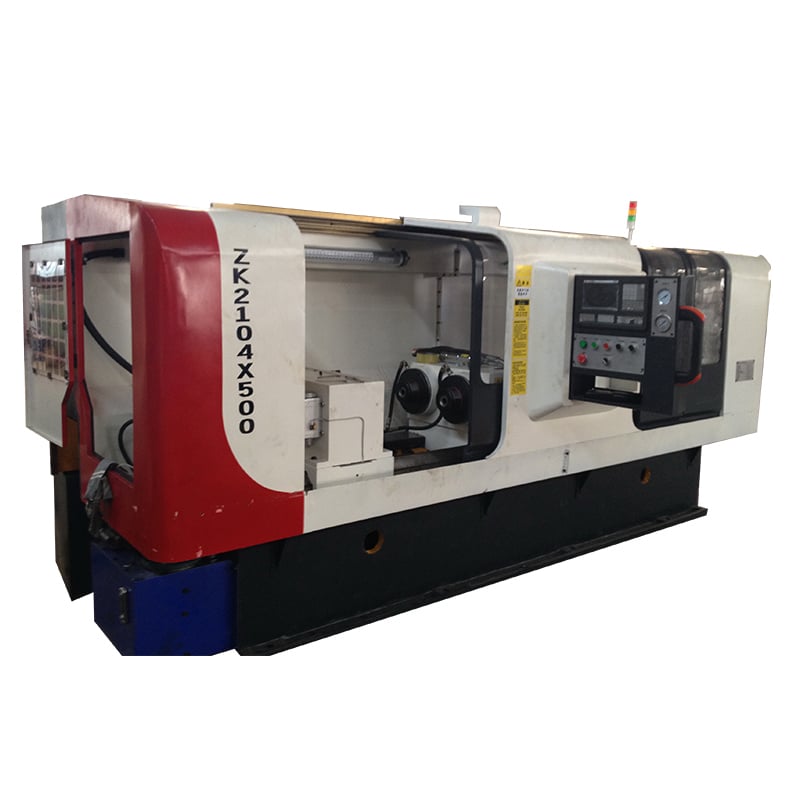
Since 2003, Taizhou Chuang Yuan Machine Tool Co., Ltd. has engineered deep hole drilling machine solutions for manufacturers who refuse to compromise on bore accuracy. Our deep hole drilling machine portfolio covers gun drilling, BTA drilling and ejection drilling configurations, delivering diameter ranges from 4 mm to 1,200 mm, depth-to-diameter ratios up to 100:1, and surface finishes of Ra 0.4 to 1.6 microns. In mold-making shops, hydraulic cylinder plants, tube and pipe production lines, and aerospace component factories, our machines run 24/7 with spindle speed stability within 1 percent, reducing scrap rates by up to 35 percent compared with conventional boring methods. A Turkish hydraulic cylinder manufacturer replaced two old lathes with one of our CNC deep hole drilling machine units and cut cycle time by 42 percent while holding concentricity within 0.02 mm across 12-hour shifts.
Get A Quote

Case Study

Hydraulic Cylinder Producer Cuts Cycle Time 42 Percent With Our Deep Hole Drilling Machine

A hydraulic cylinder manufacturer in Turkey processed 300 mm long bores on conventional lathes, facing 8 percent scrap from drifting straightness. They installed our T2120 CNC deep hole drilling machine with BTA tooling and high-pressure coolant at 80 bar. Within three months, cycle time dropped from 22 minutes to 12.8 minutes per part, scrap fell below 1.5 percent, and straightness held within 0.05 mm per meter across 4,500 monthly units. The plant now runs three shifts, and the same machine handles both 63 mm and 80 mm bore families by simple tool changes. This case proves how a right-sized deep hole drilling machine turns a bottleneck into a profit center.

Mold Base Manufacturer Reaches Ra 0.6 Finish With Gun Drilling Deep Hole Drilling Machine

A German mold base supplier needed 18 mm diameter cooling channels, 650 mm deep, without secondary honing. Our gun drilling deep hole drilling machine with carbide guide pads and internal chip evacuation delivered Ra 0.6 micron finish and 0.03 mm positional accuracy in one pass. Production time per mold plate fell from 95 minutes to 51 minutes, and the customer eliminated a separate reaming station, saving an estimated 18,000 euros annually. Over 1,200 plates have been drilled with zero rejected for surface finish, demonstrating the repeatability of our deep hole drilling machine platform.

Aerospace Tube Supplier Achieves 100:1 Depth Ratio With Ejection Deep Hole Drilling Machine

An aerospace tube fabricator in India required 10 mm holes at 1,000 mm depth in Inconel 718, a 100:1 ratio. Standard drilling failed due to tool breakage and drift. Our ejection deep hole drilling machine combined with a custom counter-rotation fixture completed each hole in 26 minutes with concentricity within 0.05 mm and no tool loss across 60 consecutive parts. The client passed AS9100 audit samples on the first submission and has since ordered a second unit, validating our deep hole drilling machine capability in the most demanding alloys.

Related products

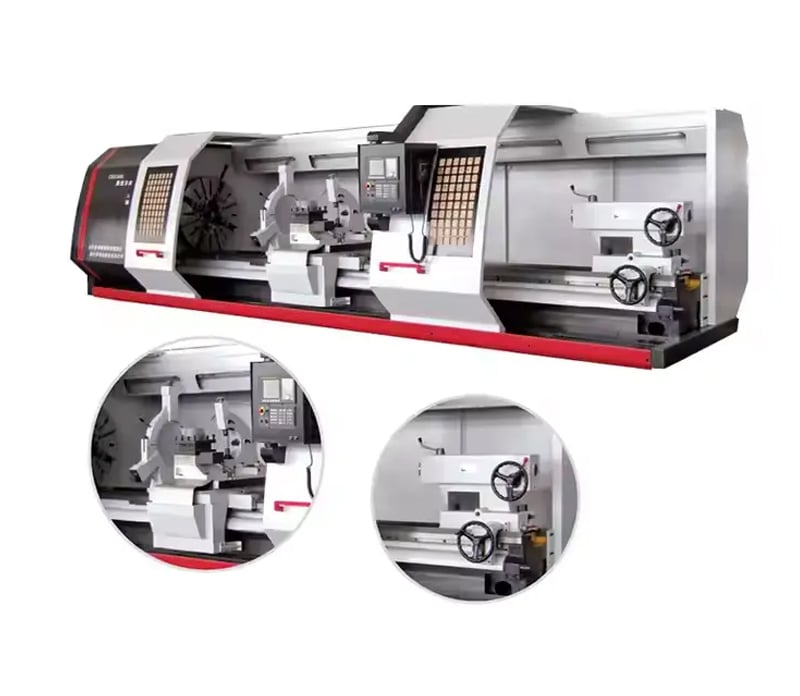
Deep hole drilling is not simply drilling deeper; it is a discipline of chip evacuation, thermal control and guide support that determines whether a bore is straight, round and mirror-finished or scrap. A deep hole drilling machine must synchronize spindle speed, feed rate, coolant pressure and tool geometry, because any imbalance causes drift, bell mouthing or catastrophic tool failure. At Taizhou Chuang Yuan Machine Tool Co., Ltd., every deep hole drilling machine is built around this principle. Our production flow begins with finite element analysis of the bed and column, ensuring vibration damping at cutting forces up to 12,000 N. Castings are stress-relieved for 48 hours, then machined on five-axis machining centers to a flatness of 0.01 mm per meter. Spindles are assembled in a temperature-controlled clean room, dynamically balanced to G1.0 grade, and tested at 4,000 rpm for four hours. The coolant system, a critical heart of any deep hole drilling machine, uses duplex filtration down to 20 microns and delivers up to 100 bar pressure, driving chips out of the bore without scoring the wall. Guide bush and steady rest alignment is verified with laser interferometry, and each machine completes a 72-hour continuous cutting trial on customer-specified material before shipment. In global applications, our deep hole drilling machine serves hydraulic cylinder barrels, injection molding manifolds, aircraft landing gear components, oil and gas valve bodies, and heat exchanger tubes. In South Korea, a tube maker uses our deep hole drilling machine to produce 6-meter pipes at 0.1 mm wall thickness tolerance. In Brazil, an agricultural machinery plant drills 120 mm bores in forged steel for harvester axles, achieving 99.2 percent first-pass yield. In Italy, a die-casting mold shop relies on our machine for conformal cooling channels that reduce cycle time by 15 percent. These results come from more than two decades of integrating research, manufacturing and sales under one roof. We export to over 20 countries and maintain long-term relationships built on measurable performance, not promises. Our engineering team provides process validation, tooling selection and operator training, so your deep hole drilling machine reaches target capability within days of installation. Whether you drill 4 mm or 1,200 mm, at 10:1 or 100:1 ratio, our deep hole drilling machine delivers the straightness, finish and throughput your contract demands.

Frequently Asked Questions

What materials can your deep hole drilling machine process effectively?

Our deep hole drilling machine handles carbon steel, alloy steel, stainless steel, Inconel, titanium, aluminum and cast iron. For hardened alloys above 40 HRC, we recommend carbide gun drilling tools with internal coolant, and our engineers provide cutting parameters validated on your material samples before shipment, ensuring stable chip evacuation and tool life.
Straightness comes from guide bush support, counter-rotation options and rigid bed design. Our deep hole drilling machine holds 0.05 mm per meter or better on typical steels, verified by laser interferometer and sample cutting. We supply a test report with every machine, so you can audit deviation before accepting delivery.
Standard models ship in 45 to 60 days after deposit, with customized deep hole drilling machine configurations in 75 to 90 days. Our technicians install, align and train your operators on-site, and remote IoT diagnostics resolve 80 percent of issues within one business day, minimizing downtime.
Yes. We offer automatic loading, chip conveyors, coolant recycling and MES-ready control interfaces. A Mexican cylinder plant integrated our deep hole drilling machine into a robotic cell handling 80 parts per shift, with no manual intervention between drilling and gauging, proving seamless automation compatibility.
We stock critical spares and ship within 48 hours to most destinations. Our deep hole drilling machine warranty covers 24 months or 4,000 operating hours, and we offer preventive maintenance contracts that reduce unplanned stoppages by up to 60 percent, keeping your investment productive for a decade or more.

Related Articles

Processing characteristics of EDM wire cutting machine

24

Dec

Processing characteristics of EDM wire cutting machine

View More
How to customize spring machine mold fixtures for special shaped spring production

03

Aug

How to customize spring machine mold fixtures for special shaped spring production

Mastering Complex Spring Production Challenges Navigating the intricacies of high-speed industrial manufacturing demands a profound understanding of wire feed dynamics, mechanical tolerances, and multi-axis bending mechanics across modern automated...
View More
Why multi functional edm machine meets mixed mold and part production factory demands

14

Aug

Why multi functional edm machine meets mixed mold and part production factory demands

Navigating the Complexities of High-Mix Manufacturing Environments Running a modern industrial production plant often feels like juggling a dozen spinning plates at once, especially when dealing with high-mix, low-volume manufacturing schedules. Pl...
View More
What output benefits enterprises gain by updating old edm spark erosion machine equipment

03

Aug

What output benefits enterprises gain by updating old edm spark erosion machine equipment

Identifying Legacy Constraints in Spark Erosion Production Operating mature, decades-old equipment on high-precision manufacturing shop floors often creates hidden operational penalties that quietly erode profit margins over time. When production f...
View More

Customer Testimonials

Mehmet Aydin, Production Director, Hydraulic Cylinder Manufacturer, Turkey
Consistent Accuracy Across Three Shifts

We run our deep hole drilling machine 20 hours a day on hydraulic cylinder tubes, and concentricity stays within 0.02 mm without operator adjustment. Scrap dropped from 7 percent to under 2 percent in the first quarter, and the ROI arrived in 11 months. The training and spare parts response have been excellent.

Rajesh Menon, Aerospace Components Supplier, India
Solved a 100:1 Depth Challenge in Inconel

Other suppliers declined our 1,000 mm deep, 10 mm diameter Inconel job. Their deep hole drilling machine with ejection tooling completed 60 consecutive holes with zero tool breakage, and our AS9100 audit passed first time. Cycle time is 26 minutes per hole, exactly as quoted.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Rigid Machine Structure Delivers Sub-0.05 mm Straightness on Every Deep Hole Drilling Machine

Rigid Machine Structure Delivers Sub-0.05 mm Straightness on Every Deep Hole Drilling Machine

The foundation of accurate deep hole drilling is a machine that does not flex. Our deep hole drilling machine uses a stress-relieved cast iron bed with finite element optimized ribs, ground guideways and a thermally symmetric column. This design absorbs cutting forces up to 12,000 N and keeps spindle-to-guide alignment within 0.01 mm per meter, even after 72 hours of continuous operation. In practice, a Korean tube manufacturer drills 6-meter pipes with 0.1 mm wall tolerance on our deep hole drilling machine, and an Italian mold shop holds 0.03 mm positional accuracy on conformal cooling channels. Compared with welded-frame alternatives, our structure reduces vibration amplitude by 40 percent, which directly improves surface finish and tool life. The machine also features a counter-rotation head option for extremely deep bores, minimizing drift without secondary operations.
High-Pressure Coolant and Filtration System Maximizes Chip Evacuation and Tool Life

High-Pressure Coolant and Filtration System Maximizes Chip Evacuation and Tool Life

Chip evacuation separates a productive deep hole drilling machine from a problematic one. Our system delivers up to 100 bar coolant pressure through the tool, with duplex filtration down to 20 microns and a temperature-controlled tank that holds coolant within 2 degrees Celsius. This prevents chip recutting, built-up edge and thermal distortion, extending carbide tool life by up to 50 percent in stainless steel and Inconel. A Brazilian agricultural machinery plant drilling 120 mm bores in forged steel reports 99.2 percent first-pass yield and tool changes every 180 holes instead of 90. The coolant system is fully enclosed, meeting European workshop environmental standards, and includes chip conveyor and oil mist extraction. For high-volume producers, this translates into lower consumable cost, cleaner parts and fewer unplanned stops. Every deep hole drilling machine we ship includes a coolant commissioning report with pressure.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop