Deep Hole Gun Drilling Machine | 100:1 Ratio, 0.01mm Accuracy

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Precision Deep Hole Gun Drilling Machine Solutions From A Trusted Chinese Manufacturer

Precision Deep Hole Gun Drilling Machine Solutions From A Trusted Chinese Manufacturer

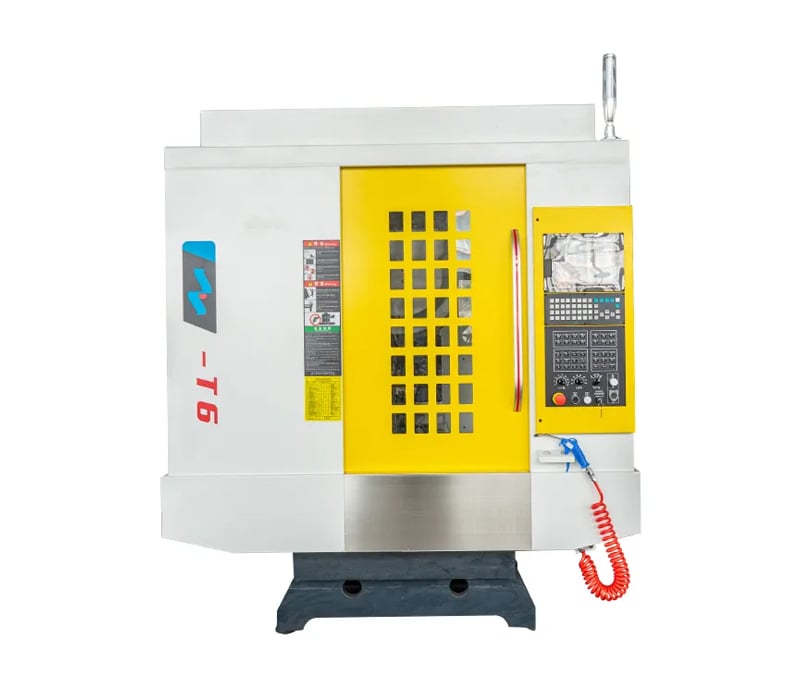
Taizhou Chuang Yuan Machine Tool Co., Ltd. has manufactured Deep Hole Gun Drilling Machines since 2003 in Taizhou City, Jiangsu Province, China. Our Deep Hole Gun Drilling Machine delivers hole diameters from 2 mm to 40 mm, drilling depth-to-diameter ratios up to 100:1, surface roughness Ra 0.4-1.6 um, and positioning accuracy of 0.01 mm per 300 mm. Spindle speeds reach 6,000 rpm with coolant pressure up to 100 bar, so deep holes are produced in one pass without peck drilling. In hydraulic cylinder manufacturing, customers drill 800 mm deep holes in 45 steel rods at 18 minutes per part, cutting cycle time by 35%. In mold making, a German tool shop uses our Deep Hole Gun Drilling Machine to produce water lines 600 mm deep in 1.2344 steel with concentricity within 0.02 mm, eliminating secondary reaming. In medical implant production, a Swiss customer drills 3 mm holes through 120 mm titanium bars with no deflection, holding tolerance within 0.015 mm.
Get A Quote

Case Study

35% Cycle Time Reduction For Hydraulic Cylinder Manufacturer In India

A hydraulic cylinder producer in Pune, India, drilled 800 mm deep holes in 45 steel rods with conventional twist drills and required 27 minutes per part, with frequent breakouts and 2% scrap. After installing our Deep Hole Gun Drilling Machine with a 100 bar coolant system and 2,800 rpm spindle, cycle time fell to 18 minutes per part, scrap dropped to 0.3%, and hole straightness stayed within 0.1 mm over 800 mm. The company now exports hydraulic cylinders to Europe and increased monthly output by 2,400 pieces.

0.02 mm Concentricity For A German Mold Base Manufacturer

A German mold maker needed 600 mm deep cooling channels in 1.2344 steel blocks with concentricity within 0.02 mm. Traditional drilling caused drift and required reaming. Our Deep Hole Gun Drilling Machine, equipped with a BTA head and servo feed, held concentricity within 0.018 mm and surface roughness Ra 0.6 um in one pass. The customer reduced secondary operations by 80%, shortened lead time from 12 days to 5 days, and now runs two shifts daily on the same machine.

Deflection-Free 3 mm Titanium Holes For A Swiss Medical Implant Producer

A Swiss medical implant manufacturer needed 3 mm diameter holes through 120 mm titanium bars with tolerance within 0.015 mm. Our Deep Hole Gun Drilling Machine with high-pressure coolant and a carbide gun drill achieved 0.012 mm tolerance and 0.4 um surface finish, with no visible deflection. Production yield rose to 99.6%, tool life reached 120 holes per regrind, and the customer now uses our machine for three implant lines and exports to 14 countries.

Related products

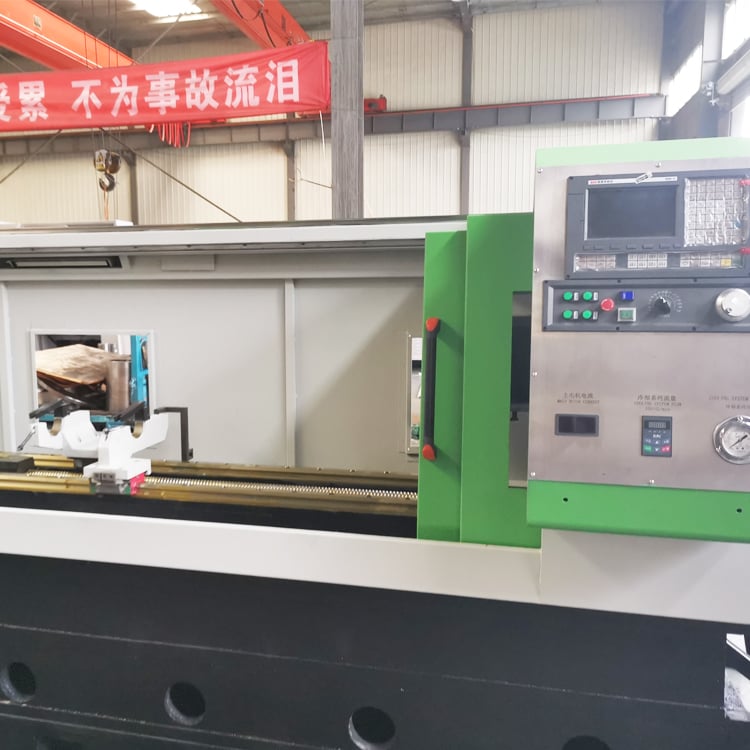
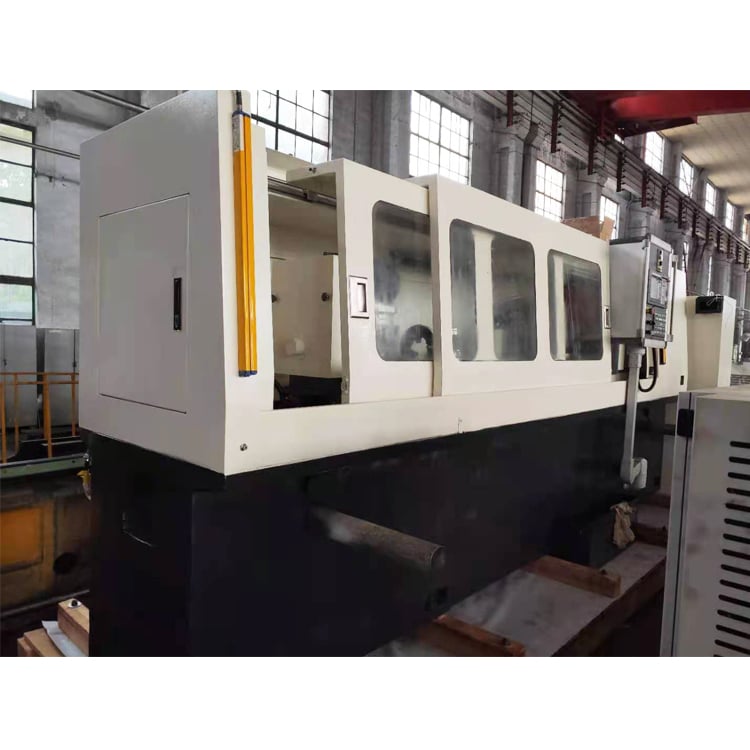
The Deep Hole Gun Drilling Machine is a specialized machining tool engineered to produce accurate deep holes with high length-to-diameter ratios in a single pass. At Taizhou Chuang Yuan Machine Tool Co., Ltd., established in 2003 in Jiangsu Province, China, we integrate research, development, production, and sales to deliver reliable precision machine tools to more than 20 countries. Our Deep Hole Gun Drilling Machine is built around a rigid cast iron bed, hardened and ground box ways, and a precision spindle that reaches 6,000 rpm. The coolant system supplies up to 100 bar pressure, which removes chips efficiently and controls thermal growth during long cycles. The machine handles hole diameters from 2 mm to 40 mm and depth-to-diameter ratios up to 100:1, with positioning accuracy of 0.01 mm per 300 mm and roundness within 0.02 mm. The production process begins with strict raw material inspection, followed by CNC machining of the bed and headstock, hand scraping of guideways, and dynamic balance testing of the spindle. Each unit then undergoes a 72-hour continuous running test that checks hole straightness, surface finish, and coolant pressure stability. A Siemens 828D CNC system manages feed rates, spindle speed, and coolant flow, and stores up to 500 programs for quick changeover. The automatic chip removal system reduces manual intervention and keeps the work area clean. In real applications, an Indian hydraulic cylinder manufacturer cuts 800 mm deep holes in 45 steel rods in 18 minutes per part, a German mold maker holds 0.018 mm concentricity in 1.2344 steel, and a Swiss medical producer drills 3 mm holes through 120 mm titanium bars within 0.012 mm tolerance. These results come from our focus on practical engineering: hardened guideways, precision ground ballscrews, and a high-pressure coolant unit that together lower tool cost per hole by up to 28% and raise throughput by 35%. Our factory covers the full process from casting and machining to assembly and testing, so we control quality at every step. We provide CE certification, a 24-month warranty, on-site installation, and online operator training. Whether you are in mold making, hydraulic equipment, aerospace, medical devices, or defense manufacturing, our Deep Hole Gun Drilling Machine offers a dependable, efficient, and cost-effective answer for deep hole challenges. We continue to invest in research and listen to customer feedback from Europe, Asia, South America, and the Middle East, refining our machines to meet diverse production environments and helping partners develop their local markets with confidence.

Frequently Asked Questions

What materials can your Deep Hole Gun Drilling Machine process?

Our Deep Hole Gun Drilling Machine handles carbon steel, alloy steel, stainless steel, cast iron, aluminum, copper, titanium, and Inconel. For example, it drills 3 mm holes through 120 mm titanium bars and 800 mm holes in 45 steel rods. Hardness up to HRC 42 is suitable. For harder materials, we recommend coated carbide gun drills and adjusted feed rates. Our engineers provide cutting parameters based on your material and hole size.
The machine supports hole diameters from 2 mm to 40 mm and depth-to-diameter ratios up to 100:1. For a 10 mm hole, you can drill up to 1,000 mm in one pass. Coolant pressure up to 100 bar ensures chip removal and straightness. If your ratio exceeds 100:1, we can customize the machine with a larger coolant system and special guide bushings.
We use a rigid cast iron bed, hardened box ways, and precision ground ballscrews to minimize vibration. The high-pressure coolant system removes chips quickly, and the Siemens CNC holds feed rates within 0.01 mm. Typically, straightness stays within 0.1 mm over 800 mm, roundness within 0.02 mm, and surface roughness between Ra 0.4 and 1.6 um. Each machine passes a 72-hour continuous test before shipment.
Standard models ship in 30 to 45 days after deposit; customized models take 60 to 75 days. We provide a 24-month warranty, on-site installation, and online training. Spare parts are available for at least 10 years. We also offer remote diagnostics through the CNC system, so most issues can be solved without a site visit, reducing downtime for customers in over 20 countries.
Yes. We customize stroke length, spindle speed, coolant pressure, control system, and fixturing. For example, we built a machine for a German mold maker with 600 mm stroke and 0.018 mm concentricity requirements. We can add automatic loading, chip conveyors, and tool monitoring. Our engineers review your drawings and samples, then propose a configuration that fits your budget and production targets.

Related Articles

How to choose a machining center?

12

Dec

How to choose a machining center?

View More
What after sales service should reliable edm drilling machine suppliers provide

14

Jul

What after sales service should reliable edm drilling machine suppliers provide

The Evolution of Flexible Manufacturing Through Modular Architecture Modern industrial landscapes demand a high degree of adaptability, where the ability to transition production configurations quickly defines a facility’s operational rhythm....
View More
How to reduce drill bit wear during continuous deep hole machine processing tasks

03

Aug

How to reduce drill bit wear during continuous deep hole machine processing tasks

Understanding the Mechanics of Deep Hole Thermal Stress Executing continuous boring and high-depth machining tasks on industrial production lines presents severe thermal and mechanical challenges that routinely test the limits of cutting tooling. W...
View More
What export quality standards international clients require for wire cutting machine products

03

Aug

What export quality standards international clients require for wire cutting machine products

Understanding International Export Compliance in Precision Machining Navigating the complex landscape of global industrial trade requires a thorough understanding of the stringent technical benchmarks that overseas buyers mandate for advanced metal...
View More

Customer Testimonials

Rajesh Mehta, Production Manager, Pune, India
Excellent Precision And Uptime In Daily Production

We purchased a Deep Hole Gun Drilling Machine for our hydraulic cylinder line. After six months, cycle time dropped from 27 to 18 minutes per part, and scrap fell below 0.5%. The 100 bar coolant system handles 800 mm deep holes in 45 steel without any drill breakage. Installation and training were smooth, and the machine runs two shifts daily with no major issues. It has become the most reliable machine on our floor.

Thomas Keller, Operations Director, Zurich, Switzerland
Reliable Performance For Mold Making And Medical Parts

Our Swiss medical implant production needs 3 mm holes through 120 mm titanium bars. This Deep Hole Gun Drilling Machine holds 0.012 mm tolerance and 0.4 um surface finish consistently. We also use it for mold bases and achieve 0.02 mm concentricity. The Siemens control stores 500 programs, so changeover is fast. After one year, tool cost per hole is down 28%, and output is up 35%. Excellent support from the manufacturer.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
High-Pressure Coolant System For Deep Holes Up To 100:1 Ratio

High-Pressure Coolant System For Deep Holes Up To 100:1 Ratio

Our Deep Hole Gun Drilling Machine features a coolant system that delivers up to 100 bar pressure, which is essential for deep hole drilling. High pressure flushes chips out of the hole, cools the cutting edge, and prevents chip packing that causes drill breakage and poor surface finish. This allows one-pass drilling with depth-to-diameter ratios up to 100:1, so a 10 mm hole can reach 1,000 mm without peck drilling. In hydraulic cylinder production, this system helps drill 800 mm deep holes in 45 steel rods in 18 minutes per part, reducing cycle time by 35%. In mold making, it supports 600 mm deep cooling channels in 1.2344 steel with 0.018 mm concentricity. The system includes a high-pressure pump, filtration unit, and adjustable flow control, and it works with water-based or oil-based coolants. The coolant tank is sized for continuous operation, and the chip removal system keeps the work area clean.
Rigid Machine Structure Ensures 0.01 mm Positioning Accuracy

Rigid Machine Structure Ensures 0.01 mm Positioning Accuracy

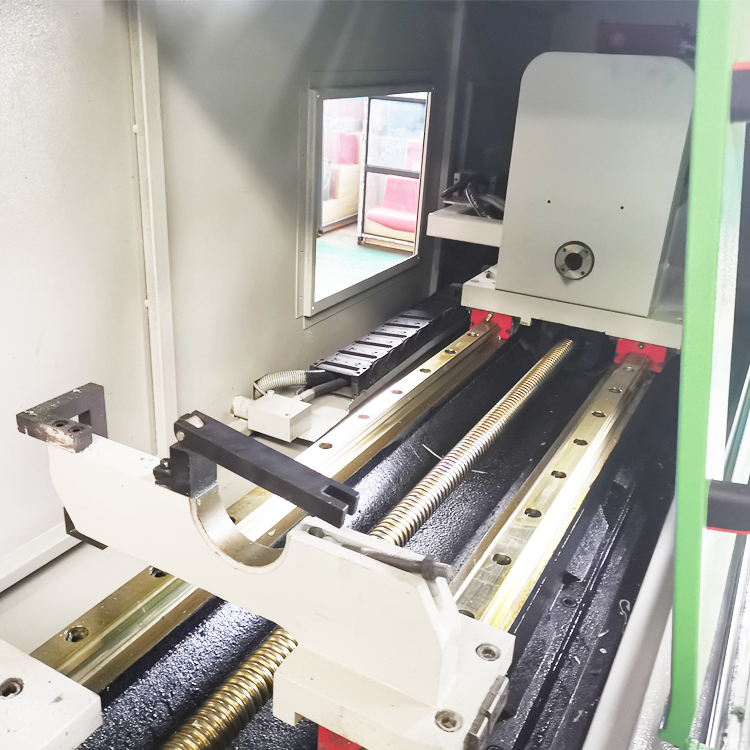
The Deep Hole Gun Drilling Machine is built on a heavily ribbed cast iron bed that absorbs vibration and maintains stability during heavy cutting. Hardened and ground box ways, plus precision ground ballscrews, deliver positioning accuracy of 0.01 mm per 300 mm and repeatability of 0.005 mm. The spindle is dynamically balanced and supported by high-precision bearings, reaching 6,000 rpm with low runout. This rigidity is critical for deep hole drilling, where small deflections grow into large errors over long holes. A German mold maker used this machine to hold 0.018 mm concentricity in 600 mm deep holes, and a Swiss medical producer achieved 0.012 mm tolerance in 3 mm holes through 120 mm titanium bars. The structure also supports roundness within 0.02 mm and surface roughness Ra 0.4 to 1.6 um, reducing the need for secondary reaming and lowering total processing cost. Each machine undergoes hand scraping and laser interferometer calibration before shipment.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop