Top Steel Slitter Manufacturers | Precision Slitting Lines

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
WeChat
Linkedin
Name
Company Name
Message
0/1000
Attachment
Please upload at least an attachment
Up to 3 files,more 30mb,suppor jpg、jpeg、png、pdf、doc、docx、xls、xlsx、csv、txt
Steel Slitter Manufacturers Delivering Precision, Speed And Global Service

Steel Slitter Manufacturers Delivering Precision, Speed And Global Service

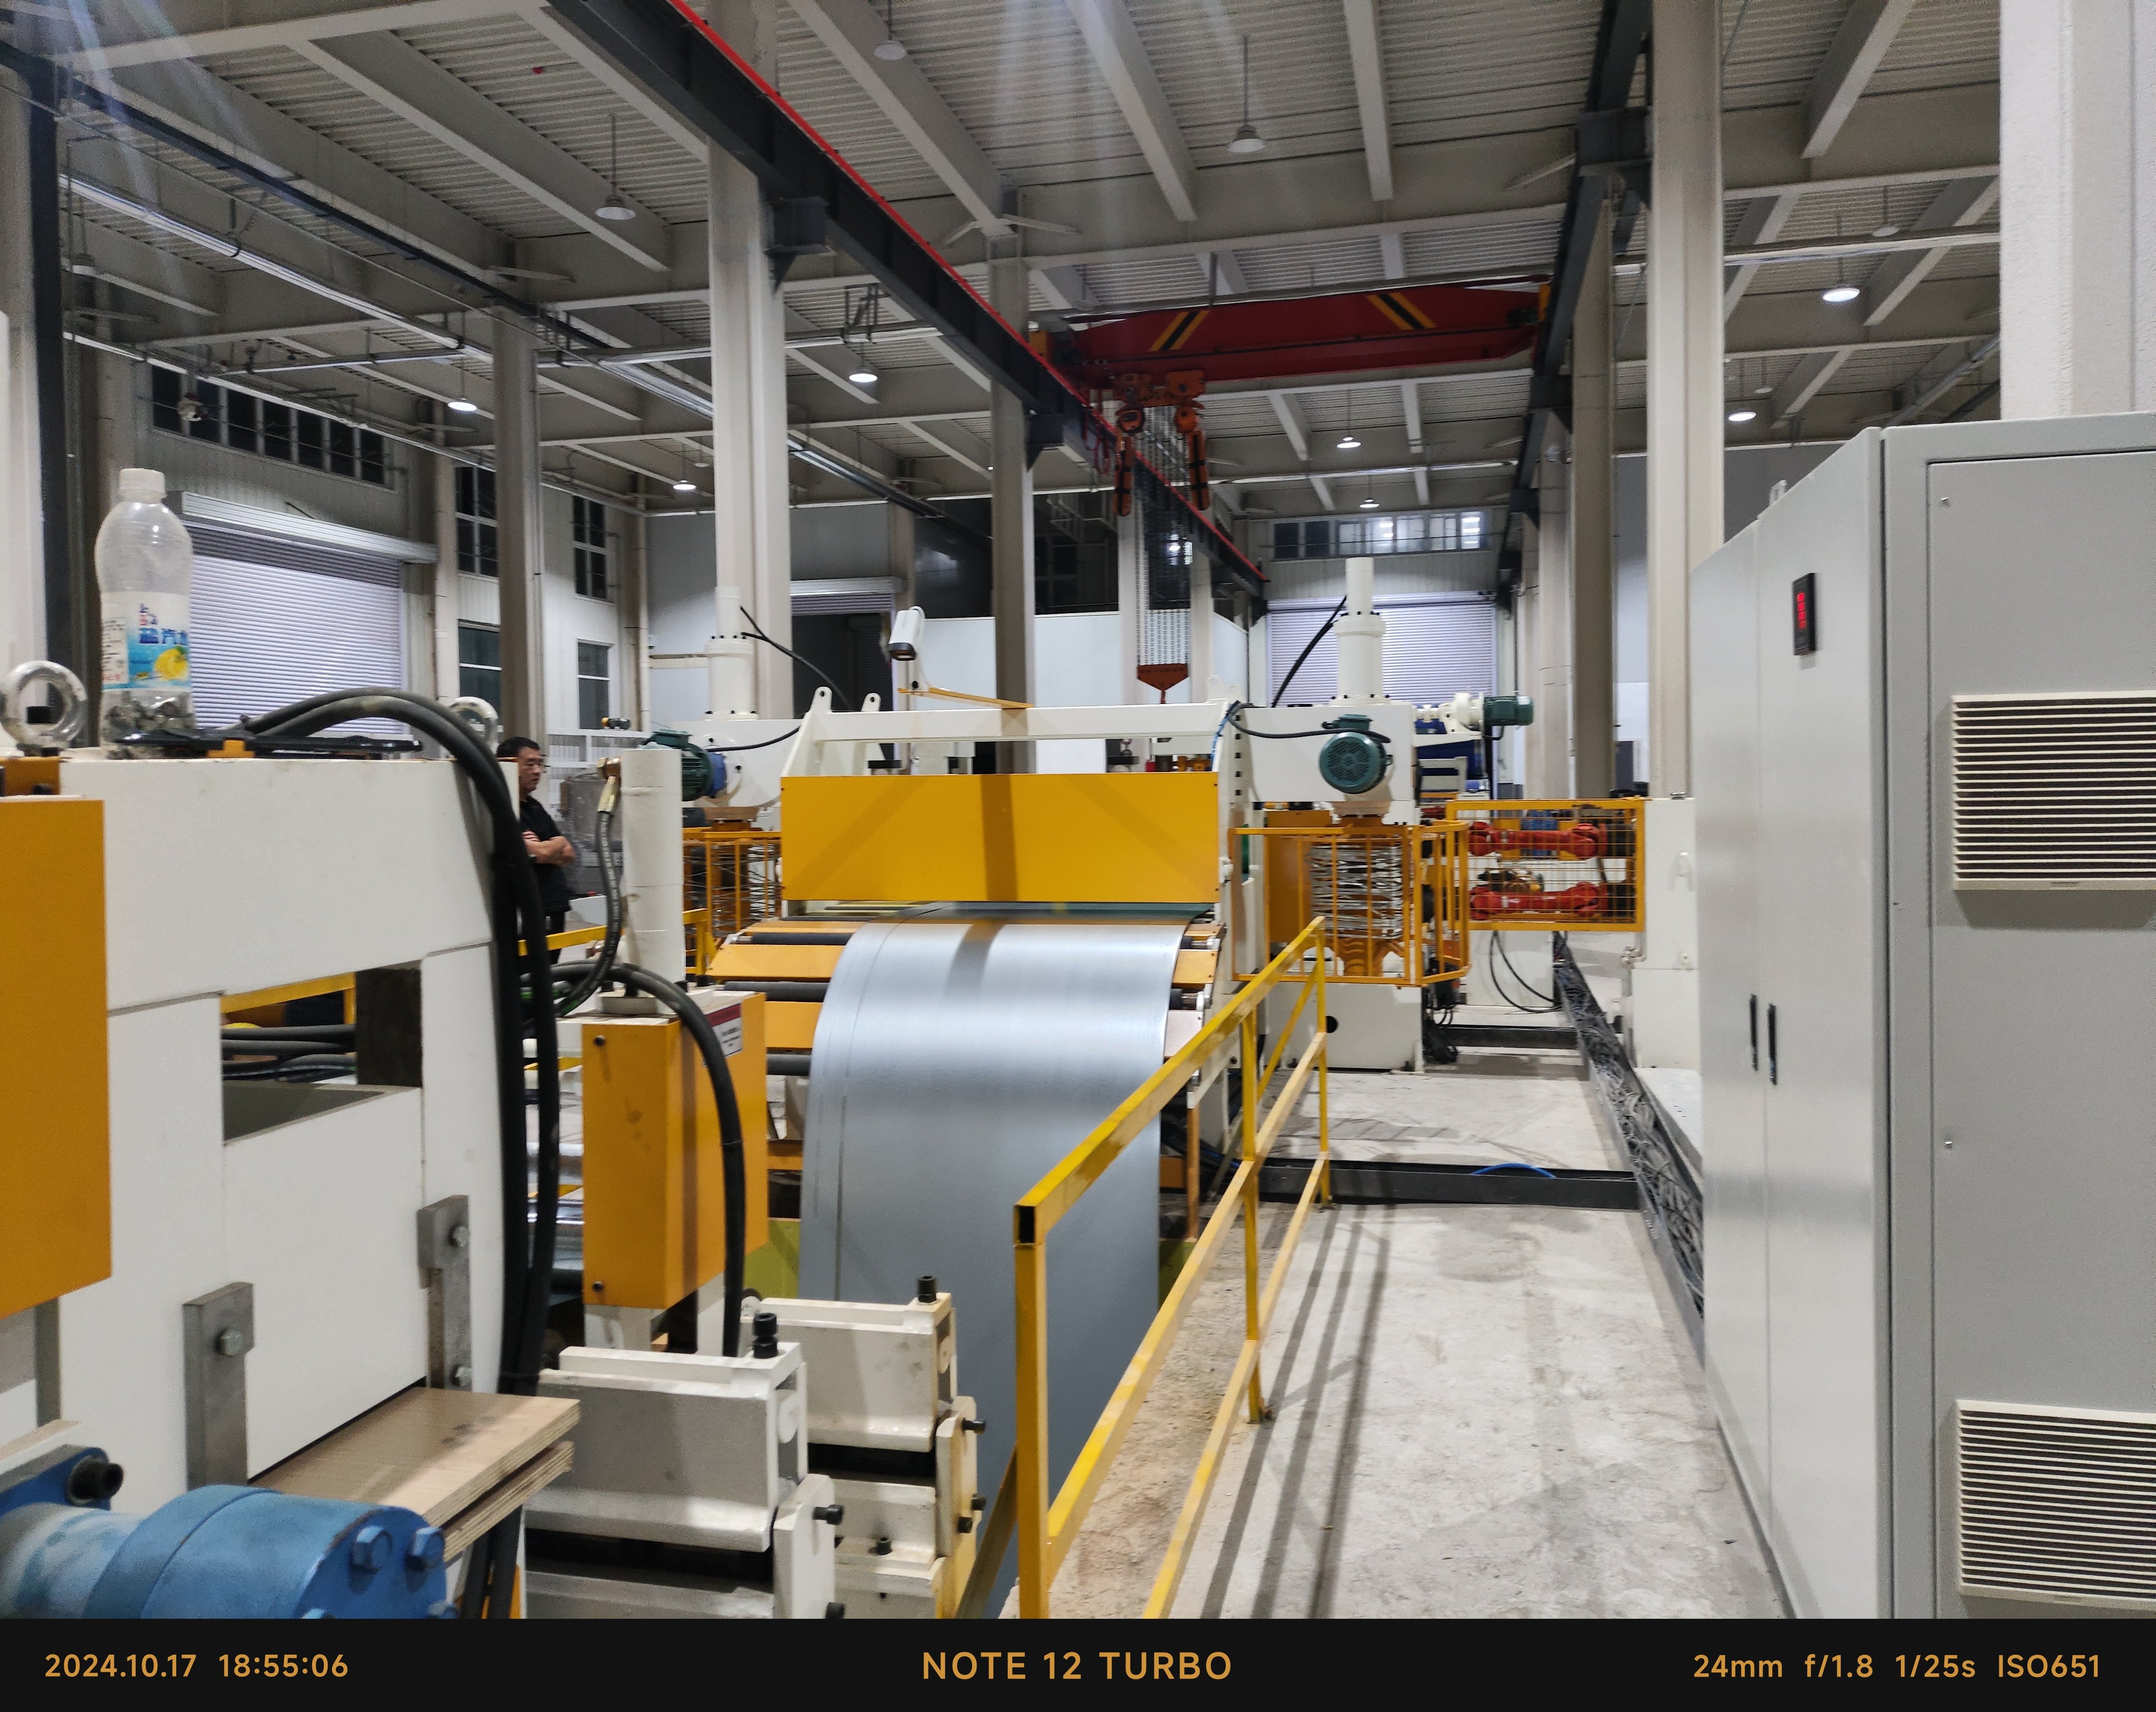
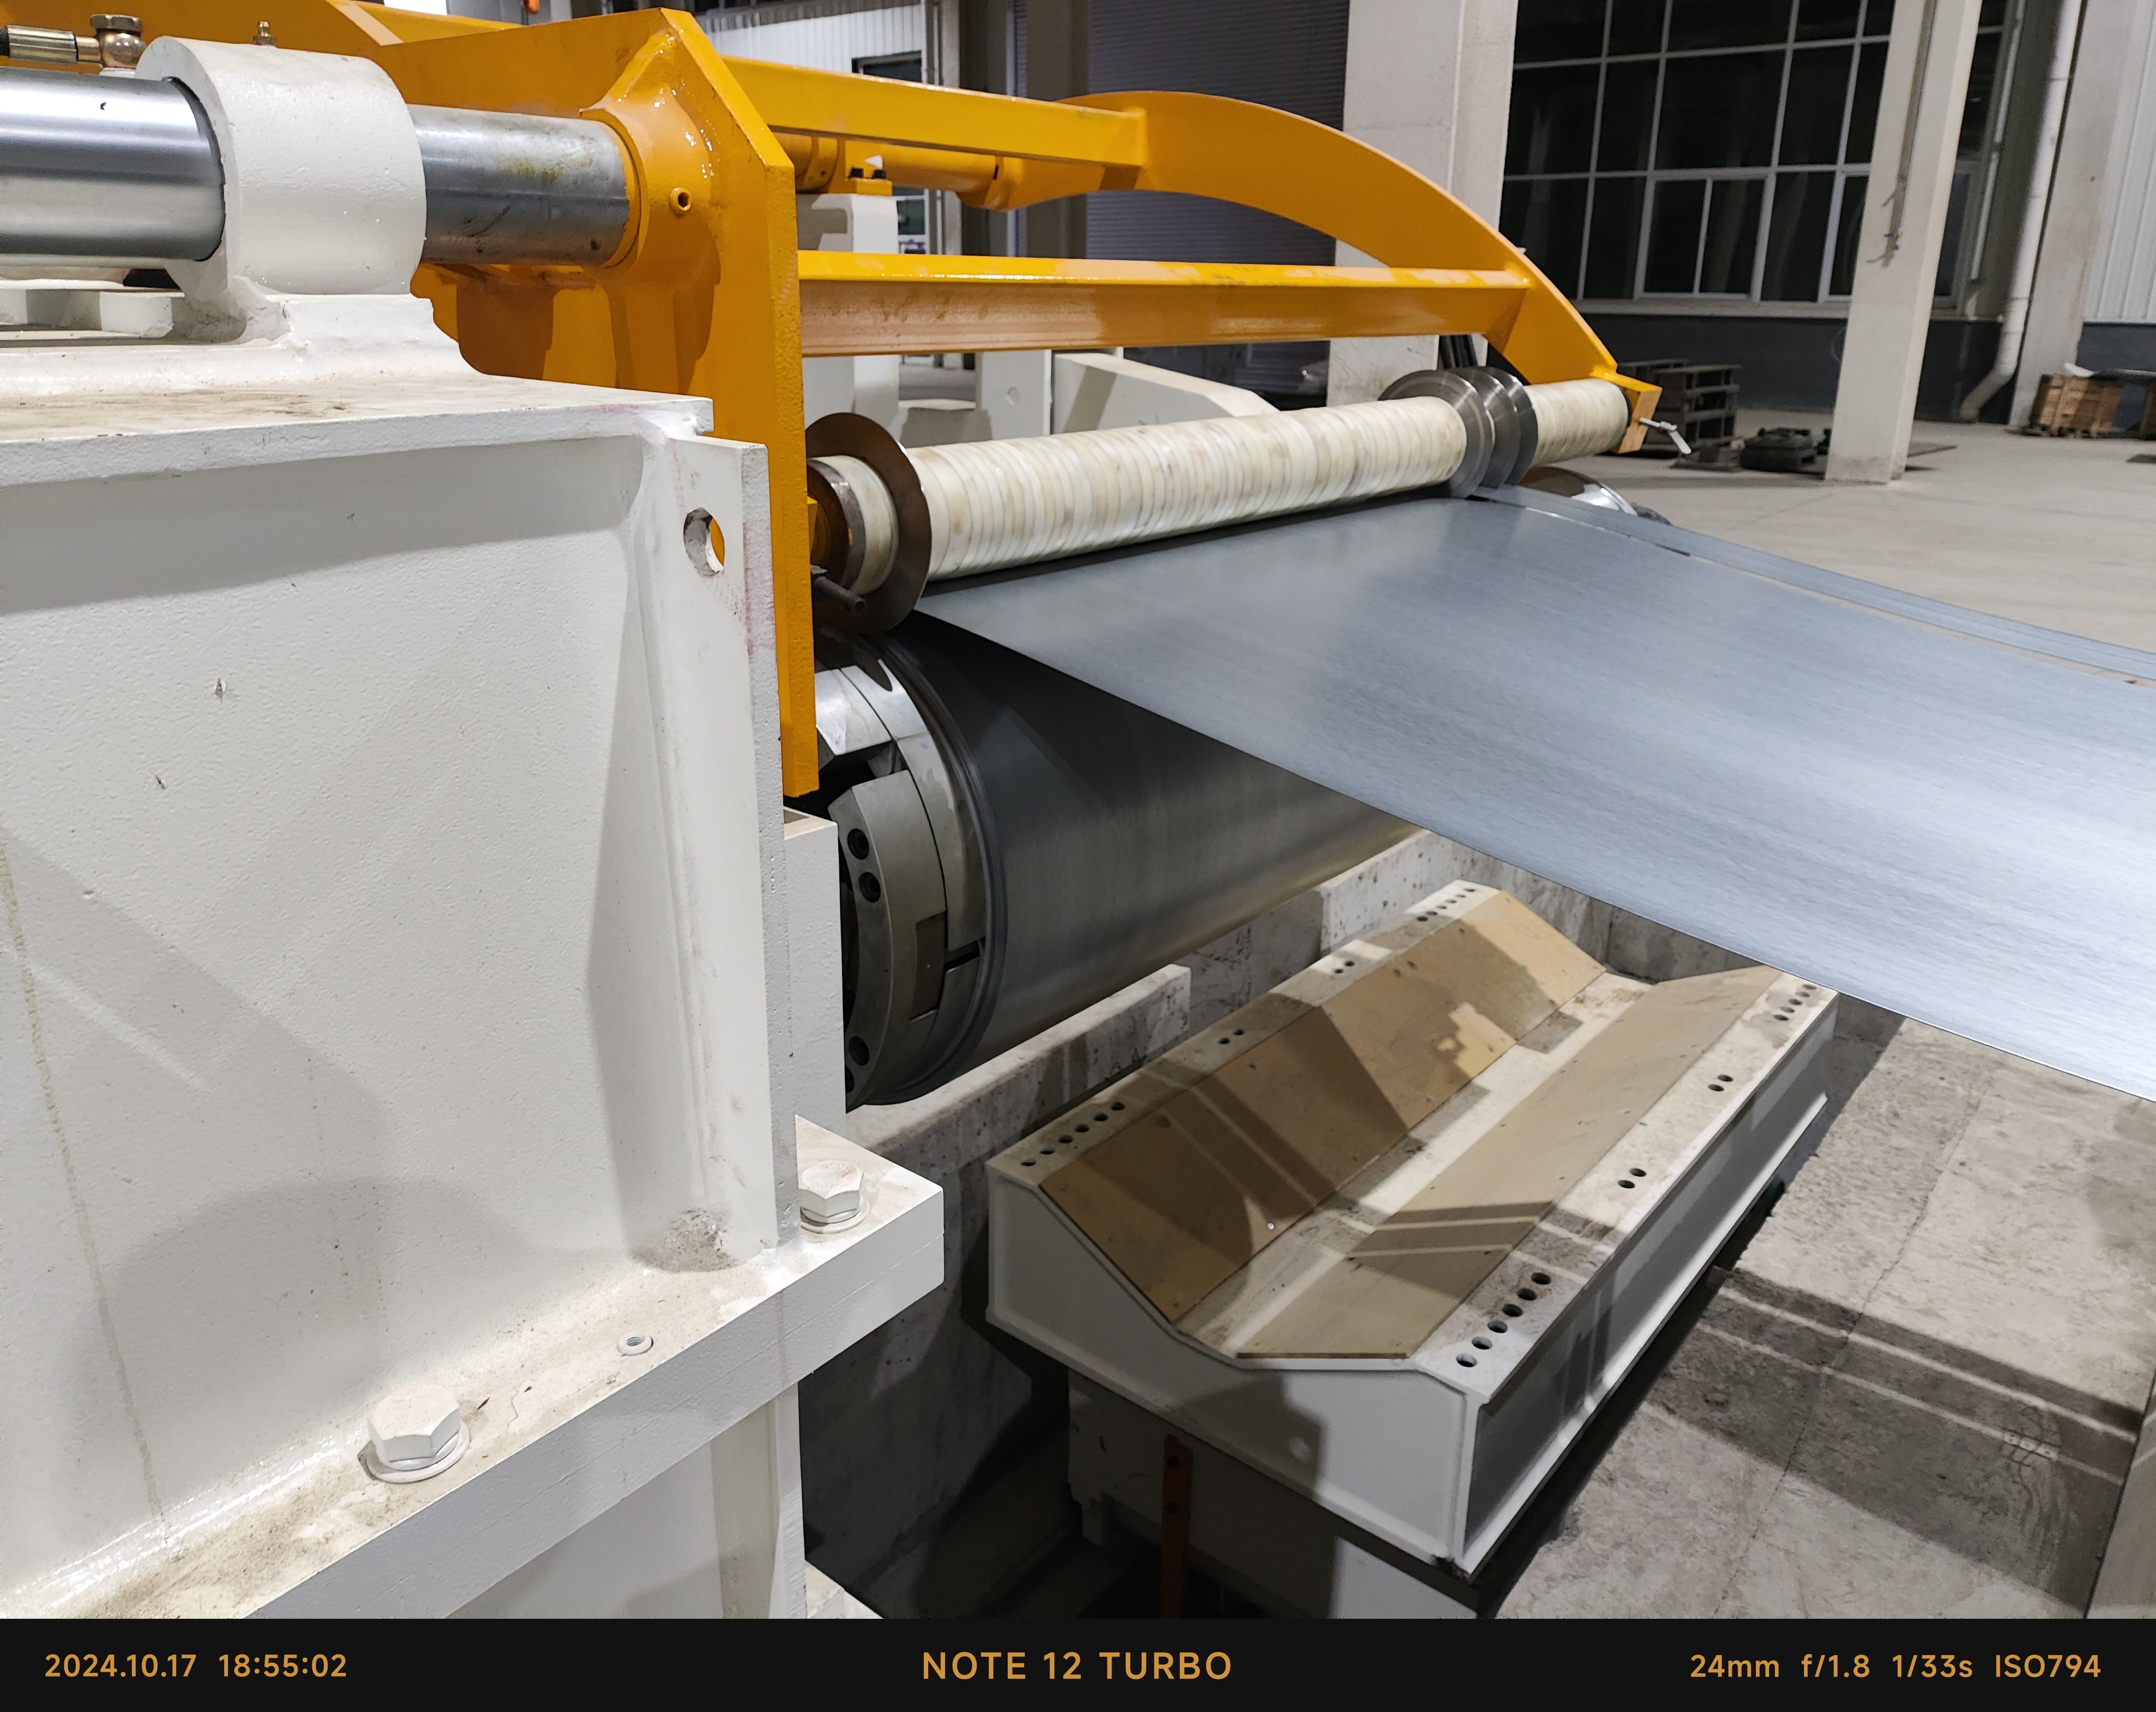
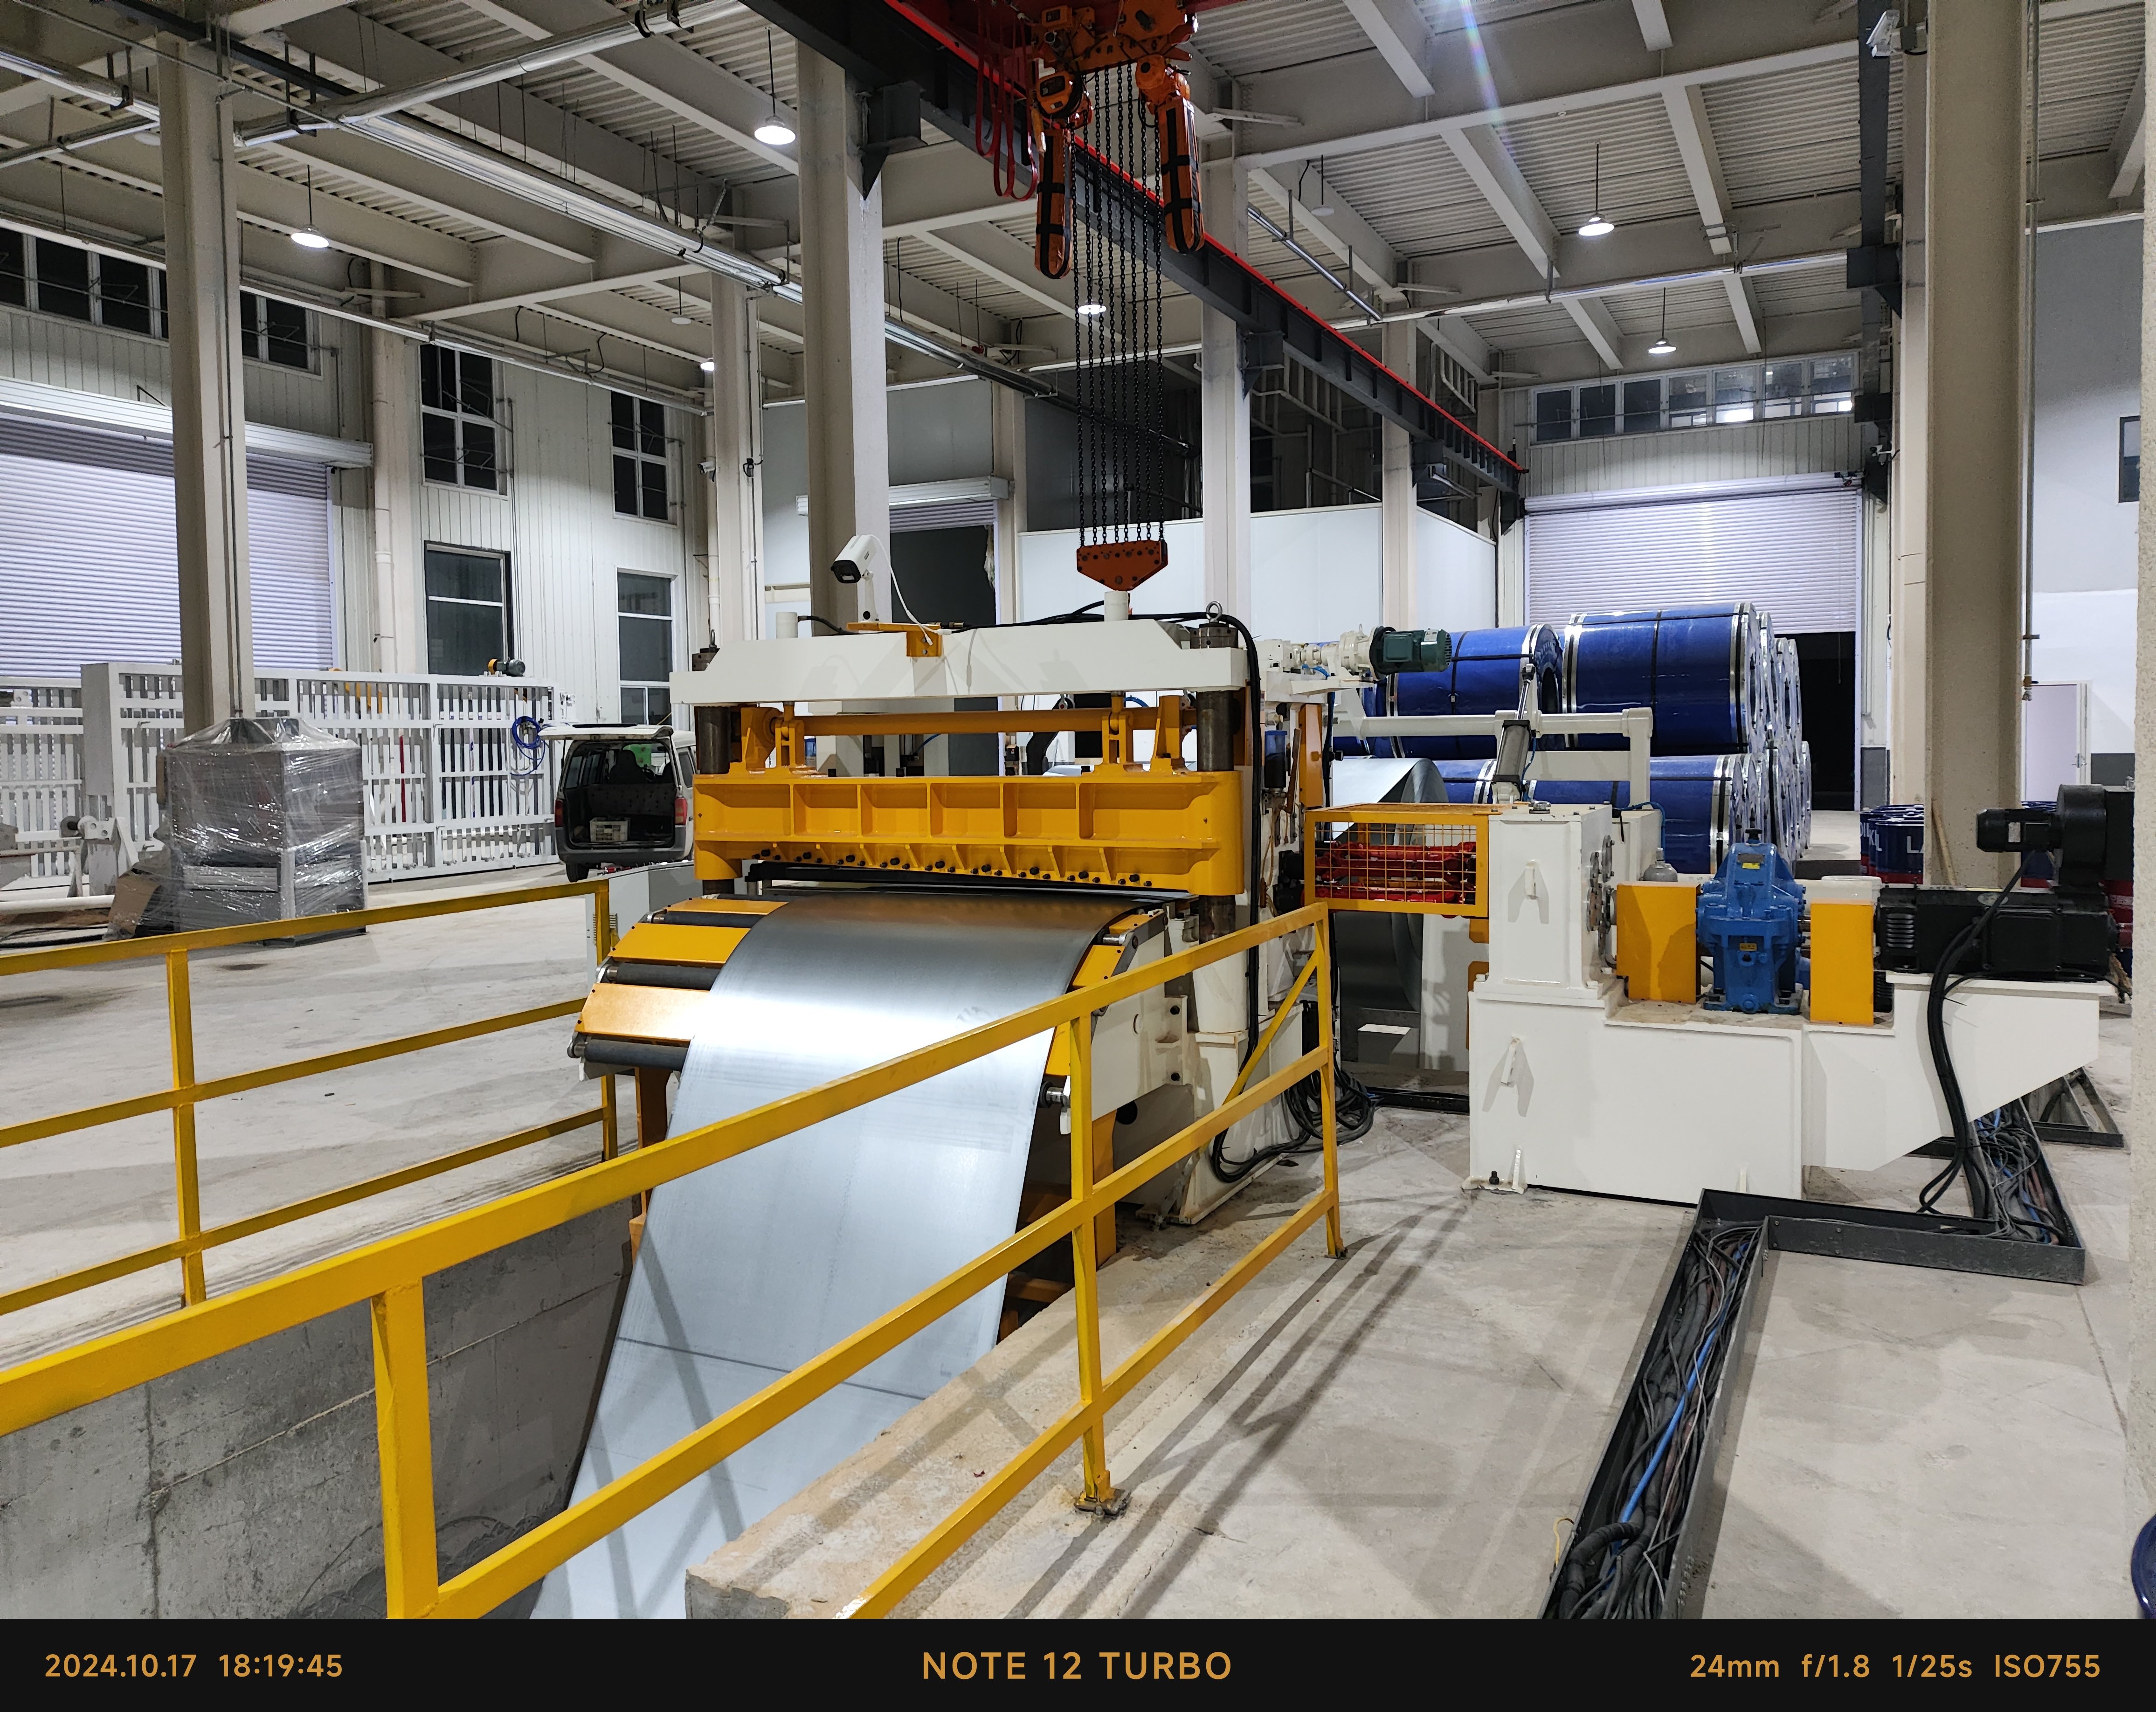
As one of the most dependable steel slitter manufacturers, Taizhou Chuang Yuan Machine Tool Co., Ltd. has engineered, manufactured and supported precision slitting lines since 2003 from its base in Taizhou City, Jiangsu Province, China. Our steel slitting lines are built for coil service centers, welded pipe producers, automotive stamping suppliers and appliance manufacturers that run 3 to 12 mm thick, 600 to 2,000 mm wide coils at line speeds of 30 to 120 m/min. Every line combines hydraulic uncoiling, precision leveling, high-rigidity slitting heads, scrap winding and tension-controlled recoiling in one synchronized system. Blade shaft runout is held within 0.02 mm and slit width tolerance within plus or minus 0.05 mm, so downstream roll formers and presses receive consistently square, burr-controlled strips. Each set passes a 72-hour continuous no-load and load test before shipment, and we validate slitting accuracy against buyer strip samples.
Get A Quote

Case Study

1,600 mm Steel Slitting Line For A German Coil Service Center

A major German coil service center specializing in advanced metal distribution faced significant operational challenges when processing high-strength low-alloy steel master coils up to 12 mm in thickness, primarily due to excessive strip camber and loose edge tolerances that triggered customer rejections. To solve this bottleneck, our engineering team configured and supplied a heavy-duty steel slitting line equipped with a robust 75 kW hydraulic uncoiler, a high-rigidity six-roll precision leveler, six precision-engineered slitting heads, and a four-arm tension recoiler. Following rigorous on-site installation and commissioning by our technical specialists, the machinery achieved exceptional performance benchmarks: edge burr height was strictly controlled under 0.05 mm, strip camber remained tightly under 1 mm per 2 meters of length, and stable operational line speeds reached 90 m/min.

High-Speed Steel Slitter Supplied To A Turkish Welded Pipe Producer

A prominent Turkish welded pipe manufacturing facility required high-speed, precision-cut narrow steel strips for continuous square tube production, frequently executing multiple width changeovers across small production batches. To address their specific operational workflow, we engineered and delivered a specialized quick-change steel slitter line featuring cartridge-style slitting heads, a powerful 60 kW drive system, and a servo loop-controlled recoiler. This advanced configuration successfully reduced strip width changeover downtime from an inefficient 75 minutes down to an agile 28 minutes, while maintaining strict width accuracies within plus or minus 0.05 mm and decreasing material scrap loss from 3.1 percent to 1.9 percent. Within nine months of full commercial operation, the client successfully recovered their total equipment capital investment through enhanced production yield and drastically minimized non-productive downtime.

Custom Steel Slitting Line For An Indian Appliance Parts Manufacturer

An established Indian appliance parts manufacturer needed burr-free galvanized steel strips for washing machine and refrigerator panels. Our steel slitting line used polymer-coated tension pads, a six-high leveler and automatic edge trimming. Surface defect rate from slitting dropped below 0.4 percent, zinc coating damage was eliminated, and the line now runs 120 m/min with a 20 percent energy saving versus the client's previous machine. This project strengthened our reputation among steel slitter manufacturers in the South Asian appliance supply chain.

Related products

Steel slitting sits at the center of modern metal supply chains, and the performance of steel slitter manufacturers directly affects coil yield, surface quality and delivery reliability for every service center and factory that consumes slit strip. Taizhou Chuang Yuan Machine Tool Co., Ltd. has focused on precision machine tool research, development, production and sales since 2003, building steel slitting lines that convert master coils into finished strips for welded pipe, automotive, appliance, construction and electrical equipment industries. Our engineering process begins with the customer's coil data: material grade, tensile strength, thickness range from 3 mm to 12 mm, strip width from 20 mm to 1,600 mm, coil weight up to 30 tons and required output per shift. From these inputs our designers select shaft diameter, blade material, leveling roll configuration and tension control strategy. Slitting heads are machined on CNC boring and milling centers, then dynamically balanced, so knife shaft concentricity is maintained within 0.02 mm during full-speed operation. Slitting blades are made from Cr12MoV or SKD11 tool steel, vacuum heat treated to HRC 58 to 62, and ground in matched sets to guarantee consistent clearance and strip edge quality.
A complete steel slitting line includes a hydraulic uncoiler with coil car, peeler, pinch and leveling unit, loop pit, slitting head, scrap winder, tension station and recoiler with hydraulic push-off. Electrical control uses PLC and HMI, with recipe storage for more than 100 strip specifications, automatic tension calculation and fault diagnostics. Optional features include quick-change cartridge heads, edge trimming, oiling units and coil packing devices. Before delivery, each line undergoes alignment checks, no-load running at rated speed, and load tests using customer material. Installation and commissioning are performed by our engineers or supported through video-guided procedures in more than 20 exporting countries. In a typical 1,600 mm high-speed line, energy consumption ranges from 15 to 45 kW, coil loading takes under 3 minutes, and slitting accuracy reaches plus or minus 0.05 mm. These figures translate into higher material utilization, fewer blade changes and lower labor cost for coil service centers, pipe mills and OEM stamping plants. We also manufacture EDM machines, machining centers, pipe making machines, cut-to-length lines, lathes and deep hole processing machines, allowing us to support broader metalworking projects while staying laser-focused on steel slitting technology. Choosing the right steel slitter manufacturers means partnering with a team that understands coil metallurgy, line dynamics and global service expectations. Our machines work in Europe, Southeast Asia, the Middle East, Africa and South America, supported by spare parts kits, multilingual manuals and remote troubleshooting within 24 to 48 hours. Field data shows that well-maintained slitting lines from our factory achieve over 95 percent availability and blade life beyond 8,000 tons of processed strip. On-site training covers blade assembly, clearance setting, tension tuning and preventive maintenance, helping clients build internal capability instead of relying on external service teams. Sustainability also matters: optimized motor sizing, regenerative braking options and efficient hydraulic systems reduce power per ton, while accurate slitting minimizes scrap. By combining engineering discipline, verified testing and global project experience, Chuang Yuan helps customers turn coil processing into a reliable, profitable operation.

Frequently Asked Questions

What Should Buyers Check When Comparing Steel Slitter Manufacturers?

Buyers should verify four points: machining capability, testing standards, project references and service response. Ask for knife shaft concentricity data, which should be within 0.02 mm, slitting accuracy of plus or minus 0.05 mm and a 72-hour load test record. Confirm that the manufacturer machines slitting heads on CNC boring and milling centers and heat treats blades to HRC 58 to 62. Request at least three international references in a similar coil range, and check whether remote support is provided within 24 to 48 hours. A factory that also produces related machine tools, such as levelers and cut-to-length lines, usually controls more of the quality chain and can integrate the slitting line with existing coil handling equipment more smoothly.
Match the line to your thickest and widest coil, not the average. If you process 3 to 12 mm thick and up to 1,600 mm wide coils, choose a line with a 1,600 mm rated width and at least 20 percent torque reserve. Line speed should match your daily tonnage target; for 90 m/min operation with a 30-ton coil, plan for 8 to 12 coils per shift. Consider quick-change cartridge heads if you change strip width more than three times per shift, and select tension recoilers with servo control for thin, high-strength strip. Always share material grade, tensile strength and strip width range so the manufacturer can size shafts, blades and motors correctly.
Slitting accuracy and blade life depend on blade clearance, shaft rigidity, leveling quality and tension control. Correct clearance is typically 8 to 12 percent of strip thickness for steel; too little causes blade wear and burrs, too much produces edge rollover. Shaft runout should stay within 0.02 mm, and blade hardness between HRC 58 and 62. Proper leveling removes coil set and internal stress, reducing camber to under 1 mm per 2 m. Stable recoiler tension prevents strip wandering and edge damage. With correct setup and preventive maintenance, blade life can exceed 8,000 tons of processed steel, and slitting width accuracy stays within plus or minus 0.05 mm.
Yes, but the line must be configured appropriately. For high-strength low-alloy steel up to 12 mm thick, choose higher motor power, six-high leveling and larger blade shafts. For galvanized or painted coils, use polymer-coated tension pads and protective guide rollers to avoid surface scratches and coating damage. Edge trimming and oiling units can further protect cut edges. In an Indian appliance project, a properly equipped line kept surface defect rate below 0.4 percent on galvanized strip. Always specify coating type and surface requirements during the technical discussion so blade clearance, pad material and line speed are set correctly.

Related Articles

How to choose a machining center?

12

Dec

How to choose a machining center?

View More
Why multi functional edm machine meets mixed mold and part production factory demands

14

Aug

Why multi functional edm machine meets mixed mold and part production factory demands

Navigating the Complexities of High-Mix Manufacturing Environments Running a modern industrial production plant often feels like juggling a dozen spinning plates at once, especially when dealing with high-mix, low-volume manufacturing schedules. Pl...
View More
How to reduce drill bit wear during continuous deep hole machine processing tasks

03

Aug

How to reduce drill bit wear during continuous deep hole machine processing tasks

Understanding the Mechanics of Deep Hole Thermal Stress Executing continuous boring and high-depth machining tasks on industrial production lines presents severe thermal and mechanical challenges that routinely test the limits of cutting tooling. W...
View More
What export quality standards international clients require for wire cutting machine products

03

Aug

What export quality standards international clients require for wire cutting machine products

Understanding International Export Compliance in Precision Machining Navigating the complex landscape of global industrial trade requires a thorough understanding of the stringent technical benchmarks that overseas buyers mandate for advanced metal...
View More

Customer Testimonials

Martin Keller
Reliable Steel Slitting Line With Excellent Accuracy

We run a 1,600 mm steel slitting line from Chuang Yuan for high-strength steel coils up to 12 mm thick. After commissioning, burr height stayed under 0.05 mm and line speed reached 90 m/min. Output increased about 22 percent, and blade changes dropped from twice per shift to once per week. Their engineers responded to our questions within 24 hours and supported us during a critical production ramp-up. For a coil service center like ours, that reliability is worth more than a low purchase price.

Emre Yilmaz
Fast Changeover And Strong Technical Support

We ordered a quick-change steel slitter line for square tube production. Width changeover dropped from 75 minutes to 28 minutes, scrap fell from 3.1 percent to 1.9 percent and accuracy held within plus or minus 0.05 mm. The factory provided clear manuals, spare blade sets and remote video support within 48 hours when we adjusted tension settings. Our operators were trained in three days and now run the line confidently. We have already recommended this manufacturer to two partner factories.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
In-House CNC Machining And Strict Quality Control For Every Steel Slitting Line

In-House CNC Machining And Strict Quality Control For Every Steel Slitting Line

Uncompromised structural integrity and absolute dimensional precision begin directly inside our manufacturing facilities through rigorous in-house CNC machining of all critical steel slitting line components, including slitting heads, drive shafts, leveling rolls, and heavy-duty machine housings. This vertically integrated manufacturing strategy allows our engineering team to maintain absolute control over concentricity tolerances, geometric parallelism, and surface finish standards, entirely eliminating the variable quality risks associated with outsourced components. Heavy-duty knife shafts undergo precision grinding and dynamic balancing to ensure rotational runout remains strictly within 0.02 mm during full-speed operations, while premium alloy slitting blades are vacuum heat-treated to HRC 58–62 and ground in matched sets to guarantee optimal cutting clearance.
Customized Slitting Solutions Based On Real Coil Data And Application Needs

Customized Slitting Solutions Based On Real Coil Data And Application Needs

Recognizing that modern coil processing enterprises operate under unique material constraints and volume targets, we firmly reject generic catalog machinery, choosing instead to custom-engineer each steel slitting line around precise, customer-specific coil data and operational workflows. Prior to finalizing any technical proposal, our experienced mechanical engineers thoroughly analyze essential parameters including metal alloy grades, ultimate tensile strength thresholds, material thickness ranges, strip width profiles, maximum coil weights, daily shift output targets, and available factory floor dimensions. Based on these verified inputs, we precisely calculate optimal motor power ratings ranging from 15 to 45 kW and above, select appropriate shaft diameters, configure multi-roll leveling assemblies, and design customized tension control strategies. Optional modular components—such as quick-change cartridge slitting heads, precision edge trimming units, automated oiling assemblies.
WhatsApp WhatsApp Email Email Mobile Mobile TopTop